


Introduction
Lead compounds are among the most important of these metals. They are strictly regulated in food, water, air, and other environments because lead is a potentially dangerous toxicant. Many countries have developed national programs to reduce lead pollution and protect children’s health [1-4].
Lead is a highly efficient raw material, and about 80% of the world’s utilization is for the production of high-performance batteries [5]. This is characterized by its energetic capabilities [6]. Also, lead has a wide range of physical and chemical properties that are utilized in various engineering sectors [7-9]. Scientists predict that the demand for lead for battery production will increase to 14 million tons/year in 2025 [10-11].
Much attention is paid to the pyromethod. Lead ores act as raw materials for their production. They are divided into primary and secondary resources. 60-66% of secondary lead is included in the resources of developed and developing countries around the world. There is no smelting of primary lead in America, although concentrates are produced routinely [12-15].
Lead slag, in large quantities, is a waste product of metallurgical production. Smelting 1 ton of concentrate produces 7100 kg of lead production slag [16]. They are only stockpiled over large areas of land, indicating difficulties in the slag disposal process [17, 18]. So, it was found in the composition of lead slag that toxic elements [19] pollute the environment [20-22].
There are also valuable components in metallurgical slags that can act as secondary resources if properly separated out [23, 24]. There are many methods of recycling lead-containing slags to date. One common method is direct reduction, where only lead and zinc are released [25-28]. The method of leaching lead minerals from lead slag is also one of the methods of utilizing metallurgical waste. Acetic acid was used as a reducing agent [29, 30], and sodium carbonate was used for sulfur fixation [31, 32].
There is also a method of biological leaching of metallurgical waste using bacteria, but it has a high cost [33-35].
The technologies of complex processing of metallurgical wastes with the extraction of valuable metals such as Pb, Zn, and Cu have been studied previously [36]. We have studied the methods of chloride distillation of metallurgical waste with the separation of lead, zinc, copper, nickel chromium, chromium, and cadmium [37, 38]. The technology was patented by our research team as a utility model in the Republic of Kazakhstan [39].
The aim of the research is to find highly effective methods of mathematical planning for metallurgical waste processing, with the separation of composite materials. There are many methods of mathematical planning, such as analytical, experimental, and experimental-analytical methods. Usually the following “elementary” processes are considered when modeling chemical technology objects: movement of phase flows; mass transfer between phases; heat transfer; change of aggregate state; chemical transformations. The application of mathematical methods in solving technological problems allows to raise the general level of theoretical research and makes it possible to conduct it in closer connection with experimental research [40-44].
Material and Methods
Samples were taken from the storage of waste slag from lead production to conduct research on solving the problems of waste-free processing of metallurgical wastes using modern methods of mathematical planning.
Chemical analysis methods such as complexometric titration and atomic adsorption were used to study the chemical and physicochemical features of waste slag and recycling products.
The phase, elemental composition, and microstructure of starting materials and obtained products were analyzed using the scanning electron microscope JSM-6490LV.
Experimental studies of the chloride-ignition roasting of waste slag were carried out in a laboratory unit at a temperature of 1000-1200°C and a duration of 10-60 minutes.
Optimization of experimental data on the firing of mixtures and determination of technological modes were carried out using the program “STATISTICA”. The application of mathematical methods in solving technological problems allows to raise the general level of theoretical research and makes it possible to conduct them in closer connection with experimental studies.
The target output variables selected are: residual metal recovery rate and physicochemical features of expanded claydite [43, 44].
The mathematical planning was based on more than 20 experimental studies on the degree of chlorination of lead, zinc, and copper as a function of mixture composition, temperature, process duration, and degree of chlorination in our research. To reduce the number of experiments, we used rototable planning for the experiment. The so-called “star shoulder” is used to construct rototable central compositional plans. The stellar leverage value is φ=1,414 (coded scale) for the two factors. The independent factors were the temperature and the duration of the process [45].
The significance of the regression equation coefficients was assessed using student’s criterion. The adequacy of the regression equation was checked using Fisher’s criterion [46].
Results and Discussion
The sample was used for experimental studies of the firing composition of mixtures of waste slag, refractory clay, and calcium chloride, the chemical composition of which is given in Table 1. Chemical and mineralogical features of refractory clay used as a fluxing component were given in our articles [38].
It is observed that the component ratio has no significant effect on the chloride distillation of lead, nickel, chromium, and copper from the results obtained.
Table 1.
Chemical composition of lead slag, %
| Components | Zn | Pb | Cu | SiO2 | Fe2O3 | CaO | S | Н2O | Others |
|---|---|---|---|---|---|---|---|---|---|
| Content, % | 2,3 | 1,95 | 0,67 | 29,5 | 38,9 | 25,2 | 0,62 | 0,11 | 0,75 |
It follows from the obtained results that the ratio of components does not significantly affect the chloride extraction of lead, nickel, chromium, and copper.
Independent parameters of mathematical modelling were the content of slag, calcium chloride, and clay. The ranges of variation in factors are given in Table 2. The plan and results of the experiments are shown in Table 3.
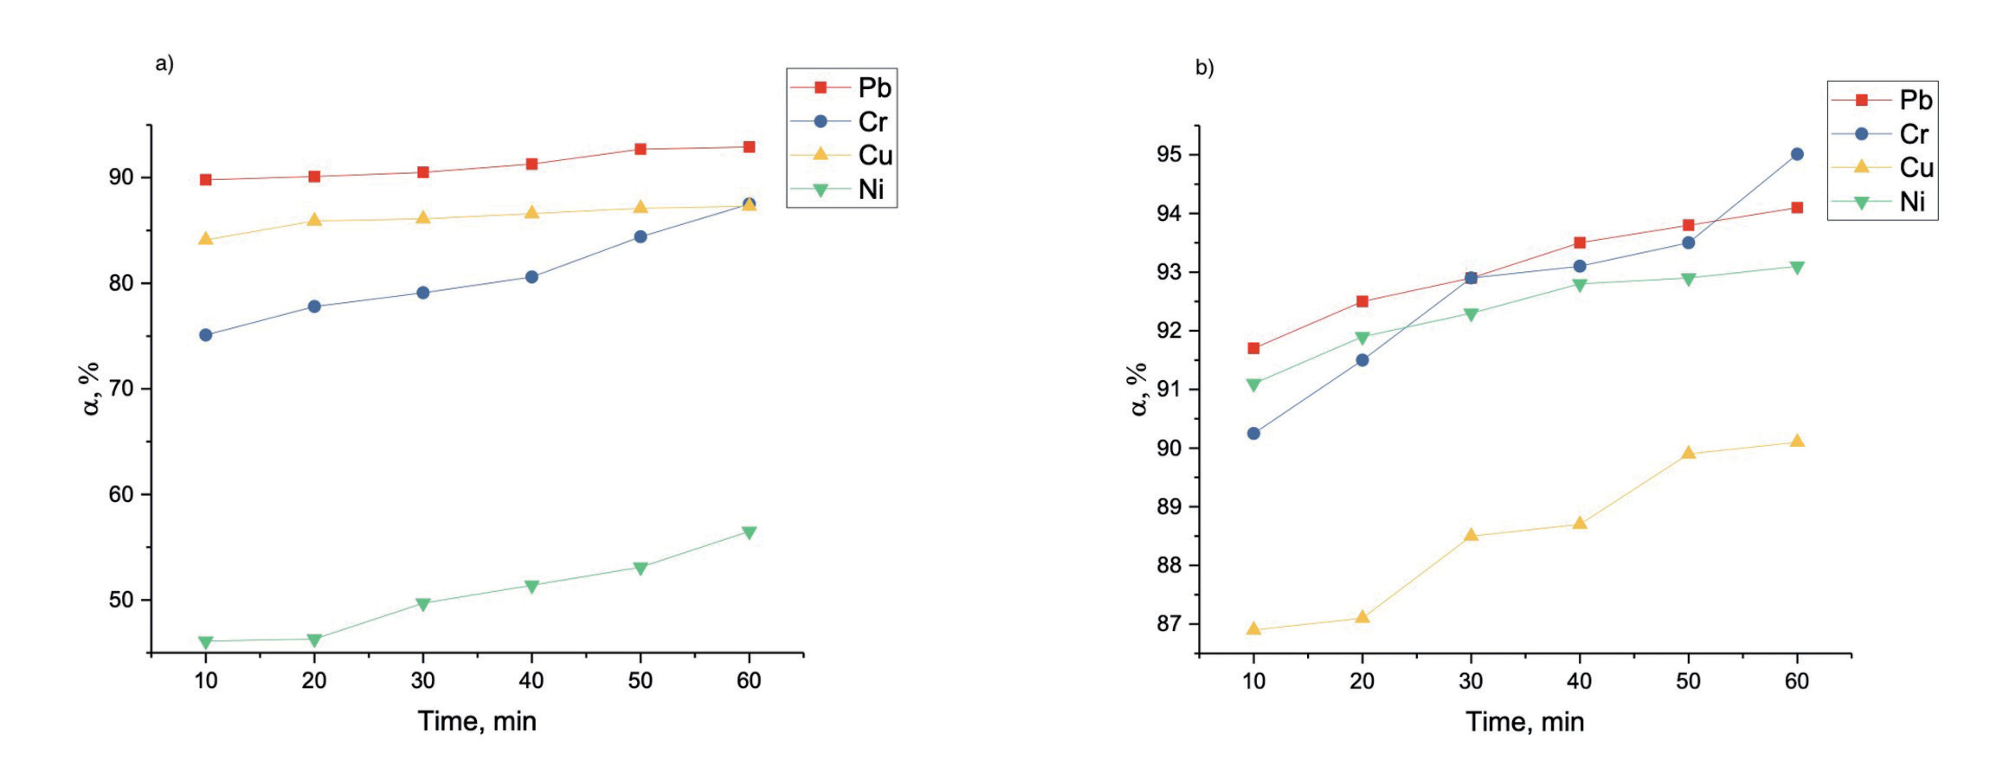
Graphical dependences of the degree of separation of metals on the duration of firing (10-60 minutes) and temperatures (1100-1200°C) are shown in Fig. 1. The analysis of the obtained results showed that the higher the temperature and duration of the process, the degree of metal extraction in the form of chlorides in the final points reaches maximum value.
Table 2.
Input data for planning experiments
Table 3.
Plan and results of experiments on lead chloride distillation
Fig. 1.
Dependence of the degree of metal release on temperature and duration of firing (a) at 1100°C, b) at 1200°C.
The coefficient b of the regression equation describing the object under study in its form as a result of mathematical processing of the results of experiments:
where
The regression equation is as follows in coded form:
Which, after the screening of independent coefficients by student’s criterion, takes the following form:
Constant and variable criteria affecting the optimization of the technological process were selected based on the results of experimental studies.
The obtained three-dimensional dependences of the degree of separation of lead, copper, chromium, and nickel are shown in Fig. 2.
Analysis of the obtained dependences showed a high degree of lead extraction up to 93-95% at the addition of calcium chloride and 9.09% of slag weight.
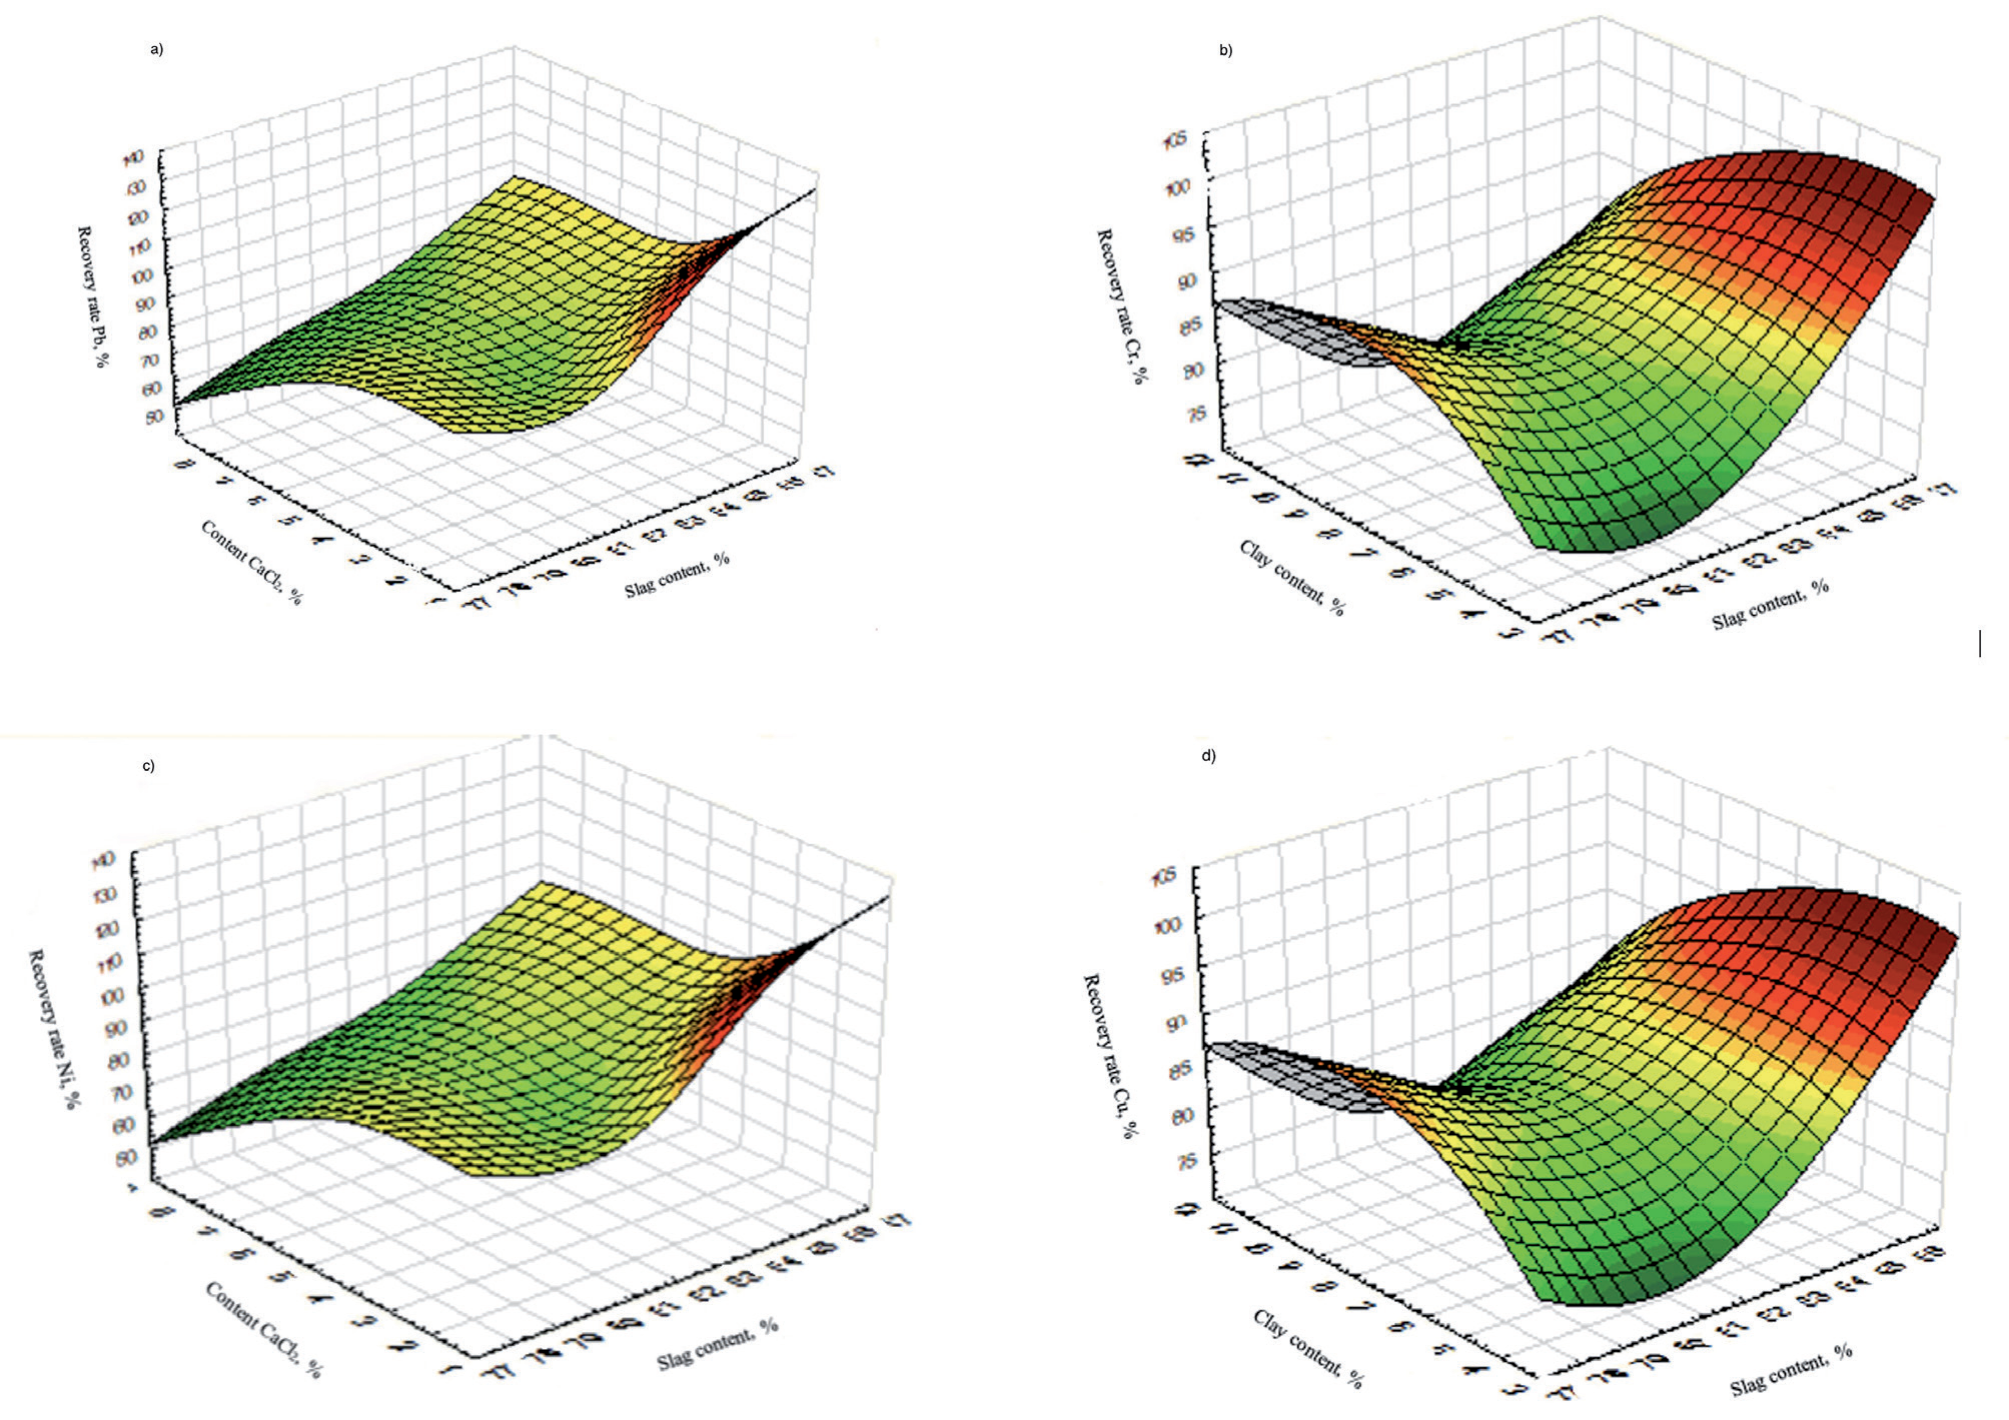
Table 4.
The elemental composition of the firing products, %
| Elements | О | Mg | Al | Si | Pb | S | K | Ca | Ti | Mn | Fe | Cu | Zn |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Sample 1 | 29.45 | 1.75 | 3.84 | 25.62 | 0.50 | 2.08 | 0.78 | 11.42 | 0.79 | 0.50 | 22.42 | 0.22 | 0.63 |
| Sample 2 | 33.23 | 1.47 | 3.01 | 25.11 | 0.47 | 0.13 | 0.91 | 12.47 | 0.57 | 0.50 | 21.2 | 0.11 | 0.82 |
The degree of chromium extraction depends on the ratio of slag and clay component. At the addition of 8-10% of the clay component, the degree of chromium extraction reaches 94-96%.
Dependence of nickel extraction showed that a degree of extraction up to 93% is achieved with the addition of calcium chloride at 8%, and copper is extracted by 90% with the addition of calcium chloride at 10%.
The elemental composition of the firing products at temperatures of 1100°C - sample 1 and 1200°C - sample 2 and the microstructure of the firing products are shown in Table 4 and Fig. 3.
The surface is characterized by the presence of the aluminosilicate minerals melilite, merwinite, and ockermanite, as well as calcium monosilicates, in the form of colorless or white crystals of prismatic structure or tablets in the general structure of firing products. A slight increase in potassium content at 1200C indicates the formation of potassium-calcium silicate as rounded, colorless crystals around the aluminosilicate minerals. Small dark gray crystals of calcium ferrite are also observed around aluminosilicate crystals.
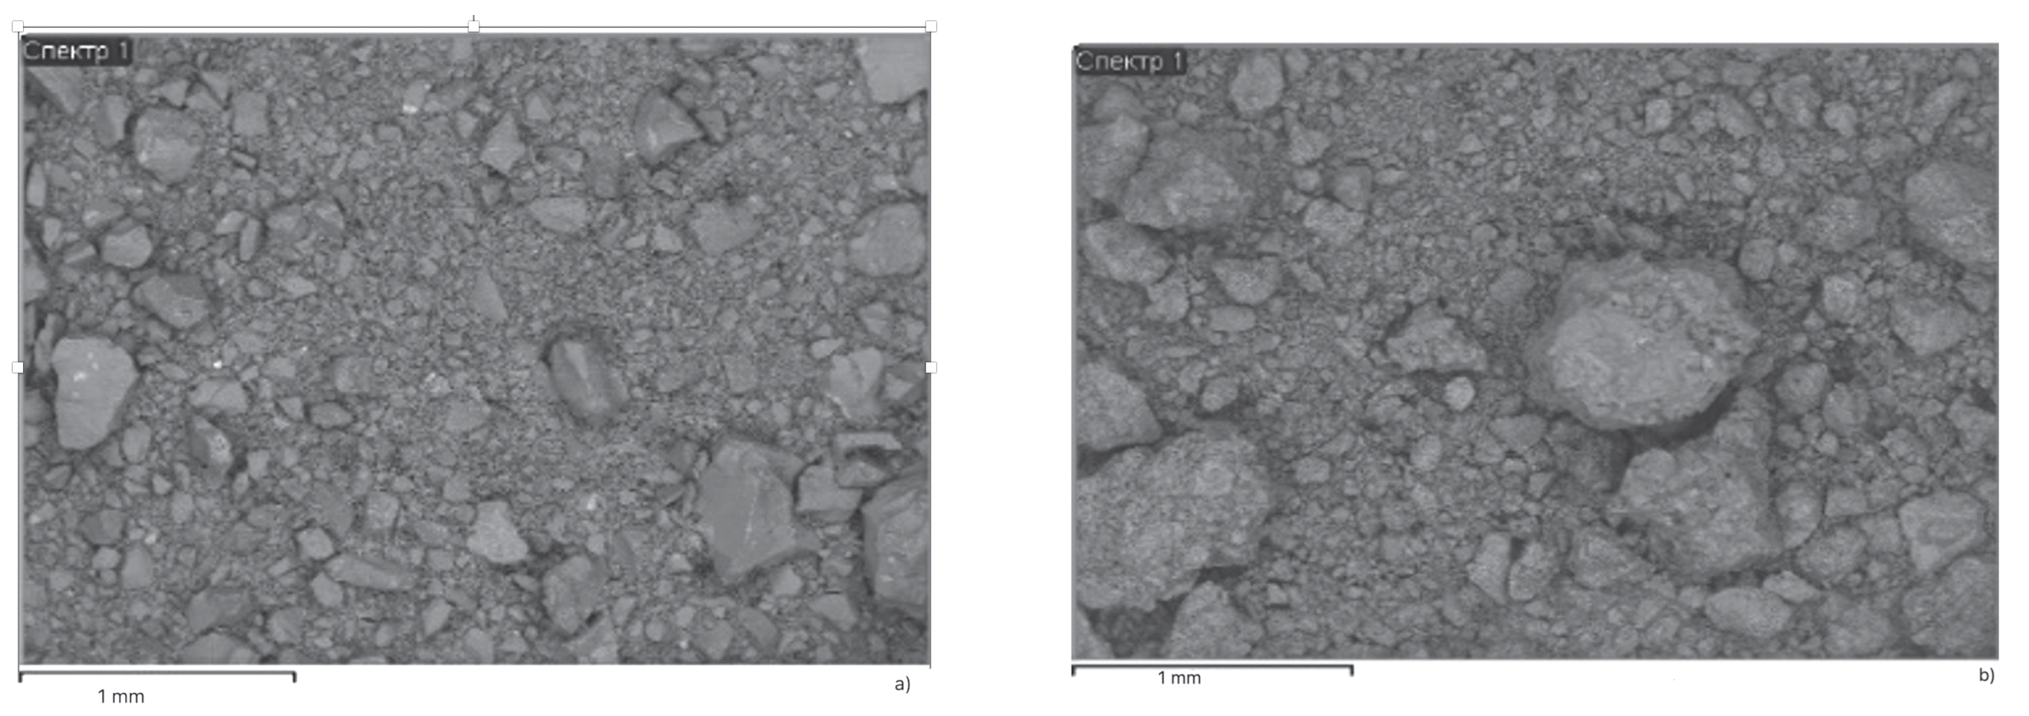
The total percentage of aluminosilicate minerals in the form of irregular hexagons with surface inclusions of calcium monosilicates increases up to 50% at 1200°C. It is connected with the increase in the formation of calcium oxide at the decomposition of its chloride.
The obtained results of optimization of technological parameters and compositions for chlorinating roasting have important practical significance for pilot tests of complex waste-free processing of metallurgical wastes.
Conclusions
The recycling of lead-containing slag offers enormous environmental and economic benefits through resource savings, hazard reduction, and greenhouse gas emission reductions. Pyrometallurgical and hydrometallurgical processes make it possible to extract and reuse valuable lead resources while minimizing the release of toxic substances into the environment.
The mathematical planning of the experiment was performed with an evaluation of the significance of the criteria and the regression equation.
The results of the mathematical planning of the processing of waste slag and galvanic sludge showed that the recovery of lead reaches 93-95%, chromium-94-96%, nickel-93%, and copper-90%.
The obtained product of firing at a temperature of 1200°C can be identified by elemental composition and microstructure as a composite material called keramsite.

