

Introduction
The general definition of cheese substitutes or imitation cheeses is products that are intended to partially or completely replace or imitate cheese and are partially or completely substituted by non-milk-based alternatives, primarily of vegetable origin [1]. There are a variety of reasons why analogue cheese products have been successful in the United States, as follows: (i), natural cheeses are more expensive; the lower price of vegetable oils causes the low cost of analogues compared to butter fat, and the relatively; (ii), lower cost of manufacturing equipment compared to that needed for natural cheese; (iii), they offer a diverse functionality range (for example, flowability, melt resistance, and shred ability). Substitute/imitation cheese products are made by mixing, blending, and heating ingredients that are obtained from dairy and/or vegetable products [2]. Soybean, one of the most important crops, is widely consumed worldwide [3, 4]. Soybean produce the highest level of protein per unit area, making them an important non-animal protein [5]. It is low in sulfur-containing amino acids, with methionine being the limiting amino acid [6]. Customers are increasingly interested in soy protein components due to their adaptability, high nutritional value, and adaptability. Soybeans are a safe and adaptable food source, providing essential nutrients and high-quality protein. However, lectins and digestive enzyme inhibitors can cause adverse effects when ingestion. To enhance the nutritional quality of soy protein-based foods, lectins and other inhibitors are usually inactivated by heat [7]. It contains all essential amino acids, has a 92% to 100% digestion rate, and contains up to 1 g/kg of isoflavones. The cheese analogue products are made using a different combination of starch and fat to imitate cheese, but starch does not react to temperature changes like milk casein [8]. Many people are suffering from lactose intolerance; at the same time, the main source of lactose is milk; consequently, dairy products have become a source of health problems, which may lead to the removal of dairy foods from the diet [9]. Therefore, several investigations were conducted previously to find out an alternative to proteins. Processed cheese spreads (PCSs) were manufactured by replacing hard cheeses with lentil paste, lupine paste, or common bean paste [10]. We examined analogues of cheese by replacing dairy fat with vegetable fat showed increased adhesiveness and hardness. The sensory analysis showed that the vegetable fat analogue was better evaluated [11]. The impact of substituting fat milk with vegetarian oils on processed cheese’s storage characteristics showed no significant differences [12]. The characteristics of spreadable analogue cheese by substituting edam cheese and cheddar cheese with soy protein isolate were investigated [13]. This study focused on producing cheese analogues from legume proteins, whose knowledge is still limited. To achieve global goals of responsible consumption and production, it is crucial to find plant-based alternatives. Further research is needed to understand the protease enzyme responsible for amino acid cleavage in plant-based proteins for cheese analogues [8]. Cheese analogues have not significantly impacted the retail market due to quality issues, psychological resistance, lack of regulations, and labeling problems [14].
According to the best of our knowledge, there is a big shortage of milk and cheese-free lactose in the local Egyptian market, which is very important for patients who are suffering from lactose intolerance as well as vegan people and Christian fasting people. Moreover, the available lactose-free or low-lactose cheeses, such as long-ripened cheeses, in the Egyptian market are mostly imported and expensive. Therefore, our research aims to use soy protein isolate as an alternative to dairy products for manufacturing imitation processed cheese free of lactose, which is useful and covers the needs of lactose intolerance patients, vegans, and Christian fasting people as well. In addition, it could be a source of low-cost prices and saving hard currency needs.
Materials and Methods
The main components applied to the formulation of the imitation processed cheese spread (IPC) blends were gratefully received from Green Fields Dairy Factory, Kafr El-Sheikh, Egypt. The factory is a white list company accredited by the National Food Safety Authority (NFSA), belonging to the Council of Ministers, Egypt. These components consisted of skimmed milk powder (SMP) (Rucker GMPH, Aurich, Germany), which contains 4% moisture, 1.25% fat, 52.5% lactose, 36% protein, and 8% ash, “emulsifying salts”, (Joha® S203, producer: BK Guilini Gm BH Ladenburg -Germany) consist of poly and diphosphates, “xanthan gum” (XG) (E- 415, Fufeng Biotechnologies Co., China), “guar gum” (GG) (E-412, it is a natural polysaccharide produced from the guar shrub Cyamopsis tetragonoloba was produced by Dabur India Limited, Rajasthan, India.), “Stabilizer” (Meyprogen JO-73, it consists of E- 407 Carrageenan, E -410 Locust Bean Gum, E 415 XG E- 508 Potassium Chloride, and E-516 Calcium Sulfate. Producer: DuPont Nutrition Biosciences ApS, Haderslev, Denmark), “soya protein isolate” (SPI) food grade was obtained from Bavly International, Cairo, Egypt, with the following composition: 90 % protein, 4.5% moisture, 5% ash and <0.1% fat, “dried potato powder” (DPP), was obtained from Teiba Company, Borg Al-Arab, Egypt, “modified starch” (Cargill NV, European Union), “whey” sweet whey powder spray dried, (SWP; Sierolat SPA, Strada Vicinale Muricino, 81050 Francolise Caserta, Italy) which contains 4% moisture, 1.25% fat, 75% lactose, 11% protein and 8 % ash, “starch” (corn starch, Turkish origin), “shortening” (100% pure palm oil, refined, non-hydrogenated, food grade, Arma Company, 10th of Ramadan City, Sharqia, Egypt (“salt”: pure dried vacuum salt produced by the Egyptian Salts & Minerals Co. Fayoum, Egypt, “cheddar flavor” manufactured by Givaudan Company (6th of October City, Egypt) and water is added to complete the mixtures as calculated.
Manufacturing Methods
The manufacture of processed cheese was done by calculating the ingredient amounts of the different blends [15, 16]. A double jacket pan (Prosestek Makina Sanayi Ve Ticaret Limited Sirketi, Turkey) was used to manufacture processed cheese at 85°C for 8 minutes. All experiments were designed using a completely randomized design (CRD). Four treatments included control, Treatment 1 (T1), Treatment 2 (T2), and Treatment 3 (T3). In all experiments, unless otherwise stated, three biological replications per treatment were analyzed (n = 3). The ingredients of treatments examined in this study are as follows in Table 1:
Physico-chemical Analyses
Moisture Determination
Processed fresh cheese samples were analyzed for moisture determination. Moisture content was measured according to Ling [17], fat (Gerber method).
Determination of Total Nitrogen
Using the total nitrogen (micro Kjeldahl method), the factor of 6.38 was used to determine protein in milk and milk products; however, the factor of 6.25 was used to determine protein in treatments, and ccc was recorded as percentages of lactic acid, and the amount of sodium hydroxide solution (0.1 N NaOH) used to reach the endpoint was recorded as the amount of titratable acidity according to the method described by Ling [17].
Determination of Salt Content
Salt content was measured by titration methods using potassium chromate (2%), and silver nitrate (AgNO3) (0.05 N). The following step involved boiling 0.5 g of the cheese sample in 50 mL of distilled water over a flame. We filtered it, followed by two washings of the precipitate. Following the completion of the filtration, we added 1 mL of potassium chromate (2%), 5 mL of filtrate, and 0.05 N of AgNO3 until a stable red color was visible, then the AgNO3 concentrations were recorded according to the Association of Official Analytical Chemists [18, 19].
Determination of Ash Content
The ash content was determined according to Hagrass [20]. One gram of sample was weighed in a constant weight crucible and then heated in a muffle furnace at 550ºC for 6 hours. The crucible was cooled and reweighed for ash calculation.
Determination of Lactose
Lactose levels were evaluated according to Barnett and Abd El-Tawab [21]. One gram of sample was accurately weighed in a 100-ml volumetric flask. Twenty-five ml of distilled water was added, followed by 2 ml of 1 N NaOH, and mixed well until the sample was completely dissolved. The flask contents were made up to volume with distilled water and mixed thoroughly. One ml of the sample solution was pipetted into a stoppered test tube, followed by 1 ml of 5% phenol, and mixed well. 5 ml of concentrated sulfuric acid was added to the tube contents with care, mixed well, and left to cool at room temperature. The absorbance was determined using a 1 cm glass cell and spectrophotometer (Tomos, Italy) at 490 nm. The lactose content of the sample was determined from a standard curve of lactose ranging from 10-100 μg/ml. A pH was used for pH measurement.
Table 1.
The ingredients of treatments.
Determination of Carbohydrate Content
Carbohydrate content was measured using the following equation: carbohydrate = total solids - (fat + protein + ash) [22].
Analysis of Processed Cheese
Processed cheese samples were analyzed for total volatile fatty acids (TVFA) according to Kosikowski [23]. The results were expressed as ml 0.1 N NaOH/100 g cheese; the meltability test was recorded in triplicate according to Olson et al. [24]. A Pyrex glass tube (30 mm in diameter and 250 mm in length) was used to hold the spreads while carrying out the meltability test. One of the ends of the tube was closed with a rubber stopper perforated by a 1mm glass tube to act as a vent. A reference line was marked on the opposite end of the melting tube. This end of the tube was also closed with a rubber stopper. A solid cheese cylinder (15 + 0.2g) was placed in the tube with its front edge aligned with the marked reference line. Melting tubes were placed in a vertical position on a rack for 10 minutes at approximately 40ºC and then in a horizontal position in an oven at 110ºC for 30 minutes. The flow of the hot cheese mass was stopped instantly for measurement with a tilt control rack. The distance of flow from the reference line to the leading edge of the melted cheese was recorded in cm as “cheese flow” or “cheese meltability. The texture profile analysis was conducted on 2×2×2 cm for each biological replicate (three replicates per treatment). A two-bite penetration test was done using the Texture Analyzer with a TA 25 mm diameter cylinder probe and operated at a crosshead speed of 50 mm.sec-1. The test was done at the Food Technology Research Institute using a Universal Testing Machine, Food Technology Corporation, Sterling, Virginia, USA, and the calculations were performed using the attained profile to obtain the following texture profile: Characters: hardness (N), chewiness (mJ), springiness (mm), gumminess (N), cohesiveness ratio, and adhesiveness (mJ).
Microbiological Examination
Staphylococci count was determined using Staph Medium No. 110 as described in the Difco Manual [25]. Coliform group count was made using the violet-violet-red bile salt agar medium. The plates were incubated for 24 hours at 37ºC. The counts of yeasts and molds were done using potato dextrose agar. Anaerobic spore-forming bacteria were counted and determined according to APHA [26] using a nutrient agar medium. The plates were incubated at 32ºC for 3 days before counting. Total bacterial counts (TBC) were enumerated using Tryptone Glucose extract agar medium according to the method described by the Difco manual [25]. All media were obtained from Biolife Company Italiana S.r.l. (Milan, Italy). One gram of cheese was accurately weighed in a sterile watch glass and then transferred to a sterile mortar jar. Nine ml of sodium citrate solution (2%) was added to the cheese, and the mixture was homogenized until it became uniform. One ml of the previous solution was added to 9 ml of sterile saline solution and mixed well to give the 1: 100 dilutions, which are used for making other dilutions serials. The microbial counts were expressed as CFU ̸ g cheese [26].
Organoleptic Properties
The sensory characteristics of produced cheese were carried on as described by Meyer [15]. Briefly, three pieces of cheese per treatment were vacuum packaged in airtight plastic bags at Green Fields Company and coded with a 3-digit code, then sent to the sensory team at the Department of Food Science and Technology, Faculty of Agriculture, Tanta University, Egypt. All assessments were done in individual booths designed according to the international standard (ISO, 2007). The panel was composed of well-trained 13 judges (7 males and 6 females, age range 30-55 years old) who had several years of experience in sensory evaluation of cheeses (4 academic staff, 3 trained and experienced consumers, and 6 quality engineers from dairy products companies). Before evaluation, the panel used commercial hard cheese in a pretesting session to standardize the panel’s definitions for the sensorial attributes. The judges assessed all samples (cheese slices of 1 cm of approximately 10 g) in a monadic sequential way using a 100-point scale (40 points for body and texture, 40 points for flavor, and 20 points for outward appearance) as described by Meyer [15]. After testing each sample, the pane lists drank water to clean their palate before testing the next sample.
Statistical Analysis
All the data were statistically analyzed by the SPSS statistical software using one-way ANOVA. Analysis of variance and Duncan’s test as well as average and standard error were carried out using the SPSS computer program (SPSS, 2016; version 24) at P≤0.05.
Results
The composition of fresh imitation processed cheese was meaningfully influenced by the combined impact of these elements. Generally, the fresh imitation processed cheese produced with different soy protein isolate replacement percentages showed acceptable physico-chemical characteristics and sensory properties compared with the control cheese.
Moisture, Salt, and Ash content of Imitation Processed Cheese
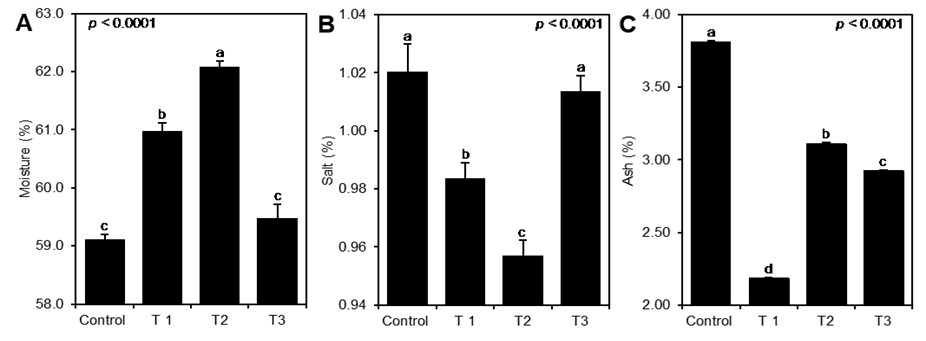
The fresh cheese produced from T2 exhibited the highest levels of moisture content (62.07±0.11%) compared with significantly lower control cheese (59.10±.10%; Fig. 1A). On the other hand, the salt content of fresh cheese produced from T3 did not differ significantly from the control (1.02±010 and 1.01±0.09%, respectively), whereas the lowest salt content was recorded by fresh cheese produced from T2 (0.96±0.11%; Fig. 1B). Finally, all treatments (T1, T2, and T3) significantly reduced the ash content of freshly produced cheese (Fig. 1C), and the minimum ash content was recorded for T1.
Effect of Soy Protein Isolate Replacement on the Chemical Composition of Imitation Processed Cheese
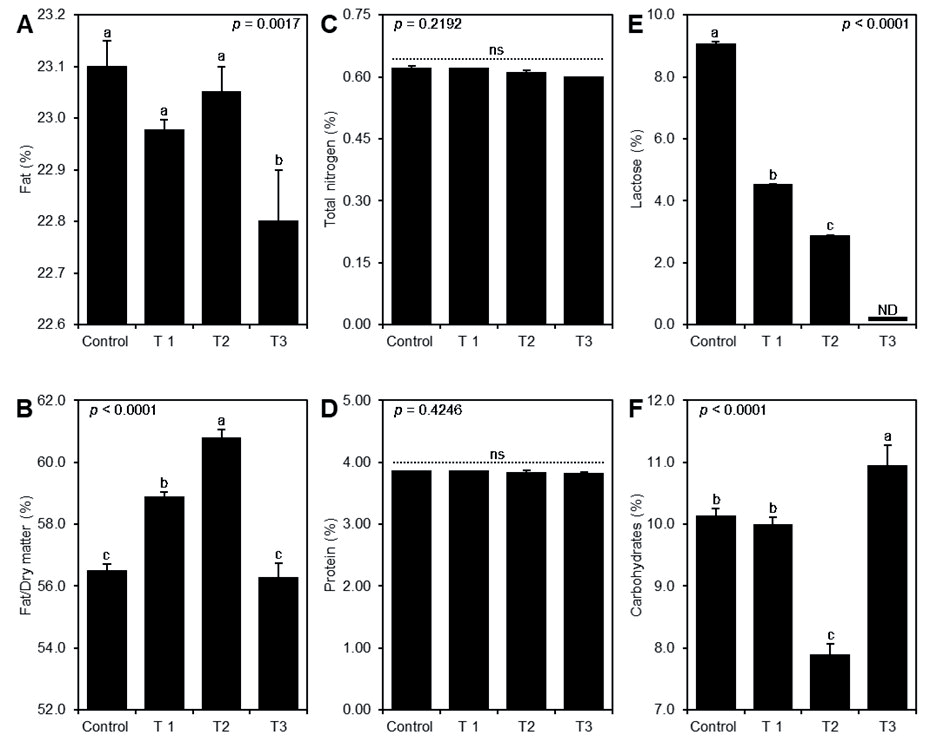
It is worth mentioning that there were no significant differences in fat percentage in control cheese and fresh cheese produced from T1 and T2 (Fig. 2A). However, both fresh cheeses produced from T2 and T1 had a higher fat/dry matter ratio (60.77±0.30 and 58.86±0.19; respectively) (Fig. 2B). On the other hand, soy protein isolate replacement affected neither total nitrogen (Fig. 2C) nor protein content (Fig. 2D), but significantly reduced the lactose percentage (Fig. 2E) in imitation processed cheese. Interestingly, fresh cheeses produced from T3 appeared to be lactose-free; however, carbohydrate content slightly increased fresh cheeses produced from T3 (10.94±0.33%) compared with control cheese (10.13±0.13%) (Fig. 2F), which retains its nutritional value.
Acidity, pH, TVFA, and Meltability of Imitation Processed Cheese
The substitution of soy protein isolates for skim milk powder significantly increased the pH (Fig. 3A) but decreased the titratable acidity (Fig. 3B) of fresh cheese. Moreover, although soy protein isolate replacement in T1 did not affect the total volatile fatty acids (TVFA) significantly compared with control cheese (10.00±0.00 ml 0.1N NaOH.100 g−1), fresh cheeses produced from T2 and T3 had lower TVFA content (7.00±0.00 ml 0.1N NaOH.100 g−1) with no significant differences between them (Fig. 3C). Finally, there were significant differences in meltability between all imitation processed cheese treatments (Fig. 3D). The maximum meltability was recorded by fresh imitation cheese produced from T2 (20.33±2.52 mm), followed by cheese produced from T1 (14.67±1.53 mm) and control cheese (10.00±1.00 mm); however, the minimum meltability was reported for T3 (0.60±0.10 mm) without the addition of any dairy products (Fig. 3D).
Microbiological Properties of Imitation Processed Cheese
It is worth mentioning that none of the control cheese or the examined variants contained any of the following microbial pathogens: Staphylococci, Coliform, E. coli, yeasts and molds, anaerobic spore, aerobic, or clostridium in the fresh cheese (Fig. 4A). Additionally, the bacteriological quality of fresh imitation processed cheese, measured by enumerating the total bacterial count (TBC), wasn’t affected significantly by the addition of SPI (Fig. 4B).
Fig. 1.
Effect of different soy protein isolate replacement percentages on the chemical composition of imitation processed cheese. (A) moisture content, (B) salt, and (C) ash percentage. Values represent the means±standard deviation (means±SD) of three replicates (n = 3). The significant differences between treatments (p<0.05) were indicated by different letters.
Textural Properties of Imitation Processed Cheese
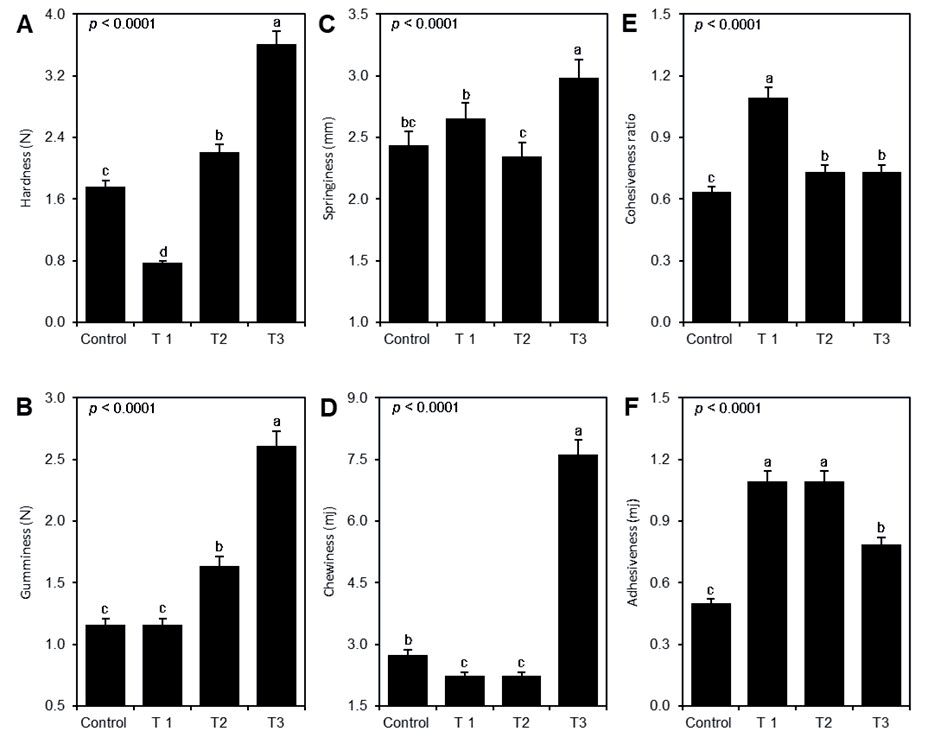
Generally, the textural attributes of fresh imitation processed cheese were significantly changed due to the addition of different portions of soy protein isolate. Briefly, fresh milk-free imitation cheese that was made using the highest percentage of SPI had significantly higher hardness (3.60 N; Fig. 5A), gumminess (2.60 N; Fig. 5B), springiness (2.98 mm; Fig. 5C), and chewiness (7.59 mj; Fig. 5D). However, the highest cohesiveness ratio was recorded by imitation cheese produced from T1 (1.09; Fig. 5E). Furthermore, imitation cheese produced from T1 and T2 had the highest adhesiveness (1.09 mj; Fig. 5F) with no significant differences between them.
Sensory Evaluation of Imitation Processed Cheese
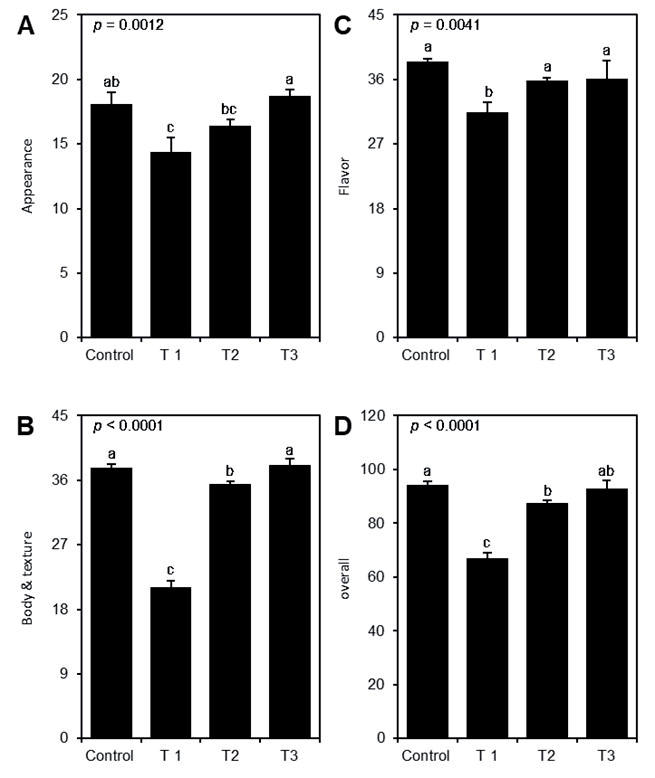
Sensory evaluation showed that the partial replacement of milk with soy protein isolate (T1 and T2) significantly reduced the appearance (14.33±1.15 and 16.33±0.58 points, respectively; Fig. 6A), body & texture (21.00±1.00 and 35.33±0.58 points, respectively; Fig. 6B), flavor (31.33±1.53 and 35.67±0.58 points, respectively; Fig. 6C), and overall grade (66.67±2.52 and 87.33±1.15 points, respectively; Fig. 6D) of fresh imitation cheese. Nevertheless, the complete replacement of milk with soy protein isolate (T3) did not affect any of the studied sensory attributes and all remained in almost the same levels, including appearance, body & texture, flavor, and overall grade (18.67±0.58, 38.00±1.00, 36.00±2.65, and 92.67±3.21 points, respectively) compared with the control cheese (18.00±1.00, 37.67±0.58, 38.33±0.58, and 94.00±1.73 points).
Discussion
Plant-based alternatives to dairy products in the European market are predicted to reach 2.22 USD million by 2026 [27]. This quick growth is determined by the increasing occurrence of allergenicity of milk, lactose intolerance, shifting consumer lifestyles, and concern about alternative diets (i.e., vegan) [28]. As a result of COVID-19 (2020), the pandemic accelerated the behavior of consumers to rethink their lifestyle and vary to a more plant-based diet as a healthier alternative. Consequently, the demand for vegan alternatives to cheese is progressively increasing in value in the trade market [29]. PCA had more total solids, fiber, carbs, vitamin A, and potassium. All PCA had lower levels of hardness, gumminess, cohesiveness, and springiness than the control cheese [30]. From previous literature, one can say that the production and manufacturing of milk-free dairy milk (analogue) became necessary to cover the needs of vegan, lactose intolerant, and Christian-fasting people as well [30]. Our results were supported by the research, which increased the amount of vegetable blend (potato, mushroom, celery, carrot, green bean, dill, leek, and parsley) powder to 10% in the processed cheese formulations. The fortified cheese had a higher protein and fiber content than the conventional cheese [31]. The analogue cheese was even manufactured by adding 4% algal biomass, resulting in a strong and cohesive network with lower oiling off and meltability, which fortified our idea of research [32]. As expected from these results, it was able to manufacture free dairy processed cheese. This was obtained in treatment (T3), which was produced by using soy protein isolate (SPI) and by replacing skim milk powder as well as sweet whey powder. The significant decrease in skim milk powder and the replacement of lactose with plant protein via SPI are quite important for individuals who are suffering from milk protein allergies or lactose intolerance. The variations in salt and ash content of T1, T2, and T3 might be due to variations in their chemical structure and quantity of each ingredient. For example, both skimmed milk powder and dried sweet whey powder spray contain 8% ash each, whereas soy protein powder contains only 5% ash.
Fig. 3.
Effect of different soy protein isolate replacement percentages on the physical and chemical properties of imitation processed cheese. (A) pH, (B) titratable acidity (%), (C), total volatile fatty acids (TVFA; ml 0.1N NaOH.100 g−1), and (D) meltability (mm).
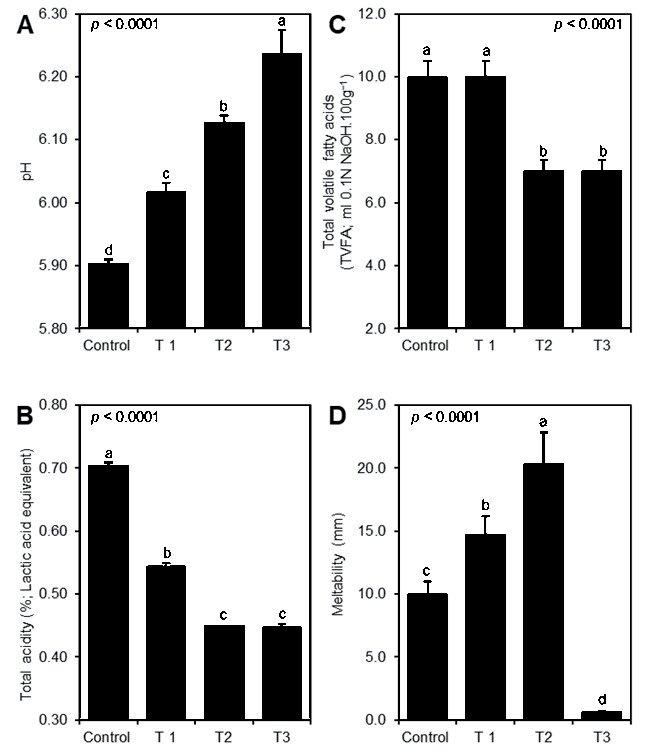
Fig. 4.
Effect of different soy protein isolate replacement percentages on the microbiological quality of fresh imitation processed cheese (CFU.g−1). (A) microbial pathogens and (B) total bacterial count (TBC; CFU.g−1).
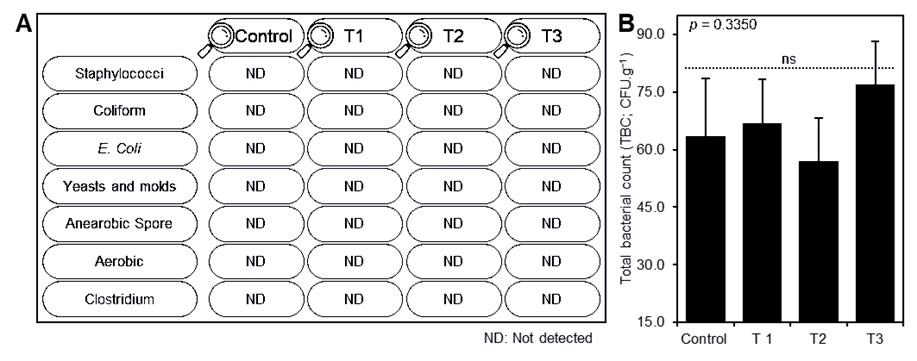
Fig. 5.
Effect of different soy protein isolates replacement percentages on the textural properties of imitation processed cheese. (A) hardness (N), (B) gumminess (N), (C) springiness (mm), (D) chewiness (mj), (E) cohesiveness ratio, and (F) adhesiveness (mj).
Interestingly enough, the chemical composition, such as pH, TVFA, and meltability, of our produced imitation processed cheese was similar to the control produced one. These results were supported by Ammar et al. [33], who determined that the pH of market cheese was 5.4, while El-Sayed [34] found that the pH of cheese was 5.46. The TVFA values in our experiments were acceptable as compared to the control; this was very important to the customers’ sensory evaluation, which led to their enjoyment. The meltability of fresh imitation processed cheese was reduced in T3 compared to the control under high temperatures, but this does not affect the texture or spreadability under normal conditions. These results correlated with that found by Awad et al. [35], who found that the meltability of fresh PCS was zero and was not affected by the cooking temperature of the blends containing cheddar cheese as a natural cheese. The impact of pH on the rheological properties of PC was the objective of some studies. Lee and Klostermeyer [36] studied the effect of pH (5.0- 6.0) on the rheological properties of reduced fat model PCS made from sodium caseinate and sunflower oil. At pH 4.5-5.0, the hardness of the product was very high only when made from acid casein, which decreased significantly with increasing pH. The production of PCS by replacing 50% milk fat with coconut, palm, or sunflower oil. The treatments affected oxidation, physical properties, and organoleptic properties [33]. As regards sensory evaluation of manufactured IPC, in this research, there was a significant reduction in scores for appearance, body, texture, and flavor with partial replacement of SMP by SPI. This suggested that soy protein might not fully mimic the sensory properties of milk in processed cheese. This could be due to differences in the physical and chemical properties of soy protein compared to milk proteins, leading to alterations in appearance, texture, and flavor. Our results proved that the lack of significant changes in sensory attributes with complete replacement of SMP by soy protein isolate (T3) is interesting. It suggests that at a certain level of replacement, the sensory properties of the imitation cheese may not be significantly altered. This could be due to various factors such as the formulation of the cheese, processing conditions, or interactions between soy protein and other ingredients. The lack of adverse effects on sensory attributes with complete replacement suggests that this formulation (T3) might be optimized to maintain the sensory quality of the cheese while achieving the desired composition. This could have implications for product development, especially for individuals with dietary restrictions or preferences. Consumer acceptance: Additionally, studies on consumer acceptance and preference are crucial to determine the market potential of imitation cheese products with complete replacement of milk. Understanding consumer perceptions and preferences can guide product development and marketing strategies. Our results supported similar results, which proved that partial dairy (casein, caseinates, soy oil, etc.) and non-dairy (soy protein, corn protein, soy oil, etc.) are important alternatives to dairy products [31].
Fig. 6.
Effect of different soy protein isolates replacement percentages on sensory evaluation of imitation processed cheese. (A) appearance, (B) body and texture, (C) flavor, (D) overall grade.
The manufacturing was conducted in a closed system, and the added components were controlled so that no microbial contamination was recorded, either coliform bacteria, staphylococci, E. Coli, yeasts and molds, anaerobic spores, aerobic spores, or Clostridium spp. The total bacterial count (TBC) was very significantly decreased as compared with the control, so one could say that there was no TBC at all. These microbial detections proved that our imitation processed cheese is a safe and microbial-free product. These results are very important because this imitation processed cheese is produced especially for patients who suffer from allergies; therefore, it is important to protect them from any source of infection. Previous textural attributes gave different values for all the aforementioned properties, which could be due to differences in the processing technique applied as well as the ingredients used [33]. In general, many variables, including moisture, fat, pH, and the condition of the protein network, influence the textural qualities. The correlation coefficient between the textural properties of cheese and the components of milk was revealed by Mehanna et al. [37]. The produced imitation processed cheese showed textural attributes, which perhaps play a pivotal role in improving the hardness even much better than the control. Our theory was dependent on a key component, namely, soy protein isolate, which is very rich in protein ratio and suitable for vegan industrial products. The emulsification, gelation, and water holding are important functional properties of proteins to produce plant-based cheese analogues [38].
Soy foods were not popular in Western diets, but it was among the popular foods in the Far East. Recently, soybeans have had a problem in the West because of their undesirable aroma and taste. FDA has permitted the use of a soy protein health claim on food labels in the USA. Soy protein may reduce the risk of heart disease because of isoflavones and some phytochemicals found in soybeans. Isoflavones decrease total cholesterol, which leads to a decrease in heart disease risk [39]. Lactose intolerance patients as well as consumers’ expectations who have healthy lifestyles are suffering from a shortage of dairy lactose-free products; therefore, this is a big challenge for industrial producers [40]. Interestingly, the vegetarian lifestyle is becoming progressively popular; recently, a plant-based diet has become more favorable than an animal-based diet [41]. The most popular plant-based protein is soybean [42]. It is very important to create a series of alternative products that are healthy and sustainable for animal products [43]. Although this trend assigns a lot of consideration to producing plant-based alternatives to dairy products such as cheese or yogurt, it is becoming universal [44-46].
The production of imitation processed cheese is promising, especially if the formulation and production methods of imitation cheese consider the consumer’s requirements [40]. It not only covers the needs of vegans, allergic patients, and Christian fasting people but also can be used as a source of medical treatments and protection against heart and cancer diseases, rather than reducing the cost of production because of the exportation of skim milk powder from a broad with hard currency in dollars.
Conclusion
Imitation processed cheese without dairy ingredients that are lactose-free could be manufactured by using 4.5% soy protein isolate, which was shown in treatment (T3). This formula could be very useful for people who are suffering from milk protein allergies or lactose intolerance, as well as vegan and Christian fasting people. SPI substitution influenced the chemical composition, texture, and sensory attributes of the IPC. While SPI-based IPC shows promise as a viable alternative for lactose-intolerant individuals and vegans. The manufacturing was done at an accredited factory from NFSA; this supports that our imitation processed cheese formula could be formulated and manufactured for the trade market and application. At the same time, this saves the consumption of hard currency (Dollars) to export skim milk powder from abroad from an economic point of view, which became urgent after the COVID-19 and Ukraine War.

