


Introduction
Cotton is one of the most valuable raw materials among other technical crops. The Republic of Uzbekistan is one of the leading cotton producers in the world, among China, the USA, India, and other countries. Hand-harvested cotton does not allow for the short-term harvest of cotton when grown on a large area of land, but the quality of hand-picked cotton is better than machine-picked cotton.
The main link in the technical progress of cotton harvesting is the mechanization of harvesting.
The benefits of mechanization of manual harvesting, including all costs associated with cotton transportation, have been practiced by all farmers, and the desire to harvest high quality cotton without precipitation for a high-quality crop shows the need for mechanization of harvesting [1, 2].
In recent years, most of the cotton grown was hand-picked. According to government decisions, the main task is to improve cotton harvesting machines. In recent years, the volume of hand-picked cotton in the Republic was 90-95%. Since 2020, the process of producing raw cotton in the full cluster system has been underway. Cotton and textile clusters expect to create more than 19,000 new jobs through the implementation of projects worth 4.8 trillion soums in 2022-2023. According to the government’s decision to reduce manual labor and introduce a cluster system in cotton production, large-scale work on the mechanization of cotton harvesting is underway. The technique and technology used in the cotton and fiber cleaning process are also based on the fact that nowadays it is mainly hand-picked. If there is an increase in machine harvesting in our country, the amount of cotton pollution coming to the enterprise will increase in proportion to it, so this research is relevant.
Numerous theoretical and practical studies have been carried out on manual and machine-made cotton and its quality. It takes about 100 days, or 3 months, to pick cotton manually. To prevent this, due to the development of technology, it is possible to gather the harvest in 20-25 days. It is important to study the impact of cotton products on quality indices first and foremost when introducing promising technologies for machine harvesting [3, 4].
During the operation of the technological equipment being created, depending on the industrial grades and class of processed cotton, different amounts of waste and dust particles are released [5-9], which is characteristic of almost all technological processes in all industries [10-25].
Cotton contains green foliage, herbs, weeds, green leaves, and other impurities [26].
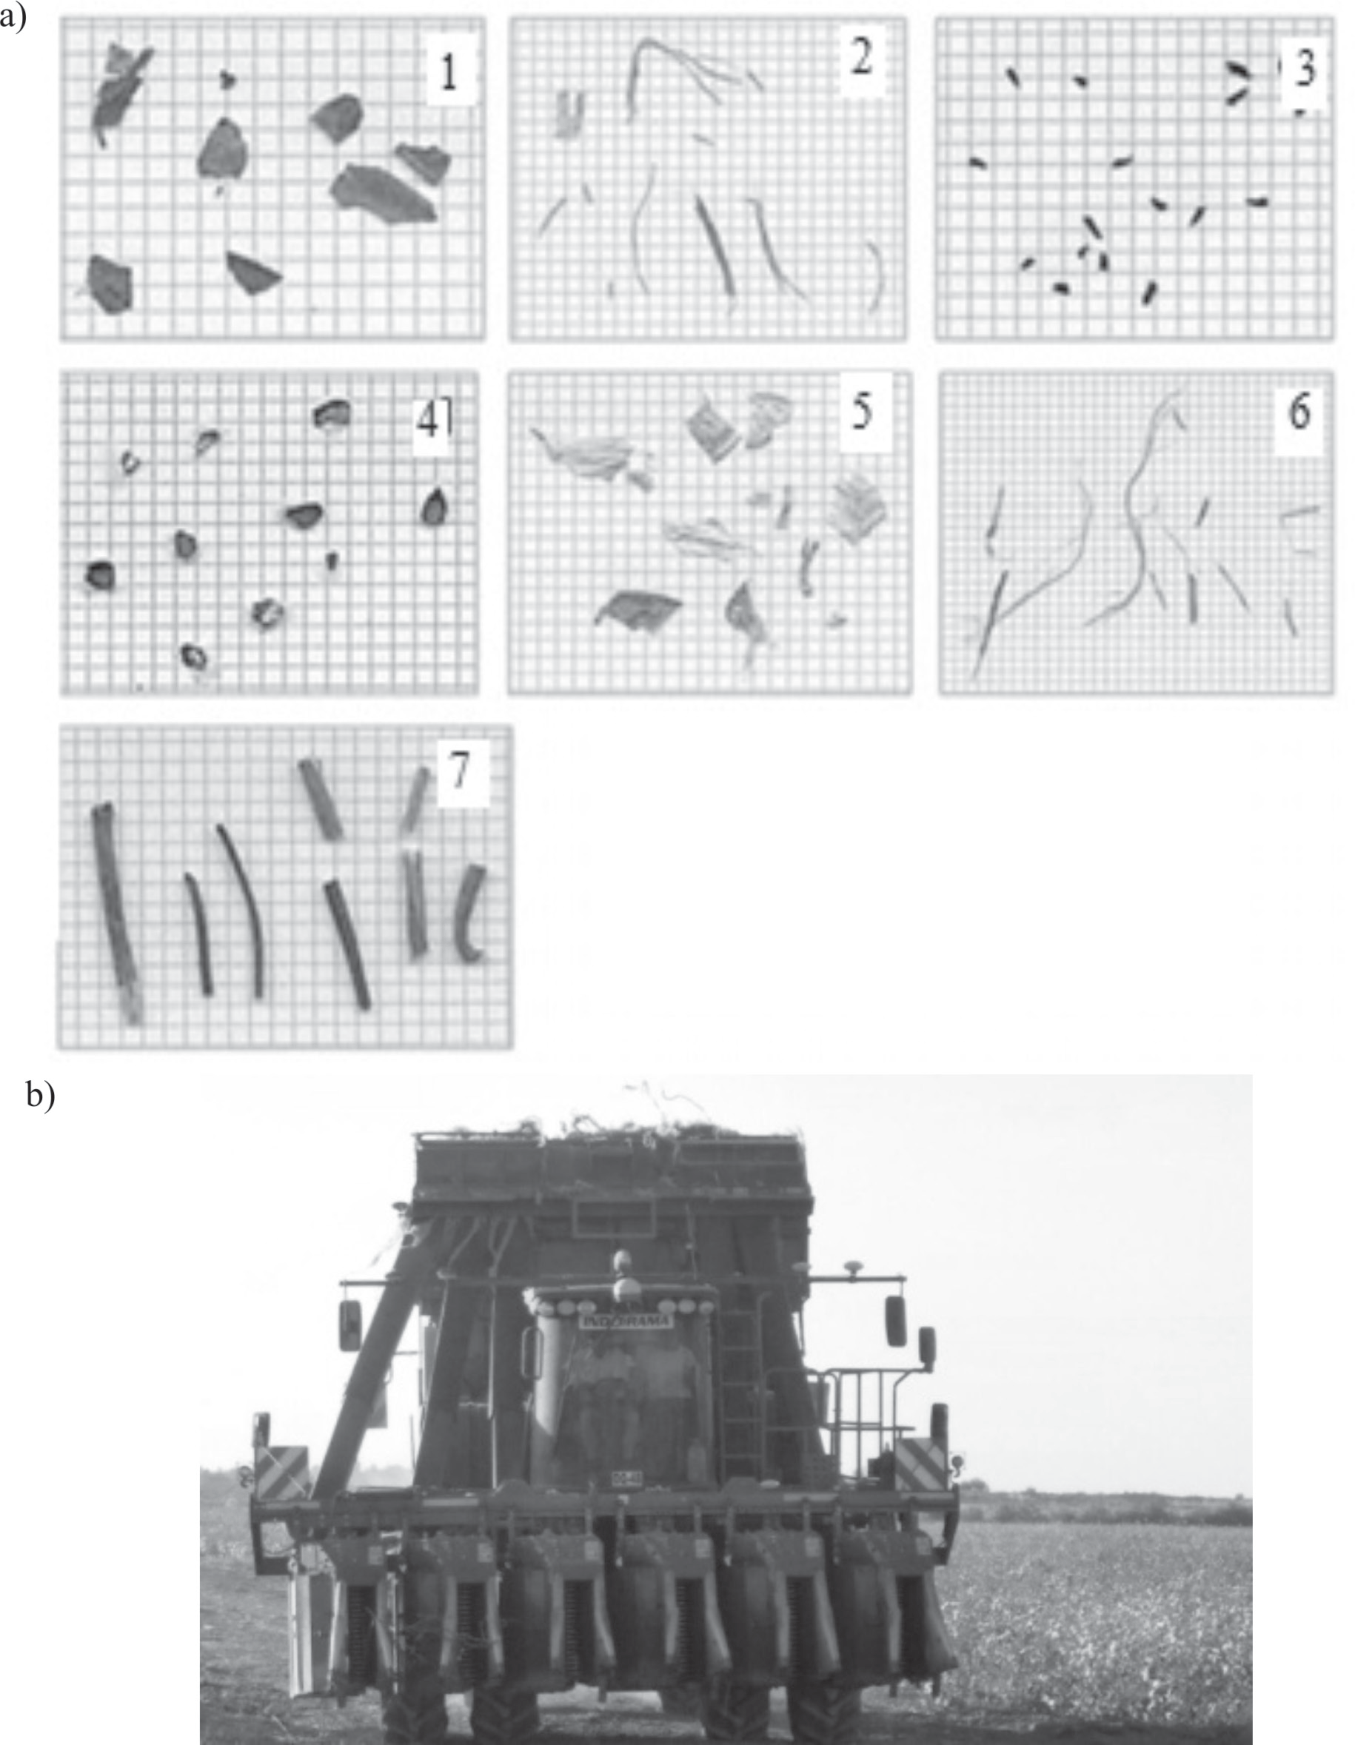
The study investigated the amount and types of pollution in machine and manual cotton. According to the study, the pollution was classified (Fig. 1a). Dirty is in the same classification. 1 - leaves, 2 - branches;
The analysis of the quality and type of contamination of cotton fiber, machine cotton, and the type and amount of impurities was investigated. The results revealed the impact of cotton picking on the amount of machine pollution and its processing. It is noted that the passage of pollutants into acute pollution is enhanced by machine picking [27, 28] (Fig. 1a).
In the Syrdarya and Jizzakh provinces, tests were carried out using cotton picked by hand, the Case-2020 machine, and the John Deere campaign based on the sampling technique.
Experimental
Materials and Methods
The moisture content of cotton depends on a number of factors, such as weather conditions during the harvest, cotton opening, field preparation, and other factors. Moisture is a major factor affecting the value of cotton in both commercial and technological quality. During the period of storage of cotton in high humidity, the biological process of the seeds goes on and produces heat. As a result, it reduces the quality of the cotton, which reduces the strength of the fiber, the level of fat in the seeds, and changes its appearance. In the process of processing, it complicates the smooth operation of technological equipment and drastically reduces the quality of products [29, 30].
The cotton moisture detection device VHS-1М (Pahtamash LLC, Tashkent, Uzbekistan) and the universal storage system USS-1 (Skaf LLC, Saint Petersburg, Russia) thermonam meter are used in cotton labs and cotton plants for the rapid detection of cotton, cotton fiber, and cotton seeds.
Fig. 1.
Classification of machine and hand picked cotton pollution a) 1 - leaf, 2 - stem, 3 - funiculi 4 - seed coat, 5 - shale, 6 - grass, 7 – steck; John Deere is a cotton picker b).
For testing on the USS-1 thermonuclear device (UzDst 644-2008), a standard 40 g sample size is collected from daytime skin. If the sample humidity is above 20%, two of the 40 g are taken. The average sample is obtained from 3-4 samples, as follows: 10-13 g of cotton in each jar, combined with the first sample, and weighed on an average of 0.01 g SLCC -500 (NPP Gosmetr, Saint Petersburg, Russia) electronic scale.
The operating temperature of the heating surfaces at test time with the USS -1 thermoelectric device is 195 ± 2. 40 g, testing with the USS -1 thermometer. The 40 g weight of cotton wrap is spread evenly over the surface of the aluminum mixture, and the clamp is closed. Then the “drying” button is pressed. After 4 minutes and 45 seconds, the instrument will sound a warning signal, and at 5 minutes, the “drying” light will go off, warning that the drying time is over. The dried sample was removed from the device and put into a separate container, then quickly removed from the container and weighed on a SLCC-500 electronic weighing scale of 0.01.
Cotton moisture (W) is calculated by the following formula:
Here: W- actual cotton moisture,%; mn - pre-drying sample weight, 40 g; mq - weight of the specimen after drying, g; 0.6- error rate of instrument.
One of the indicators that defines the quality of cotton is its impurities. The level of cotton contamination is the percentage of dirty impurities in it.
Cotton compounds are divided into 2 types according to their origin: organic and mineral.
Organic mixtures include cotton leaf slices, dried slices of flowers, slices of cotton wool, parts of the stem, dried, and rotten pieces of cotton.
Mineral compounds include dust, soil, fine rock, and others. The presence of mineral and organic pollutants in cotton causes a number of difficulties in cotton processing. It also has a negative impact on the natural quality of the cotton during storage at the cotton processing facilities.
In terms of acclimatization, it is divided into active and passive compounds. Active impurities are located on the inside of the cotton fiber and are tightly bonded to the fiber; cleaning them is difficult. Passive impurities are located on the surface of the cotton and are easily removed.
Depending on the size of the dirty impurities, they are divided into small and large impurities. Small pollutants are defined as impurities smaller than 10 mm. Large pollutants include impurities greater than 10mm.
State standard UzDst 592-2008 coordinates the methods of detecting cotton pollution. LKM instruments are used in cotton laboratories and reception centers for the rapid detection of cotton contamination.
The average daily amount of cotton is mixed on a flat surface (iron or plastic with a coating) so that dust and fine dust cannot be spilled. The sample is then mixed thoroughly and spread evenly in rectangular form, and evenly divided into four parts. The two opposing parts are removed together with dust and dirt, and the other two are still spread and divided into four. In this manner, continue until 1 kg of sample is left. The remaining cotton is measured at 300g on a scale whose degree of accuracy is 0.01.
If the moisture content of the sample is greater than 12%, then the sample is dried in the cotton dryer laboratory SHL-3 (Moscow, Russia).
300 g were obtained for experiments on a device for determining the clogging of cotton, the LKM-2 instrument (Tashkent, Uzbekistan). The weight of the cotton is put into the feeder bunker. Pressing the “Run” button, and as soon as the instrument starts working, the cover of the unit is pressed to ensure that the sample gets into the drum. In the first half, the cotton is removed from the dirt for 120 seconds, then gets into the second section, and for a further 45 seconds, it removes large impurities. In the second part, the sample falls into a box of purified cotton for 15 seconds.
During this process, the operating mode of the device will continue automatically. Using special flashing lights, the units work alternately. In the end, the instrument will stop automatically.
The pieces of cotton that fall into the box for dirty impurities are separated from the major impurities. Then the box with the cotton wool is removed, and the presence of large impurities is checked. If there are large, dirty impurities, they are added to the resulting impurities. The rotten parts of the cotton and the powders collected from the grapes are weighed to a depth of 0.01 g [31-33].
The percentage of cotton pollution (P) is calculated in percentages by the following expression:
where, where: mC - weight of impurities, g; mn - weight of cotton sample, g.
If the difference between the two levels of pollution in the two samples is less than 0.6% for cotton with up to 10% and more than 1% for cotton with more than 10%, then the average value of these indicators is used to find the actual contamination of cotton. If this difference is greater than the specified threshold, the third specimen designated for use shall be contaminated, and the mean value of the three indices will be determined. Experiments were conducted on the methods of determining the moisture and dirtyness of the cotton mentioned above [34, 35].
Results and Discussion
Before harvesting cotton, it is necessary to thoroughly destroy the field to be harvested. Defoliation is a process to reduce the level of cotton contamination and improve the quality of the products. Field deforestation, irrigation ditches, arches, and turning areas will be properly leveled before defoliation. Then the spraying units work evenly, increasing their productivity and defoliation. The effect of soil moisture on defoliation efficiency is significant. Therefore, the soil moisture content during the defoliation period should be 60-65%, against the limited field moisture content. If this figure is below 60%, the concentration of leaf and body fluid in the cotton will increase, the absorption of defoliants will decrease, and the effectiveness will decrease. Conversely, when the concentration of the plant is higher than 70%, the effect of defoliants decreases. It is advisable to provide light irrigation 10-12 days before the defoliation of very dry soils. One of the main factors determining the effectiveness of defoliants is air temperature. Each defoliant is subject to varying degrees of temperature depending on its chemical properties and mechanism of action. Therefore, it is necessary to take a clear air temperature forecast 7-10 days before defoliation and determine which defoliants to use and how long they should be used. In particular, if there is precipitation within 1-2 days after defoliation or if the temperature drops sharply, then this field will need to be re-defoliated. High temperatures can have a negative effect on cotton and reduce its productivity. Conversely, the use of defoliants at low temperatures can reduce the efficiency of the solution and increase costs. The duration of defoliation depends on the soil-climatic conditions of the regions, the biological nature of the varieties of cotton, and their availability [34-36].
Table 1.
Quality indicators of cotton harvested.
Artificial shedding and defoliation play an important role in the rapid and high-quality harvest of cotton, not leaving the cold and rainy days of autumn. This is a timely and quality event. In order to compare the dirt and humidity of the cotton harvested by hand and in the Sase-2020 machine (CNH Industrial America LLC, USA), in the Dustlik district of the Jizzakh region, a case study was carried out on the 1st «Genafon» selective breeder type. The results of the studies are presented in Table 1.
From the results, we can see from the table that the humidity of manual and machine cotton in homogeneous varieties and grades increases from 9.1% to 11%, and pollution increases from 7.1% to 10%, which is extremely harmful to the farmer and results in a sharp fall in cotton condensate weight. Secondly, there are many problems with processing and spinning such cotton.
The Syrdarya region is equipped with the latest six-line SP690 cotton pickers manufactured by JohnDeere, USA (Fig. 2b).
These innovative cotton pickers were tested for the first time by Indarama, a Singaporean company «Indarama», in the Akaltin district of the Syrdarya region.
A comparative analysis of the dirt and moisture content of cotton by hand-harvested cotton and by the John Deere Company SP690. In this case, samples of Sulton selection type cotton from type 5 cotton were sampled, and experiments were carried out on humidity and dirt from laboratory equipment from USS and LKM. The results are presented in Table 1.
From the results, we can see from the table that the moisture of the cotton and man-made cotton “SP690” by John Deere increased to 9.1% to 11.2% from 7.1% to 9.2%. It has a negative effect on the cleaning and harvesting of cotton, which is considered harmful. There are also many problems with spinning.
One of the most important features of cotton is the length of the staple fiber, i.e., the longer the fiber, the better the quality of the yarn. The length of a fiber - its quality is measured by indicators of the distribution law of length. There are two methods for determining the length of the fibers, which are performed manually and on instruments. Fiber lengths “Modal” and “Staple” are widely used [36, 37].
Modal length is the most common length in a sample. The staple length is Lsht = Lmod + (3: 4) mm.
The HVI-1000 system has been used in recent years to detect fiber properties. In this system, the following parameters of the fiber length are accepted:
High average length is the average length of the longest fibers in the sample and is called 2.5% length;
Staple length is the measured length of the fiber staple manually paralleled by the classifier;
50% length is the amount of fibers capable of spinning;
Average length shows the average length of all the fibers in the sample.
UzDSt - 604-2016 is a technical specification of cotton fiber that contains the requirements for the classification of cotton fiber.
Cotton fiber is divided into 9 types according to properties such as staple length, linear density, and relative tensile strength. These indicators analyze the quality of manual and machine cotton.
Hand-sorted breed of JCS “Dustlik cotton cleaning” AnB-2 (1/2) cotton staple length, percentage of dirty particles in the detection area, number of dirty particles in the detection area, micronaire index, comparative tensile strength, and high fiber content results were obtained for the average length parameters. The results are presented in Table 2.
Sase-2020 “Dustlik cotton cleaning” stock type selection type AnB-2 (2/2) cotton staple length, percentage of dirty particles in the detection area, number of dirty particles in the detection area, microwave polarity, granularity index, information on short fiber content, and high average length indicators. The results are presented in Table 2.
From the results of the table, we can see that the staple length of the manual and cotton class SP690 in the same grade and class decreased by 28.7 mm to 28.2, or 0.5 mm. The number of dirty particles in the detection area increases from 20 to 37. These indicators have a negative impact on the quality of the yarn during spinning.
The results obtained in the tables, which affect spinning, are mainly the number of cotton fibers (Fiber Nep count) and fiber staple length, the quantity of cotton fiber staples, and the staple length of fiber. Experimental test results have been carried out in the laboratory of the foreign joint venture Jizzakh textile LLC (Tashkent, Uzbekistan). The experiment was carried out on a USTER AFIS PRO 2 (Uster Technologies AG (HQ), Uster, Switzerland) device and weighed 0.55 g of the sample.
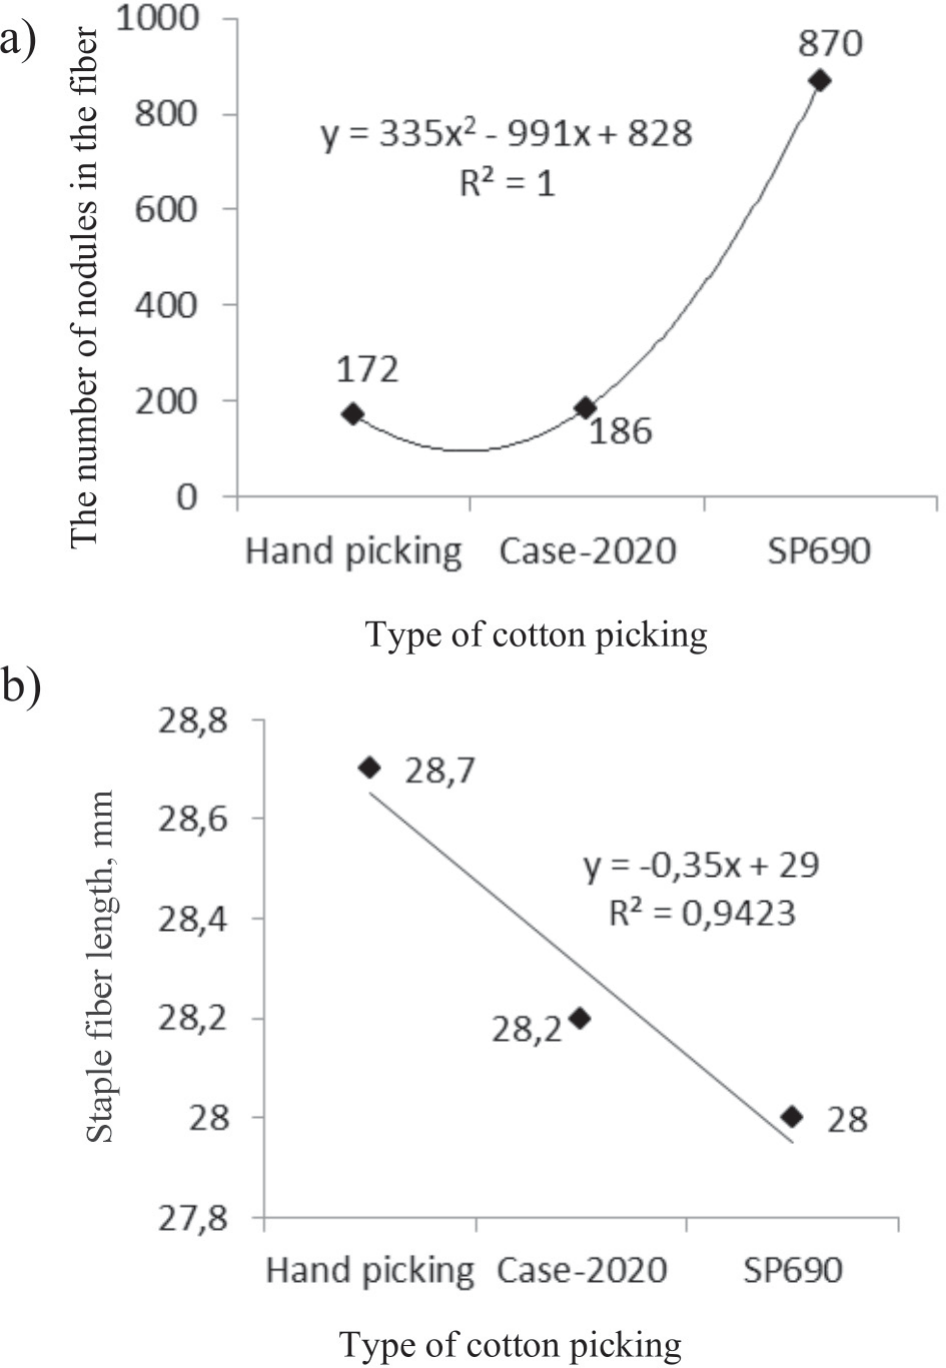
(Fig. 2a) As shown by the method of cotton picking, namely SP690, Sase-2020, and hand-picked cotton in the laboratory, the quality of the fibers was 870, 186, and 172. Based on the results, we can say that the cotton harvested on the SP690 machine is higher. This indicator affects not only the quality of the yarn obtained during the processing of cotton, but also the spinning, which results in the loss of fiber due to the removal of the cloths in it. (Figure 2 b), when investigating the effect of the type of cotton harvest on the fiber staple length, it was 28, 28.2, and 28.7 mm. As we know, every millimeter of fiber has a major impact on the quality of the fiber. That is why the fiber is sold in 9 types. According to the results, the staple length of the fiber is 28 mm, which is shorter when dialed on the SP690. We can see that these figures decreased by 0.7 mm compared to the hand harvest [35-44].
Table 2.
Quality indicators of cotton harvested.
Conclusions
It can be said that when the cotton was harvested from the Sase-2020 car and the SP690 harvesters from the US John Deere campaign, the moisture content in the cotton was 9.1%, 11% in the Sase 2020 machine, and 11.2% in the SP690 machine. This results in a drastic change in the quality of cotton harvested on 11.2% of cars. Cotton pollution was 7.1% in hand, 10% in Sase 2020, and 9.2% in SP690. Based on the results, the cotton harvested on the Sase 2020 machine is more dirty than the SP690 machine, so it is necessary to increase the initial cleaning process of the cotton harvested on the Sase 2020 machine. The number of fibers in a laboratory is 55 g. During the sampling experiments, there were 172 units of hand-picked cotton, 186 in the Sase 2020 machine, and 870 in the SP690. Based on the results, we can say that the cotton harvested on the SP690 machine is higher. This indicator affects not only the quality of the yarn obtained during the processing of cotton, but also the spinning, which results in the loss of fiber due to the removal of the cloths in it. The length of the staple fiber was 28.7 mm for hand-picking, 28.2 mm for Sase 2020 car assembly, and 28 mm for SP690. According to the results, the staple length of the fiber is 28mm when it is dialed on the SP690. We can see that these figures decreased by 0.7 mm compared to the hand harvest. As we know, every millimeter of fiber has a major impact on the quality of the fiber. That is why the fiber is sold in 9 types. There are also many problems with spinning. This implies the need to improve the processes of drying and cleaning for cotton during its initial processing, as well as the process of cleaning the yarn.

