

Introduction
In recent years, a large number of industrial factories have been removed from the city center as the process of urbanization progresses in China [1, 2]. Due to the poor environmental management of industrial factories over a long period of time (e.g. tank leakage, wastewater discharge, and illegal landfilling of chemicals), some of the retired sites were found to be polluted [3]. Among these brownfields, a considerable proportion of them were HM-contaminated sites, especially those sites that once served as electroplating plants, e-waste recycling plants, and metallurgical plants [4-8]. HM-contaminated sites are proven to be threats to human health, and various remediation processes have been studied and applied to solve the problem [1, 9, 10].
In general, traditional remediation processes for HM-contaminated sites include excavation and dumping [11], stabilization, and mobilization [12, 13]. Among these, excavation and dumping of HM-contaminated soil have been utilized in the early days, but it is not currently promising because the landfill resources in well-developed areas of China are very precious (such as Shanghai, Zhejiang province, and Jiangsu province), and HM pollutants tend to leach out and transform into leachates, which are threats to the leachate treatment system [14]. Except for excavation and dumping, another popular remediation method for HM-contaminated sites is the stabilization process. However, many stabilization processes utilize in situ remediation techniques, and HMs still remain in the field after stabilization. The remaining HMs will be a concern in the future if the stabilization system is destroyed after extracting saltwater and acid rain for many years [15]. The third approach is mobilization, which includes chemical soil washing and phytoextraction. According to the research, chemical soil washing can lead to the production of HM-polluted water/sludge and may change the basic characteristics of soil [16, 17]. As an environmentally friendly process, phytoextraction is limited by the concentration of pollutants and plant growth conditions [18].
To accelerate the remediation of contaminated soil and alleviate land use pressure, some contaminated soils are allowed to be treated by cement kilns in China [19]. This approach has been proven to be effective because it can effectively decompose organic pollutants and solidify HMs. However, with the adjustment of industrial structures in China, small and medium-sized cement kilns are being demolished. Only a small number of large-scale cement kilns (5000 t/d) still exist, which means that even though the cooperative disposal of cement kilns is an effective technology for remediating contaminated soil, not all cities have large cement kilns. Therefore, except for cement kilns, if there is any other system that has similar high temperatures, can the kiln structure be considerably similar to that of the cement kiln?
Based on the above considerations, as a sort of thermal system with considerable quantity in southeast China, the ceramsite roasting system was proposed in this paper. According to our research, the ceramsite manufacturing industry is flourishing in China. In 2021 and 2022, the production of ceramsite in China reached 12.54 and 13.85 million cubic meters, respectively. A typical ceramsite roasting line consists of pretreatment equipment (i.e., sieving and stirring machines), a granulator, a drying kiln, and a rotary kiln (kiln temperature from 200ºC to 1100 ºC and residence time from 30 mins to 60 mins). Put simply, the process of preparing ceramsite is to heat the soil pellets to the melting point, then cool and harden them. Common raw materials for ceramsite preparation include shale, underground soil, fly ash, and sludge [20-22]. Relevant studies and cases using HM-containing sludge showed that organic pollutants were effectively decomposed and HMs were inert after high-temperature roasting. After cooling, the surface glaze layer of ceramsite can act as a barrier to prevent HM leaching. As mentioned above, it seems that the ceramsite roasting system has possessed some objective conditions for treating HMs-contaminated soil.
However, polluted soil from industrial contamination sites often contains high concentrations of HMs and is much better than conventional raw materials for making ceramsite. From some studies on waste incineration, it can be found that HMs migrate and transfer during waste incineration [22, 23] (i.e. HMs are also likely to migrate during ceramsite preparation). The temperature of a ceramsite kiln is between the temperatures of the cement kiln and the municipal solid waste (MSW) incinerator (1450℃ - 850℃). The behavior of HM-contaminated soil during the ceramsite preparation process cannot be directly extrapolated from studies conducted on cement kilns or municipal solid waste (MSW) incinerators. Additionally, variations in raw materials, residence time, and temperature may lead to differences in the stability of HMs in ceramsite compared to bottom slag produced by MSW incinerators and cement kilns. At present, there are few studies on the preparation of ceramsite using HM-contaminated soil, especially on the stabilization of the prepared ceramsite [24, 25]. As a versatile material, ceramsite can be used as a building material, culture substrate, and industrial filter media; therefore, in these scenarios, it is of great practical significance to study the stability of residual HMs in ceramsite products prepared from contaminated soil. Hence, in this study, two types of contaminated soils were used to produce ceramsite. The stability of HMs in ceramsite was systematically investigated by conducting HMs leaching tests, long-term acid rain extraction, metal speciation analysis, and characterization of mineral morphology and microstructure.
Materials and Methods
Materials
Two types of soil samples containing different amounts of HMs were selected, which were marked as C1-soil and C2-soil. The soil samples were prepared by adding HM solvent and placing them on the balcony for drying and weathering for 1 month before testing. The HMs of copper (Cu), zinc (Zn), lead (Pb), chromium (Cr), and nickel (Ni) were chosen in this study for their universality in the retired sites of the electroplating factory, electronic waste dismantling plant, and smelt factory. The concentrations of Cu, Zn, Pb and Ni were referred to as the risk screening values and risk intervention values for the second category of development land as defined by the Chinese National Standard “Soil Environmental Quality: Risk Control Standard for Soil Contamination of Development Land (GB36600-2018)” [26]. Given that the risk screening value and intervention value of Cr(VI) for the second category of development land in the GB36600 standard are both lower than 100 mg/kg, the leaching and residual amount may not be detected when the soil is prepared into ceramic particles. Therefore, this study increased the concentration of Cr(VI) in the C1-soil and C2-soil to 1000 mg/kg, and 2000 mg/kg, respectively. Consequently, the concentrations of Cu, Zn, Pb, Cr, and Ni in the C1-soil were 18000 mg/kg, 10000 mg/kg, 800 mg/kg, 1000 mg/kg and 900 mg/kg, respectively; for the C2-soil, the concentrations of Cu, Zn, Pb, Cr, and Ni were 36000 mg/kg, 20000 mg/kg, 2500 mg/kg, 2000 mg/kg, and 2000 mg/kg, respectively.
Ceramsite Roasting Experiment
As the ceramsite kiln used during industrial production is a horizontal rotary kiln, the roasting tests were conducted on a horizontal tube furnace (the diameter was 4 cm, the length was 90 cm, and the maximum temperature was 1500ºC). Before being placed in the tube furnace, the prepared HM-contaminated soil was ground to less than 1 mm. A certain proportion of distilled water was added to the soil for moisture content adjustment before granulation (when the moisture content is approximately 45%, the soil can be processed into pellets). After the contaminated soil pellets were inserted into the furnace, the temperature in the furnace gradually increased from 25ºC to 1100ºC with an air injection of 15 mL/s. The residence time of the pellets was controlled at 45 minutes, as conducted in some ceramsite factories. When the furnace temperature reached 200ºC, 500ºC, 800 ºC, and 1100ºC, the pellets inside were removed from the furnace for subsequent testing.
To study the migration of HMs away from the material during the calcination process of ceramsite, the residual HMs content in the ceramic pellets was measured. In addition, the tube furnace was equipped with gas absorption bottles (500 mL mixture of 5% HNO3 and 10% H2O2) to capture HMs. These HMs captured by the absorption liquid were considered to have escaped from the ceramsite kiln and migrated to the subsequent flue gas purification system.
Metal Speciation Analysis
To study the transformation process of HM speciation from raw materials to ceramsite, a BCR (Community Bureau of Reference) extraction test was conducted on the HM soil. Intermediate products and final ceramsite (pellets taken from the furnace at 200ºC, 500ºC, 800ºC, and 1100ºC) were used in the BCR test. According to the definition of BCR leaching, HMs were analyzed in 4 categories: ① Acid soluble / exchangeable fraction, ② Reducible fraction, ③ Oxidizable fraction, and ④ Residual fraction.
Leaching Tests
To assess the risk of HM release during the use of ceramsite as a building material and greening filler, the HM-contaminated soil and final ceramsite were analyzed via the TCLP (toxicity characteristic leaching procedure), SPLP (synthetic precipitation leaching procedure), and DTPA (diethylene-triamine penta acetic acid; the phytoavailability of HMs was measured by a single step extraction of DTPA, which was the leachate) leaching tests.
To evaluate the environmental risks of the long-term use of ceramsite, a simulated acid rain leaching experiment was set up. The simulated acid rain was prepared according to the characteristics of acid rain in southeast China (the concentration of SO42-, NO3-, and Cl- in the simulated acid rain was 104.8 mg/L, 16.1 mg/L, and 20.8 mg/L, respectively, and the pH was adjusted to 5.5).
In order to simulate the worst scenario, the ceramsite obtained by roasting was ground into sizes smaller than 8 mm and then placed in a polyethylene bottle with a small hole at the bottom. The diameter of the polyethylene bottle was 5 cm, and approximately 150 g of ceramsite fragment were in each bottle. Because the annual rainfall in Zhejiang is approximately 1500 mm, the total rainfall in one year can be completed in approximately 30 days under continuous heavy rainfall (49.9 mm/d). According to the size of the bottle mouth, the flow rate of the acid rain was controlled at 392.5 mL/d. Acid rain from the bottom hole of the bottle was collected periodically for further analysis.
Analytical Methods
The leaching liquid and HM absorption liquid were all filtered by a 0.22 μm membrane and analyzed by atomic absorption spectrophotometry (AAS, 700 P, Analytik Jena, Germany) in triplicate. Solid materials, such as soil, raw pellets, and ceramsite pellets, were dried at 10ºC and ground into powder (less than 100 mesh). Then, each sample was digested with HNO3 / HClO4 / HF. To analyze the microstructure and morphological mineral changes in the HMs during the ceramsite roasting process in detail, scanning electron microscopy (SEM) and X-ray diffraction (XRD) were applied in this study.
Results and Discussion
Environmental Migration of HMs
Although the peak temperature for ceramsite roasting reached 1100 ºC, there was still a certain amount of HM residue in the ceramsite. Based on the amount of HMs remaining in the ceramsite, enrichment behaviors of Cu, Zn, and Cr were found (as shown in Table 1). The enrichment indexes were calculated by Equation (1).
Table 1.
Average concentration enrichment of HMs after roasting.
| HMs | Cu | Zn | Pb | Cr | Ni |
|---|---|---|---|---|---|
| Enrichment | 1.31 | 1.13 | 0.53 | 1.28 | 0.76 |
where: h represented one of the 5 HMs (i.e. Cu, Zn, Pb, Cr, and Ni); C(h, ceramsite) was the HM concentration of ceramsite, mg/kg; C(h, soil) was the HM concentration of soil, mg/kg.
This result showed that after the HM-contaminated soil was completely treated according to the ceramsite roasting process, the concentrations of these three HMs (Cu, Zn and Cr) in the ceramsite were higher than those in the original material. The concentration of Cu reached 1.31 times that before calcination, which was the most significantly enriched among the five HMs. Cr showed the second concentration enrichment ability, with an enrichment index of 1.28. The concentrations of Zn are basically the same as before roasting, with an enrichment concentration of 1.13. In contrast, the concentrations of Pb and Ni in ceramsite decreased compared to those before roasting. The roasting process of ceramsite was equivalent to the removal process, especially for Pb (the concentration of Pb in ceramsite was only 53% of the raw soil sample).
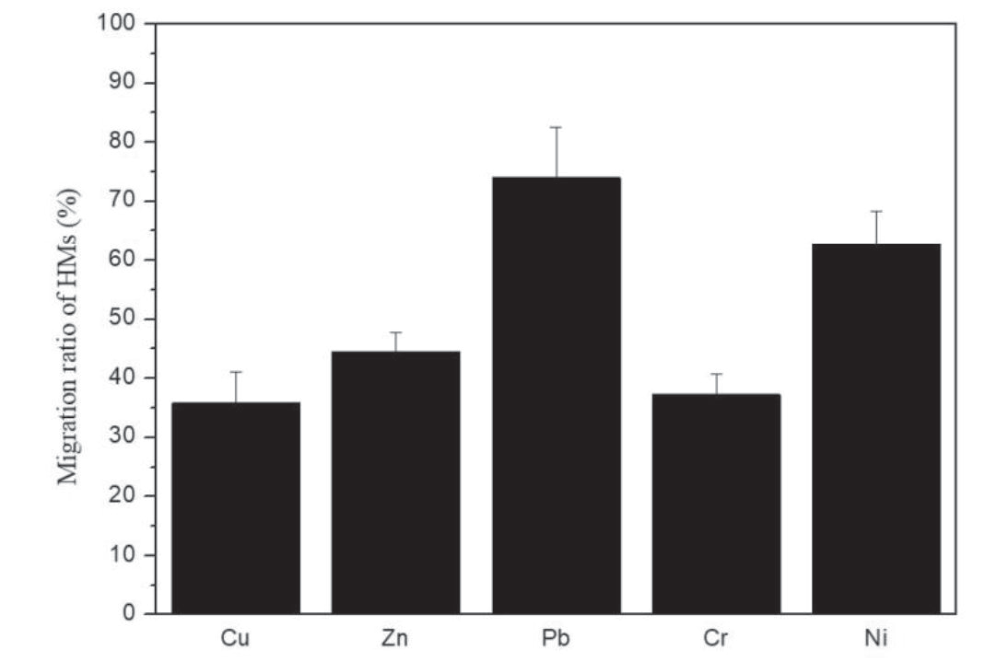
In terms of the roasting process, the migration of HMs was observed by detecting the absorbed liquid, which is shown in Fig. 1. Approximately 35.81% of Cu, 44.63% of Zn, 74.03% of Pb, 37.28% of Cr, and 62.76% of Ni in the soil sample (by average) migrated to the absorbed liquid. Based on this result, when the HM-contaminated soil was used to prepare ceramsite on a large scale, the HMs in flue gas needed to be focused and treated.
HM Leaching Risk
According to the leaching results of SPLP, after the contaminated soil was made into ceramsite, the leaching concentrations of the HMs showed very significant decreases (as shown in Table 2). The average SPLP leaching values of Cu, Zn, Pb, Cr and Ni in the C1-soil were 998.67 mg/L, 697.33 mg/L, 10.18 mg/L, 21.07 mg/L, and 55.10 mg/L, respectively, which means the leaching ratios were 18.49%, 22.64%, 4.24%, 7.02%, and 18.37%, respectively. After being made into ceramsite, the average SPLP leaching values of Cu, Zn, Pb, Cr, and Ni decreased to 3.67 mg/L, 0.33 mg/L, 0.03 mg/L, 0.01 mg/L, and 0.02 mg/L, respectively, which means the leaching ratios were 0.09%, 0.01%, 0.03%, 0.01%, and 0.03%, respectively. It indicated that the leaching concentrations of HMs can be reduced by more than 99.99% compared with the raw materials. It should be noted that the concentrations of Cu, Zn, and Cr in ceramsite were higher than those of the raw materials. Similar patterns in the high-concentration raw material experimental group were also found. According to the calculation, only 0.012% of Cu, 0.005% of Zn, 0.02% of Pb, 0.007% of Cr, and 0.017% of Ni can be leached out of ceramsite, which means most of the HMs were not able to leach out during the SPLP tests.
The results indicated that the higher the concentration of HMs in the raw materials, the higher the concentration of HMs leached from the prepared ceramsite. However, the difference in leaching concentration is not particularly significant. For example, the leaching concentration of Cu is 3.67 mg/L in C1-Cermsite and 4.18 mg/L in C2-Cermsite, which is twice the difference in Cu concentration in the raw materials of the two. This conclusion also applies to the description of the leaching patterns of the other four HMs. It should be noted that the leaching concentration of Cu in C1-Cermsite reached 3.67 times the Class III limit of the Chinese National Standard GB/T 14848- 2017 [27], while the leaching concentration of the other four metals was lower than the corresponding limit. This means that ceramsite prepared from Cu contaminated soil with a high concentration can lead to an increase in Cu concentration in surrounding groundwater in an inorganic acid environment.
In the TCLP leaching results, the solidification effect of ceramsite on HMs was observed (as shown in Table 2). The HMs leaching concentration of the C2-soil in the TCLP was very high, but after the C2-soil was made into ceramsite, the leaching concentrations of the HMs all dropped by more than 99.99%. According to the calculation of the leaching ratio, it can be concluded that the leaching ratios of Cu, Zn, Pb, Cr, and Ni in C2-Ceramsite were 0.09%, 0.01%, 0.03%, 0.01%, and 0.03%, respectively, while the leaching ratios of the five HMs in C2-soil reached 47.94%, 45.18%, 33.75%, 17.76%, and 41.78%, respectively. It was found that the leaching concentrations of Cu and Zn in C1-Cermsite and C2-Ceramsite were higher than the Class III limits of the Chinese National Standard GB/T 14848-2017, which indicated that ceramsite prepared from Cu and Zn contaminated soil with high concentrations can lead to an increase in Cu and Zn concentrations in surrounding groundwater in an inorganic acid environment.
The results of the HMs extracted by the DTPA solution are reflected in Table 2. After the contaminated soil was roasted, the bioavailability of HMs also dropped significantly (DTPA leaching concentration can be reduced by more than 99.9%). The average leaching ratios of Cu, Zn, Pb, Cr, and Ni in C1-soil and C2-soil were 3.76%, 13.9%, 3.93%, 0.08%, and 22.23%, respectively, while the average leaching ratios of the five HMs in C1-Cermsite and C2-Ceramsite dropped to 0.05%, 0.07%, 0.05%, 0.01%, and 0.07%. Through the analysis of leaching concentration, it can be found that the HM leaching concentration of the C2-Cermsite group is 2 to 13 times higher than the corresponding leaching concentration of the C1-Cermsite group, indicating a significant difference in leaching concentration compared to SPLP and TCLP. This result showed that the concentration of HMs in plant absorbable forms released by ceramsite is also significantly influenced by the concentration of HMs in the raw materials. In addition, ceramsite prepared from soil contaminated with high concentrations of HMs may still be absorbed by plants when it is used for greening purposes.
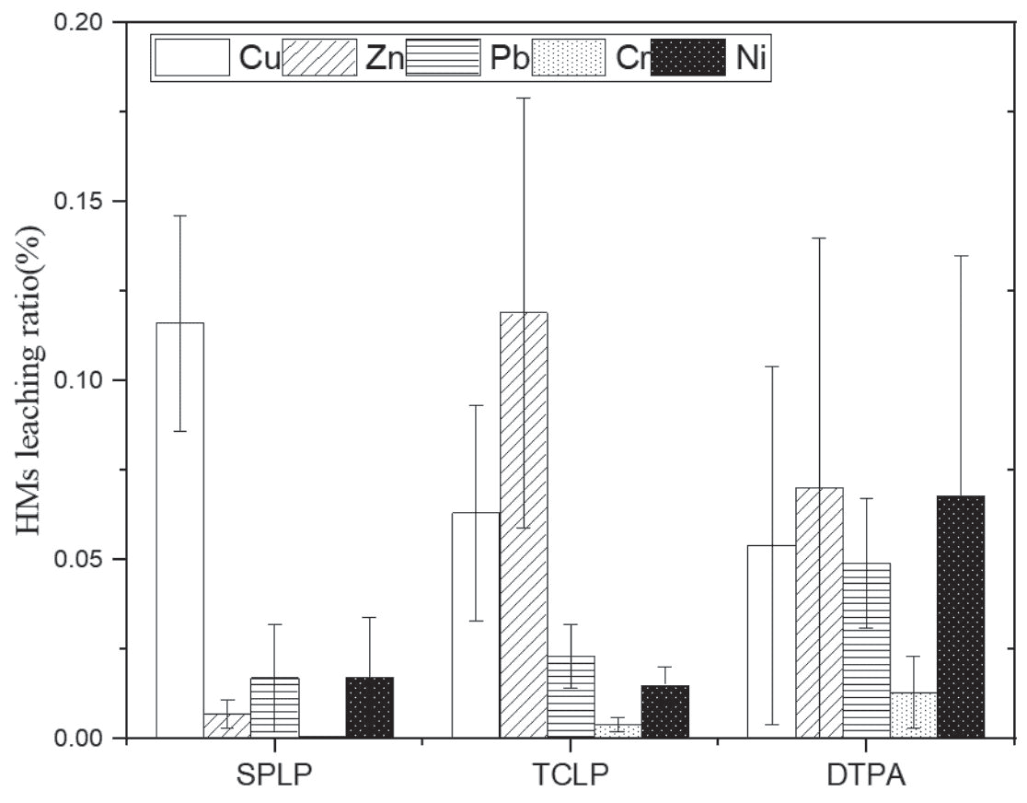
By comparing the stabilization effects of the ceramsite roasting process on HMs, some differences were found. In the SPLP group, Cu showed the highest leaching ratio (the average leaching ratio was 0.12%), followed by Pb. However, in the TCLP group, Zn tended to leach out more than the other HMs, with an average leaching ratio of 0.11%. In addition, ceramsite had the best stabilization effect on Cr (as shown in Fig. 2).
Long-term Acid Rain Extraction
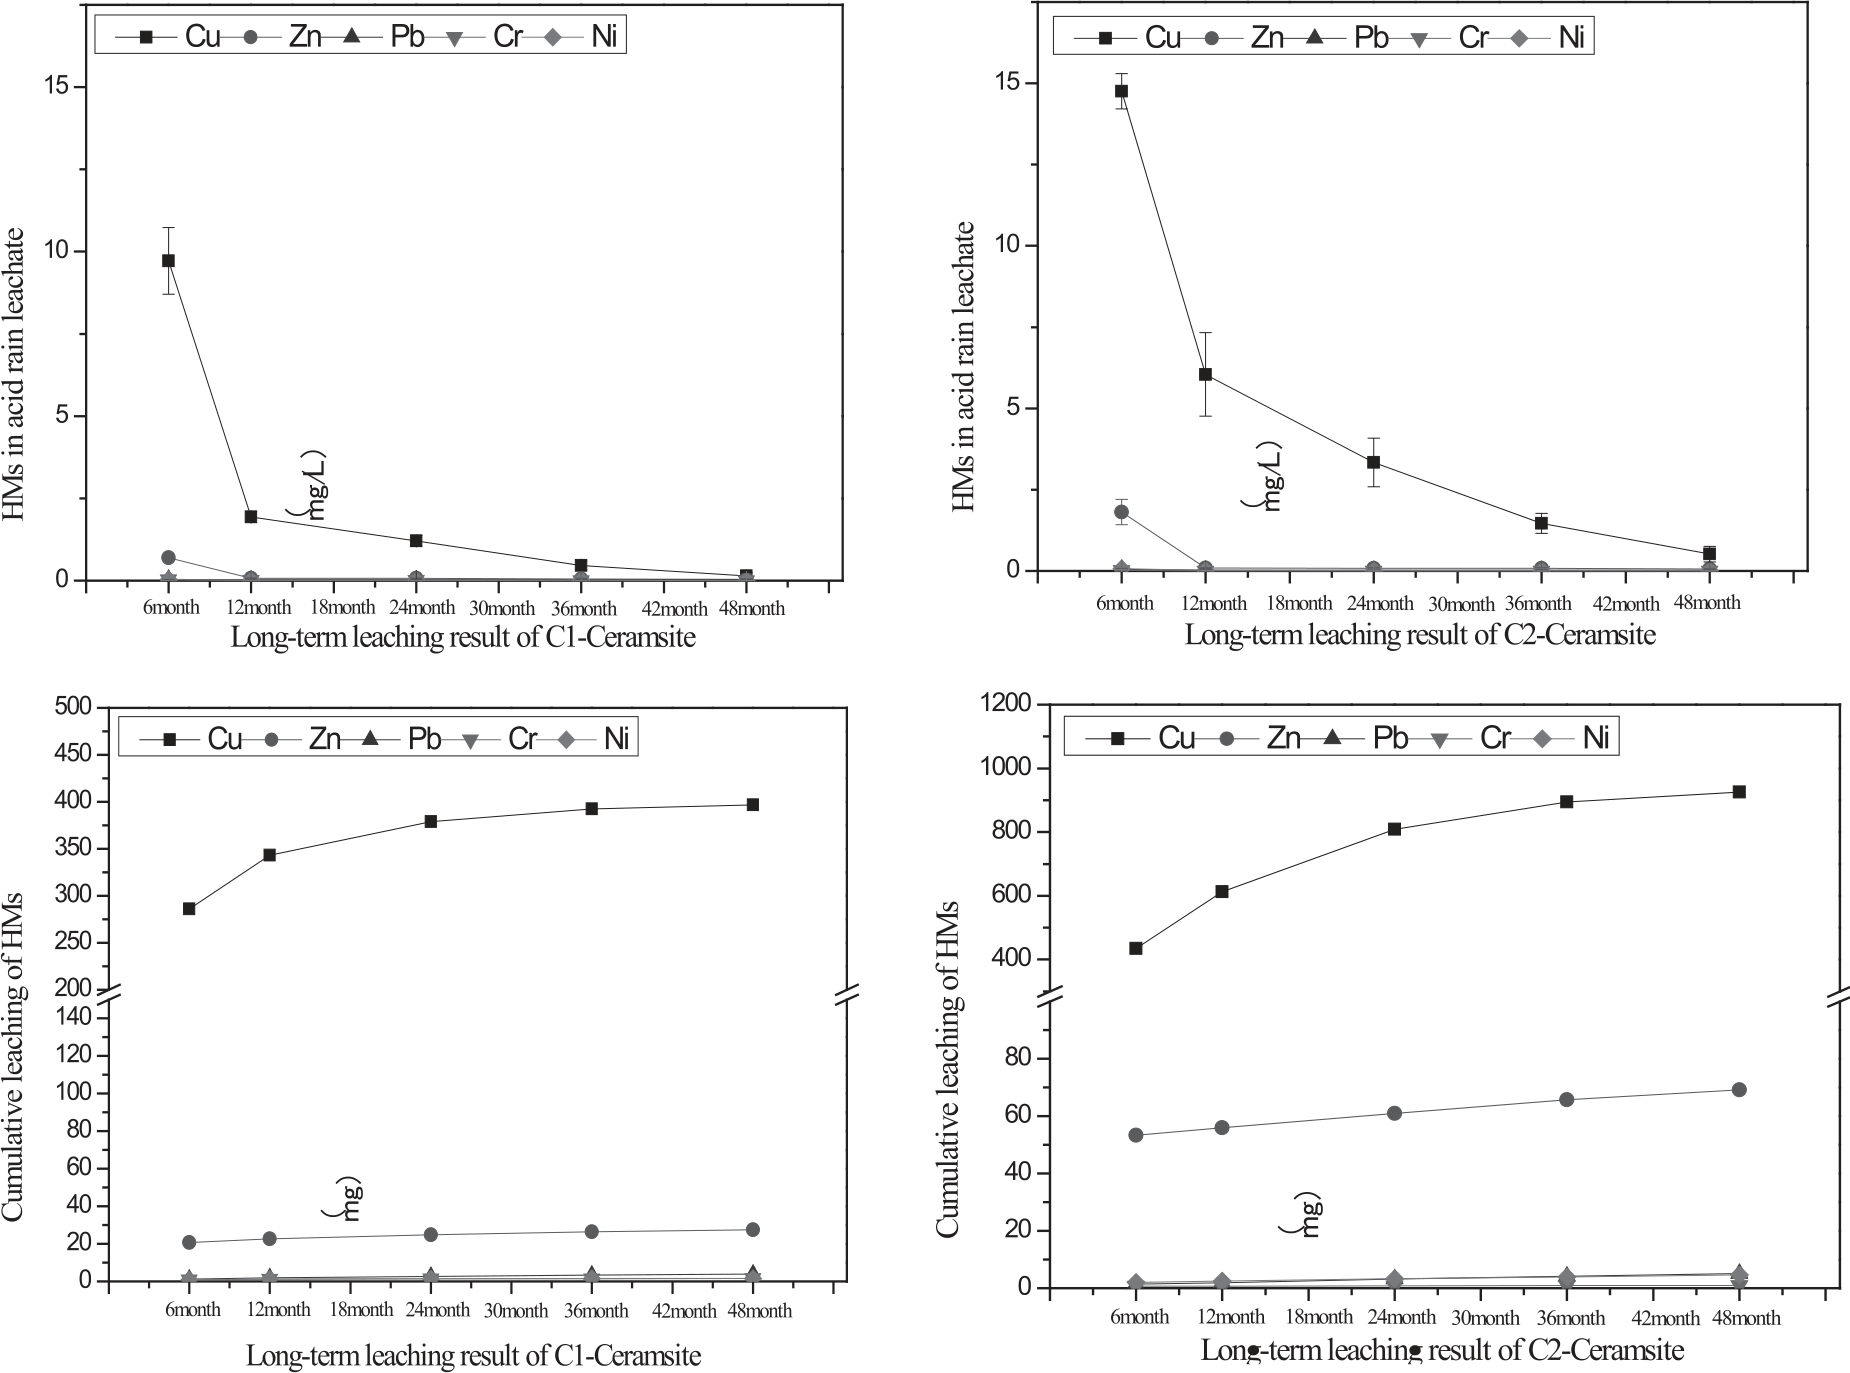
According to the results of acid rain extraction (Fig. 3), the leaching concentration of HMs gradually decreased with a prolonged acid rain extraction time (the first 36 months comprise the fast release stage). In the early stages of acid rain leaching, the leaching concentrations of Cu and Zn were relatively high (even higher than the corresponding SPLP leaching concentrations). The leaching concentrations of Cu in C1-Ceramsite and C2-Ceramsite were 9.72 mg/L and 14.76 mg/L, respectively. In contrast, the leaching concentration of Cu in the corresponding SPLP experimental group did not exceed 5 mg/L. Similarly, Zn was also released at high concentrations during the initial six months, with leaching concentrations reaching 0.7 mg/L and 1.81 mg/L in the C1-Cermsite and C2-Cermsite experimental groups, respectively. This result may be due to the presence of calcium and magnesium ions in simulated acid rain compared with the SPLP solution, which benefits the dissolution of HMs. In addition, according to the results, the leaching concentrations of Cu were 0.147 mg/L in the C1-Ceramsite group and 0.517 mg/L in the C2-Ceramsite group after 48 months of acid rain extraction, both lower than the Class III limit of the Chinese National Standard GB/T 14848-2017 (1.0 mg/L). In the early stages of acid rain extraction, the leaching concentrations of Pb, Cr, and Ni were relatively low (under 0.1 mg/L), and these concentrations continued to decrease over time. Overall, under the condition of acid rain extraction, the leaching concentrations of these five HMs basically exhibited a decreasing trend from high to low. On the other hand, approximately 12.1% of Cu, 1.83% of Zn, 4.34% of Pb, 0.55% of Cr, and 1.82% of Ni leached out after 48 months of acid extraction in the total calculation. It represented that in the ceramsite solidification system, Cu was relatively easy to leach in the acid rain leaching environment, followed by Pb, Ni, and Cr.
Table 2.
Leaching result (mg/L).
Transformation of HM Speciation
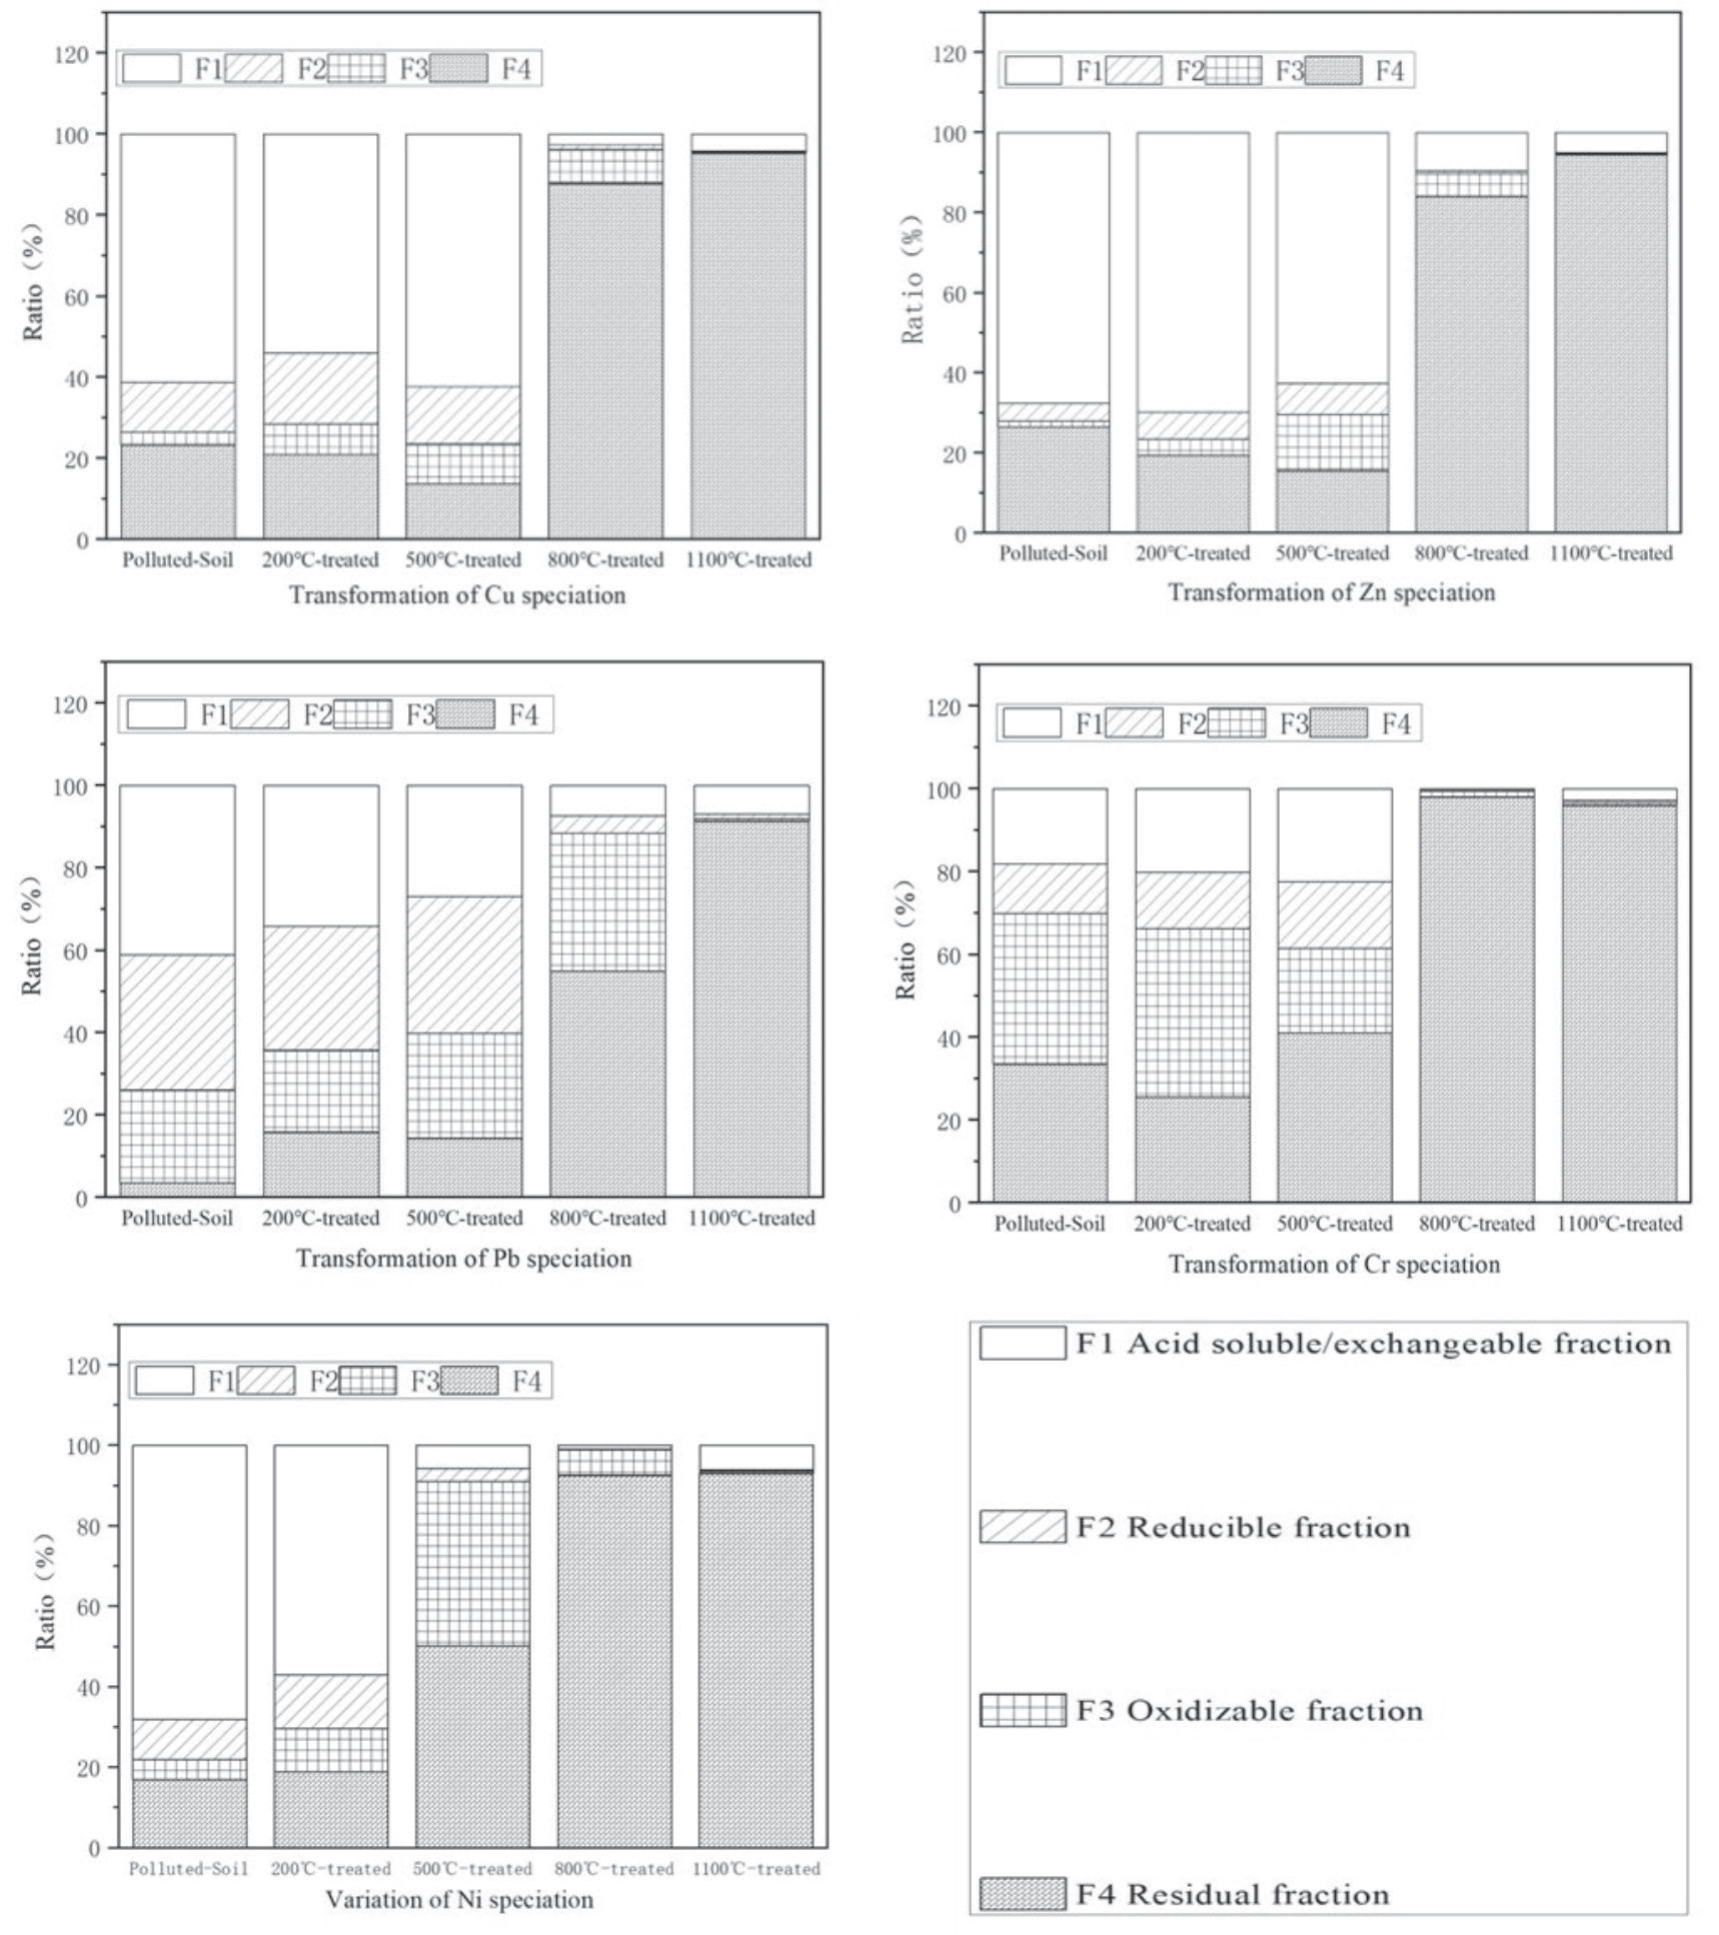
The transformation of HM speciation during roasting is shown in Fig. 4. As the calcination temperature increased to 800ºC, the HMs gradually transformed toward the residual fraction (F4). The metals in F4 have the strongest binding with the crystal structure of minerals, making it difficult to separate [28]. The proportion of residual fractions of Cu and Zn tended to decrease slightly when the HM-contaminated soil was heated from room temperature to 500ºC. During this process, the proportion of components (F1, F2, and F3) that easily migrated into the environment in Cu and Zn increased. In terms of Pb, as the temperature increased from 200ºC to 500ºC, the proportions of F1, F2, and F3 remained stable. When the roasting temperature reached 800ºC, the proportions of F1 and F2 obviously decreased, while the proportions of F3 and F4 increased. For Cr, the proportions of F1 and F2 continued to increase during the heating process (from room temperature to 500ºC). For Ni, F3 showed an increasing period during the roasting process from room temperature to 500ºC. For all five HMs, after roasting at 1100ºC, the HM content of F4 accounted for over 90% of the ceramsite, and the remaining fraction was composed of the acid soluble/exchangeable fraction. According to what was mentioned above, the HMs gradually changed to more stable chemical forms during the ceramsite process, which also explained why the leaching concentration of the HMs in ceramsite decreased significantly compared with the raw material. Besides, Fig. 4 illustrates that a small amount of F1 still exists in ceramic particles (1100ºC), in other words, the roasting temperature of 1100ºC cannot completely eliminate the acid soluble fraction of HMs. The proportion of Cu, Zn, Pb, and Cr, Ni in F1 was 4.27%, 5.13%, 6.96%, 2.62 %, and 6.10%, respectively. The residual F1 may be the reason why HMs are still leached in TCLP, SPLP, and acid rain extraction.
Changes in Mineral Morphology and Microstructure
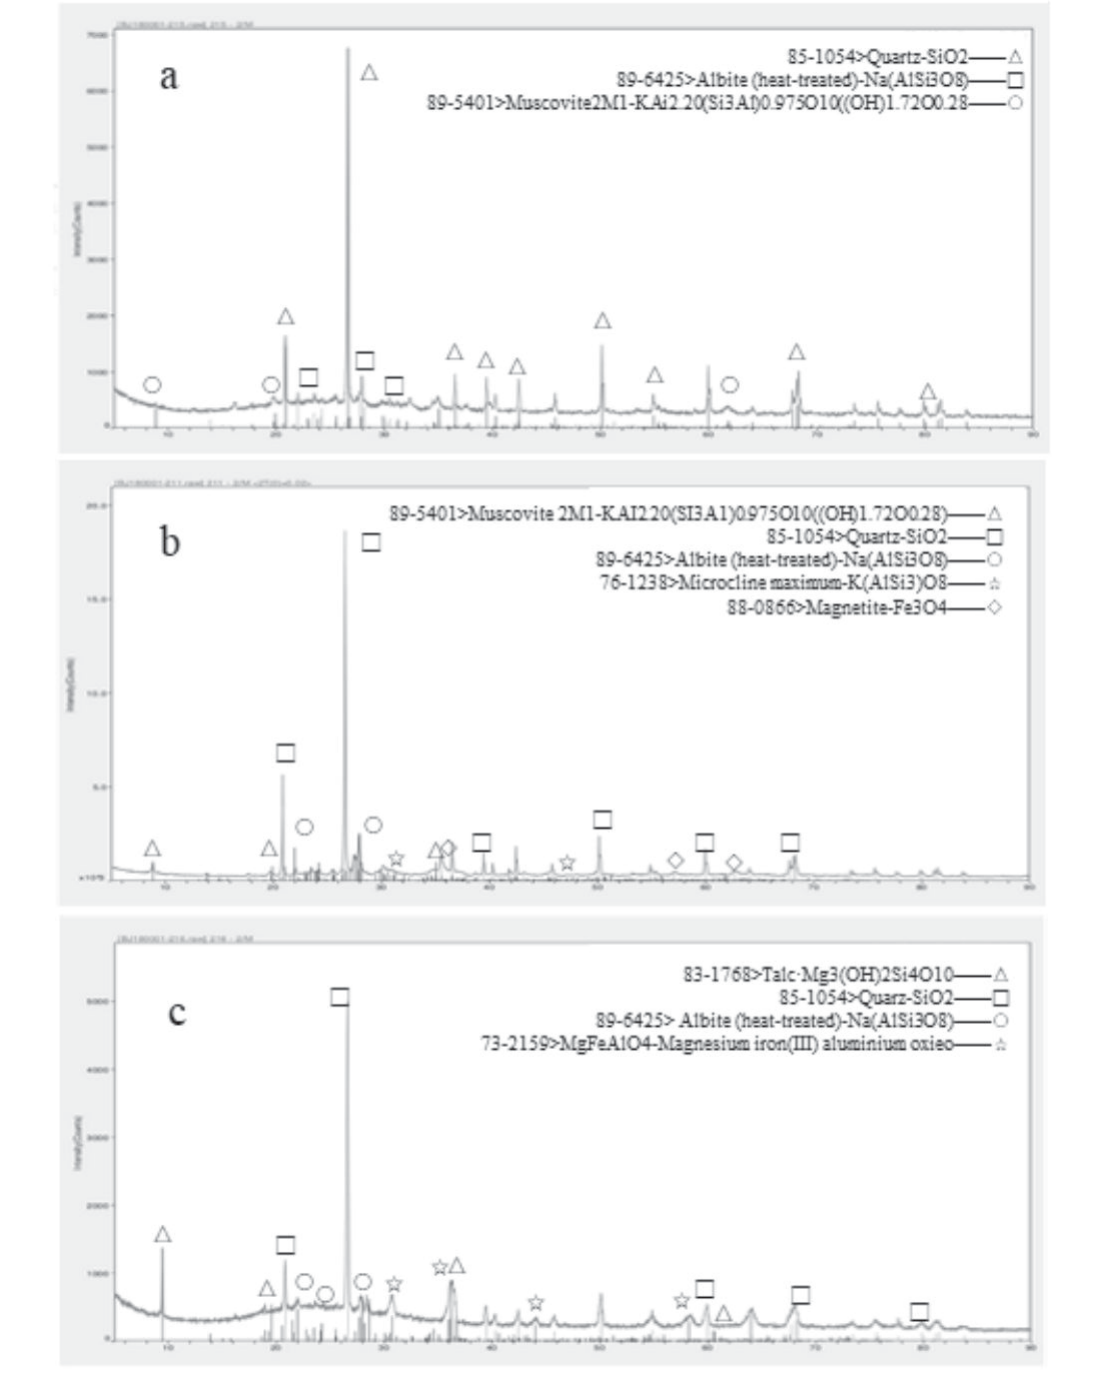
As presented in Fig. 5, the XRD analysis showed that in the process of HM-contaminated soil roasting, the mineral morphology changed. The main mineral forms of the HM-contaminated soil were quartz and dolomite. After calcination at 800ºC, minerals such as kaolinite, muscovite, and magnetite appeared in the solid phase. After roasting at 1100ºC, minerals such as talc and magnesium iron (III) aluminum appeared in the ceramsite. In other words, after high-temperature treatment, more abundant silicate ore crystals appeared in the solid phase, and these crystals also provided a possibility for the HMs to form relatively stable ores (the HM mineral was not detected in the ceramsite, which may be due to the detection limit of the XRD equipment).
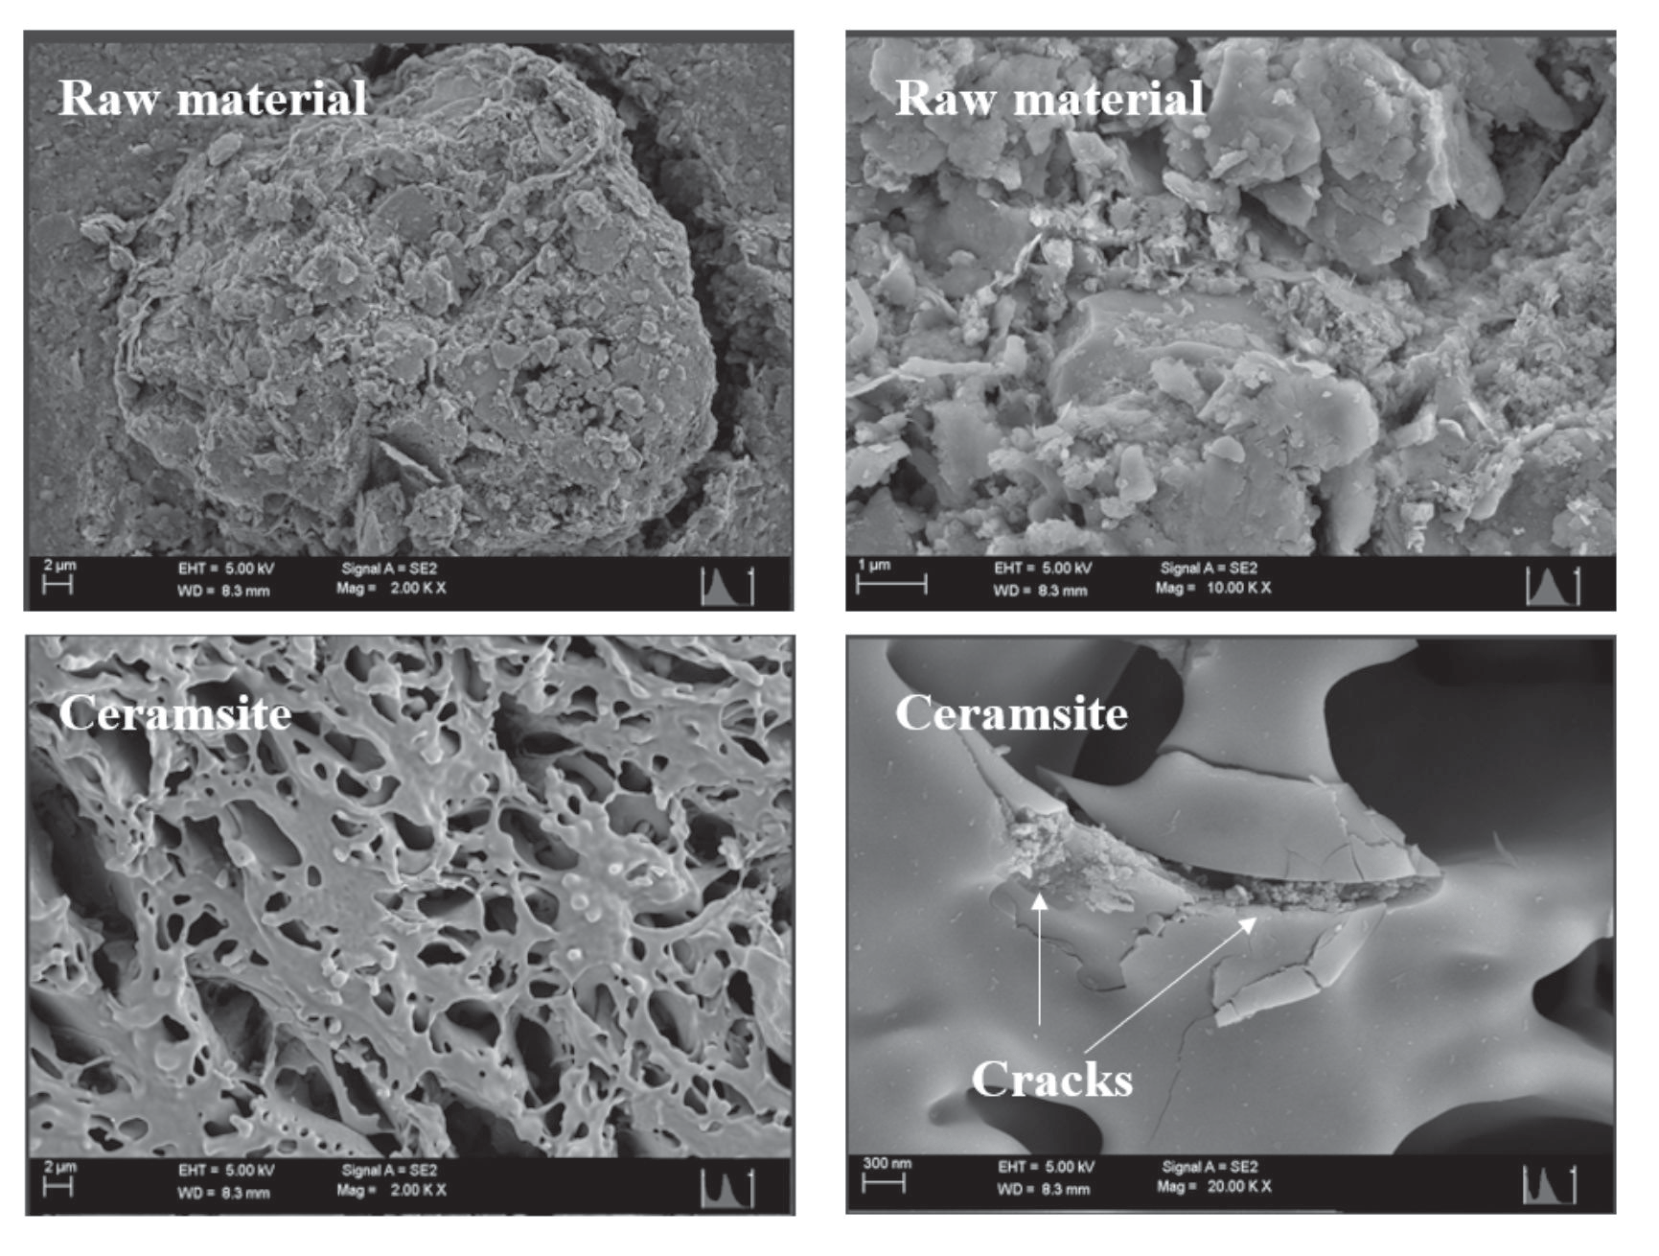
According to the SEM results (shown in Fig. 6), it was easy to find that the microstructure of the raw material changed after roasting. The microstructure of the raw material was composed of many non-compact, tiny particles. To some extent, it was easy for these particles to make contact with the leaching solution. However, the microstructure underwent significant changes after roasting at 1100ºC. The microstructure of ceramsite showed itself to be more smooth and compact compared with the raw material, and parts of the residual particles were fixed in the microstructure. However, some cracks existed in the microstructure, which may be a potential pathway for HM leaching.
Conclusions
In conclusion, the preparation of ceramsite from HM-contaminated soil is an effective way to utilize waste soil. After the HM-contaminated soil was made into ceramsite, the HM concentration changed to some extent. The HM leaching concentration of ceramsite in the SPLP, TCLP, and DTPA tests was much lower compared to soil samples. However, ceramsite prepared from HMs contaminated soil with high concentrations still has certain environmental risks, such as causing an increase in HMs content in the nearby groundwater environment or releasing HMs that are absorbed by plants. Acid rain extraction experiments showed that under adverse conditions (such as ceramsite damage and rainstorms), the release concentration of HMs in the first year was relatively high, and then there was a significant decline. In the ceramsite roasting process, the HM chemical species turned into stable fractions. Additionally, some stable mineral forms were found, and the microscopic surface of the solid phase also became tight after roasting. However, when the soil was seriously contaminated by the HMs, the HMs still leached under certain conditions and even remained in the ceramsite. This result also means that the environmental risks of HMs have not been completely eliminated. In addition, HMs migrate into flue gas during the high-temperature roasting process. This problem should also be considered when this technology is applied to engineering tasks.

