

Introduction
In October 2018, the United Nations Intergovernmental Panel on Climate Change (IPCC) stated that global warming needs to be limited to 1.5°C worldwide to achieve net-zero greenhouse gas (GHG) emissions by the middle of the 21st century [1]. The Carbon Dioxide Emission Report 2022 issued by the International Energy Agency (IEA) indicated that China’s carbon dioxide emissions in 2022 would be 11.48 billion tons, of which 1.2 billion tons were attributed to the total carbon emissions of the automobile industry’s whole life cycle, accounting for approximately 10% of the total emissions [2]. Therefore, the low-carbon green development of the automobile industry has become inevitable.
In 2019, the European Union (EU) mandated regulations concerning carbon emissions from automobiles from a life cycle perspective in order to reduce carbon dioxide emissions from new vehicles [3]. The life cycle refers to the entire process of an object from “cradle to grave”, and the life cycle assessment (LCA) method can systematically and comprehensively analyze products; therefore, it is an effective tool for carbon footprint and environmental impact analyses [4]. Research on automotive LCA has focused on the whole vehicle. Jovanovic [5] evaluated the life cycles of electric and hybrid electric vehicles, but both struggled to offset the massive traffic growth and, therefore, it was suggested to focus on Belgrade’s carbon emissions and the energy consumption of urban transportation from an international perspective. Qiao et al. [6] found that pure electric vehicles (EVs) have 18% lower life cycle carbon emissions than fuel vehicles. Burchart-Korol et al. [7] conducted a life cycle evaluation of local EVs and found that the electricity mix resulted in higher human toxicity and particulate matter than that generated by fuel vehicles during the use phase of the new energy vehicles in the local area. Del Pero et al. [8] applied the LCA method to account for the carbon footprints of internal combustion engines (ICE) and EVs at production, use, and end-of-life stages and showed that the total life cycle carbon footprint of ICE vehicles was higher than that of EVs. Marques et al. [9] found that batteries significantly affected the life cycle environmental impacts of these vehicles when conducting an LCA of new energy vehicles. Wong et al. [10] used a GREET-based LCA process to compare the product carbon footprint of electric and hydrogen-fuel-cell vehicles and showed that the fuel cycle significantly affected the carbon footprint of both vehicles. Shafique et al. [11] comparatively analyzed the life cycle impacts of pure EVs under different electricity scenarios in 10 countries and showed that the use of clean energy contributes to reducing global environmental impacts and mitigating climate change.
An automobile consists of more than 10,000 parts and components, and the production and use of these parts and components have a significant impact on the carbon emission level of the whole vehicle during its entire life cycle. To clearly control the carbon emissions of each link in the whole vehicle, automobile OEMs (original equipment manufacturers) should start from the carbon emissions of automobile part-supplying enterprises and control the carbon emissions of the whole vehicle through supply chain management. Therefore, the LCA of auto parts has become a research hotspot.
Piotrowska et al. [12] used LCA to evaluate the environmental impacts of the whole life cycle of automotive tires, and their results showed that the most energy-consuming stage in their life cycle was the use stage. Poritosh et al. [13] used LCA to assess the environmental impacts and benefits of biocomposites over the life cycle of automotive parts produced from traditional composites and showed that biocomposites have a slightly higher environmental impact per unit mass than conventional composites. Chen et al. [14] investigated the carbon footprint of lithium-ion batteries produced in China using a cradle-to-cradle LCA methodology and reported carbon emissions of 91.21 kg CO2 eq/kWh, with cathode production and battery assembly processes being the primary sources. Shah and Kaka [15] conducted a carbon footprint study of batteries for EVs and evaluated the carbon footprint of lithium-ion batteries throughout the life cycle and showed that lithium-ion batteries have the largest carbon emissions at the raw material preparation stage. Fan et al. [16] used lithium–iron phosphate (LFP) batteries and lithium–nickel–cobalt–manganese acid ternary batteries, which are commonly used in EVs, as a research object. The environmental impacts of their full life cycle were compared, and the results showed that the environmental performance of lithium–iron phosphate batteries was superior.
Sensitivity analyses are often used to interpret the results of LCA methodologies and identify the key factors or parameters that most affect the results, thereby aiding the optimization of these factors. Scholars in various countries have conducted numerous studies on sensitivity analysis. Yi and Bauer [17] conducted a detailed deterministic and stochastic sensitivity analysis on the propulsion energy cost of EVs with respect to environmental variables; their results showed that the sensitivity of energy consumption relative to the four environmental variables varied greatly with the operating conditions of the vehicle. Bargal et al. [18] proposed a sensitivity analysis of theoretical parameters of the automotive radiator based on the validity-NTU method; theoretical parameter sensitivity analysis showed that radiator efficiency is significantly related to the water Reynolds number and inlet water temperature, but not to the air Reynolds number and inlet air temperature. These environmental effects can have a profound impact on the overall energy consumption of an EV and greatly affect the driving range. Jamroen et al. [19] utilized variance-based global sensitivity analysis mainly for identifying the parameters affecting the uncertainty while charging an EV; their results showed that the number of participating EVs has the greatest impact on the frequency stabilization capability, followed by the rated charging power of the EV. Braband et al. [20] used global variance-based sensitivity analysis to investigate how uncertain (system or controller) parameters in a vehicle affect energy efficiency, ultimately concluding that variations in vehicle mass, battery temperature, rolling resistance, and auxiliary consumers have the greatest impact on energy consumption.
In summary, to meet national requirements and emission standards on carbon neutrality and achieve green development, automobile enterprises must collaborate to reduce carbon emissions in the entire supply chain. To date, research on sensitivity analysis has only considered a single factor; however, changes in multiple factors can be correlated, and changes in one factor are often accompanied by changes in other factors. Therefore, single-factor sensitivity analysis is limited. This study examined the full range of auto parts enterprises, divided the life cycle of parts into phases, constructed the carbon footprint accounting model of each phase, and accounted for the carbon emission of auto parts in each phase using this model. Furthermore, a two-factor sensitivity analysis was performed to analyze the total mass of the parts and types of materials, as well as the mass ratio of the constituent parts, as the two factors of change.
Materials and Methods
Carbon Footprint Accounting Modeling
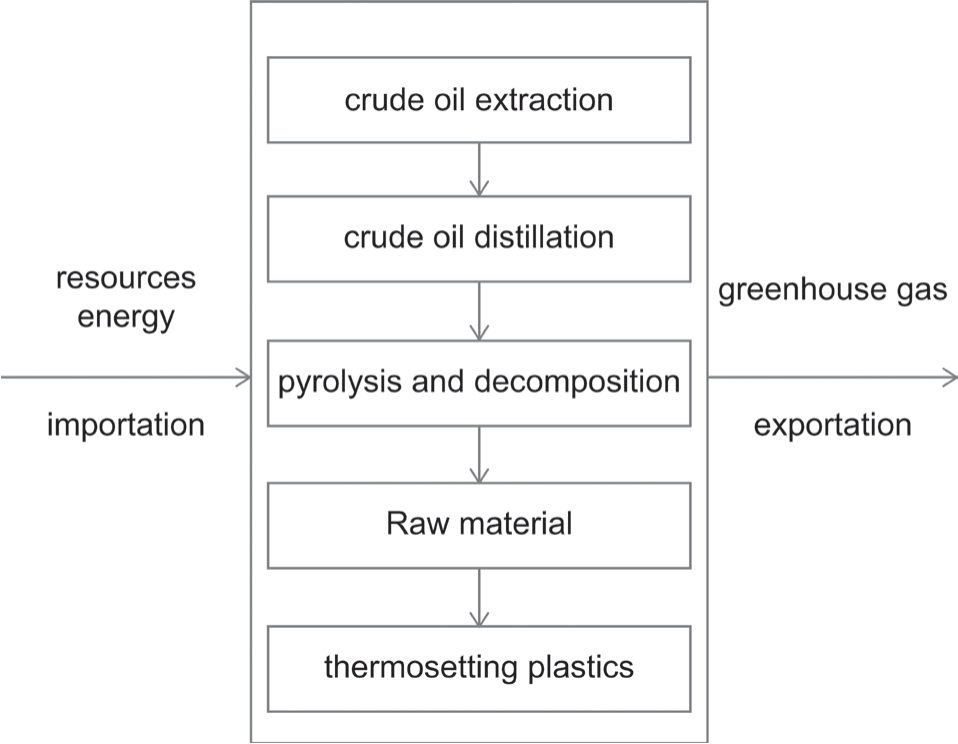
The carbon footprint is the pool of GHGs emitted during social activities. The carbon emission factor refers to the generation of GHGs accompanying the consumption of a unit mass of a substance and is an important parameter characterizing the GHG emissions of a substance. The manufacture of a product will have resources and energy as inputs, and after a series of processes, form the final product and emit GHGs. However, in the actual production process, many materials are provided by upstream enterprises; although there are many upstream enterprises and the carbon emission factor of this part of the materials cannot be calculated individually, these can be queried in the GaBi database (https://www.gabi-software.com/). The production process for thermosetting plastics is illustrated in Fig. 1. The carbon emission factor of energy and resources consumed in this process can be obtained from the GaBi data, and the final GHG can be calculated.
To fully assess the life cycle carbon footprint of automobile parts, the carbon emissions in the raw material preparation, parts production and manufacturing, usage and maintenance, and end-of-life recycling stages must be considered. The accounting methodology was based on the carbon emission factor methodology provided by the IPCC, as shown in Equation (1):
where Ci is the carbon emission, ADi is the quantity of physical activity level, and CEFi is the carbon emission factor.
Raw Material Preparation Phase
Two sources of carbon emissions exist in the raw material preparation phase: carbon emissions generated by energy consumption during resource extraction and processing and those generated by transportation to the component manufacturing enterprises after preparation as raw materials.
Carbon Emissions from Raw Material Preparation
First, we established the raw material quality matrix M part for automobile parts, assuming that n parts and t materials are needed to produce an automobile part, and expressed the mass of each material used for each part as follows:
(2)
where n is the number of part types, t is the total number of material types required to produce automobile parts, and mpart,nt is the mass of the t-th material in the n-th part.
The raw material carbon emission factor matrix CEFm was established and the expression of its transpose matrix is presented in Equation (3):
where CEFm,t is the carbon emission factor of material t.
The calculation formula for carbon emissions in the raw material preparation stage is presented in Equation (4):
Carbon Emissions from the Transportation of Raw Materials
First, the energy consumption matrix Etrspt in the transportation process was established. Modes of transportation include land, water, air, and "other," which require different types of vehicles that require different types of energy sources. Therefore, the energy consumption matrix Etrspt in the transportation process was established as presented in Equation (5):
where r is the type of energy used in transportation and er is the amount of energy r consumed per mile during transportation under full load conditions.
The carbon emission factor matrix CEFe of the energy used by the transport vehicle was established. The expression of its transpose matrix is presented in Equation (6):
where cefe,r is the carbon emission factor of r-type energy.
In the transportation process, energy is consumed and exhaust gas is produced, contributing to the carbon footprint. The mass matrix Mw of exhaust gas emission per unit mileage of vehicle was established, as presented in Equation (7):
where f is the type of exhaust emission and mw,f is the mass or volume of the f-type exhaust emission.
The carbon emission factor matrix CEFw of the transport vehicle exhaust substances was established, and its transpose matrix expression is presented in Equation (8):
where cefw,f is the carbon emission factor for tailpipe emissions of type f.
The carbon emissions of raw material transportation were accounted for using Equation (9):
where Ctrspt is the carbon emissions from raw material preparation to production and manufacturing, and L1 is the transportation distance from raw material preparation enterprises to production and manufacturing enterprises.
The carbon footprint accounting formula for the raw material preparation stage is presented in Equation (10):
Production and Manufacturing Phase
Carbon emissions during the manufacturing process mainly come from the energy consumption of the equipment used. During processing, carbon emissions result from the consumption of auxiliary materials and the energy consumption of mechanical equipment in the assembly process. In the transportation process, carbon emissions result from the energy consumption of vehicles and exhaust emissions.
Carbon Emissions from Energy Consumption During Processing and Manufacturing
First, we established the energy consumption matrix, EMF, for each process involved in parts processing. The matrix represents the energy consumption associated with processing a single product, as presented in Equation (11):
(11)
where g is the total number of processes involved in the manufacturing of automobile parts and Ee,ng is the amount of energy for the g-th part of the n-th part.
The carbon emission factor CEFmf,e was established for each process in the manufacturing stage of automobile parts, and the transposed matrix expression is presented in Equation (12):
where cefe,g is the carbon emission factor for energy consumption in category g processes.
The carbon emissions Cmf,e from the manufacturing stage due to process energy consumption were calculated using Equation (13):
Carbon Emissions from the Consumption of Auxiliary Materials
We established the quality matrix Ma of auxiliary materials used in each process during the production and manufacturing of automobile parts using Equation (14):
(14)
where ma,ng is the mass of auxiliary materials added in the g-th process of the n-th part.
The carbon emission factor matrix CEFma for auxiliary materials was established, and its transposed matrix expression is presented in Equation (15):
where cefma,g is the carbon emission factor of auxiliary materials consumed in category g processes.
The carbon emission accounting formula for the consumption of auxiliary materials in the manufacturing process of auto parts is presented in Equation (16):
Carbon Emissions from Energy Consumption in the Assembly Process
We constructed the assembly process energy consumption matrix Eassemble using Equation (17):
where eab,r is the amount of r-type energy consumed in the assembly process.
The carbon emission factor matrix CEFea of energy consumption in the assembly process was established, and its transposed matrix expression is presented in Equation (18):
The calculation formula for carbon emissions generated by energy consumption in the assembly process is presented in Equation (19):
The carbon footprint calculation formula of the auto parts production and manufacturing process is presented in Equation (20):
Usage and Maintenance Phase
Carbon emissions in the usage phase of auto parts originate from two sources: carbon emissions generated by energy consumption during normal use and those generated from product maintenance and material consumption due to collision and extrusion during use.
Carbon Emissions from Energy Consumption During Vehicle Use
Cars may use different energy sources; thus, we assumed that “r” types of energy are consumed by cars in the running process. First, the energy consumption matrix Euse of the vehicle use stage was established using Equation (21):
where r is the type of energy consumed during the use of the car and euse,r is the amount of energy r consumed per mile of a vehicle during normal use under full load conditions.
The energy carbon emission factor matrix CEFuse,e of energy at the use stage was established, and the expression of its transpose matrix is presented in Equation (22):
where CEFe,r is the carbon emission factor of r-type energy.
The carbon emission formula accounting for the vehicle in the service stage is presented in Equation (23):
where L2 is the vehicle life cycle mileage.
The calculation formula of carbon emissions of auto parts in the vehicle life cycle mileage was established. Based on the mass ratio method, the energy consumption ratio of the automobile bumper in the use stage was calculated. The mass ratio expression is presented in Equation (24):
The mileage of auto parts is less than that of the entire vehicle. Therefore, the mileage of auto parts includes a part of the mileage of the life cycle of the entire vehicle. Assuming that the number of bumper changes in the life cycle of the car is X times, the mileage of a part is calculated using Equation (25):
The calculation formula for carbon emissions generated by energy consumption in the usage stage of automotive parts is presented in Equation (26):
In addition to energy consumption, cars produce exhaust emissions during the driving phase, contributing to the carbon footprint. The Muse,w mass matrix of exhaust gas emitted by vehicles in the usage stage was established, and w is presented in Equation (27):
where f is the type of exhaust emissions and mw,f is the mass or volume of the f-type exhaust emission.
The carbon emission factor matrix CEFuse,w,m was established, and the expression of its transpose matrix is presented in Equation (28):
where cefw,mf is the carbon emission factor per unit mass of the f tail gas.
The calculation formula for carbon emissions generated by exhaust emissions of automobile parts during driving is presented in Equation (29):
Carbon Emissions from the Maintenance Phase
Automobile parts are not completely obsolete following accidents and can be returned to service after repair. The repair process may involve the consumption of raw materials or auxiliary materials and energy. The carbon emissions from maintenance during the usage phase were calculated using Equation (30):
The carbon footprint accounting formula for the use phase of automobile parts is presented in Equation (31):
End-of-Life Recycling Phase
The carbon emissions of auto parts at the end-of-life recycling phase comprise three parts: carbon emissions generated by the energy consumption of the recycling process, positive environmental benefits generated by the partial material recovery and material regeneration distribution, which are negative carbon emissions, and carbon emissions generated by the energy consumption and exhaust emissions of vehicles at the end-of-life point.
Carbon Emissions from Energy Consumption During Recycling
The energy consumption matrix ERY of the recycling process in the recycling phase is presented in Equation (32):
(32)
where y is the total number of processes required in the end-of-life recycling process of auto parts and Ee,ny is the amount of energy consumed by the y-th recycling process of the n-th part.
The energy carbon emission factor matrix, CEFRY,e, was established for the energy consumed by each process in the end-of-life recycling phase of automobile parts. The transpose matrix expression is presented in Equation (33):
where cefe,y is the energy carbon emission factor for energy consumption of process category y.
The carbon emission accounting formula for the end-of-life recycling phase due to the energy consumption of the recycling process is presented in Equation (34):
Negative Carbon Emissions from Material Recycling
We established the recovery stage of all types of material recovery matrixμRY, and its expression is presented in Equation (35):
where μre, tt is the recycling rate of the t-th material.
The positive environmental benefits of material recycling and the calculation formula for negative carbon emissions are presented in Equation (36):
Carbon Emissions from Transportation of Scrap Recovery Bumpers
The carbon emissions in the transportation process are consistent with the carbon emission algorithm generated in the transportation process of the raw material preparation phase. Therefore, the description was repeated for this phase; the transportation distance was L4. The calculation formula for scrap carbon emissions is presented in Equation (37):
Therefore, carbon emissions in the recovery phase are the sum of the carbon emissions of the three processes because the recycling of materials has positive benefits for the environment and negative carbon emissions. The carbon emission formula accounting for the scrap recovery phase of auto parts is presented in Equation (38):
The recycled material will become the raw material of the next product, thereby reducing the use of new raw materials. Therefore, a part of the carbon emissions generated during the recycling phase should be allocated to the next product life cycle system. The allocation of material recycling efficiency should be determined based on the Product Environmental Footprint Standards, combining enterprise reality, and establishing the appropriate η distribution coefficient. The calculation formula for carbon emissions in the scrap recovery stage is presented in Equation (39):
Results and Discussion
Carbon Footprint Accounting for Car Bumpers: A Case Study
In this study, an S201XXX bumper produced by PW Enterprise in Chongqing, China, was selected as the research object, including the front and rear bumpers of this model. The specific model and main functional parameters of the bumper are listed in Table 1.
The bumper comprises 30 parts with a total mass of 19 kg. Of these parts, 14 are locally made, accounting for approximately 98% (18.51 kg) of the total mass. The other 16 parts, mostly small parts such as connecting bolts and decorative strips, with a total mass of 0.49 kg, are purchased. Owing to their relatively small mass and volume, the purchased parts were not considered in this study. Therefore, this study focused on the 14 locally made parts of the bumper; the specific components and names are presented in Table A.1.
Scope and Assumptions of LCA
The scope of this bumper study is consistent with the scope defined by the carbon footprint accounting model for automobile components. Based on this scope, the following assumptions were made:
(1) Outsourced parts were not included in the analysis owing to their small mass and percentage.
Table 1.
Bumper-related parameters of S201XXX.
| Name | Product number | Quality (kg) | Specification (mm) |
|---|---|---|---|
| S201XXX front bumper | 2804100-XW13 | 9.06 | 1815 × 567 × 687 |
| S201XXX rear bumper | 2803100-XW14 | 9.94 | 1814 × 569 × 614 |
(2) Internal logistics and transportation within the parts manufacturing workshop and manual handling were not considered.
(3) During the use phase, if the bumper is involved in an accident, it is more likely to be replaced rather than repaired. Therefore, the focus of the use and maintenance phase was on bumper replacement, ignoring repair scenarios.
(4) Regarding logistics and transportation, only long-distance transportation exceeding 5 km was considered.
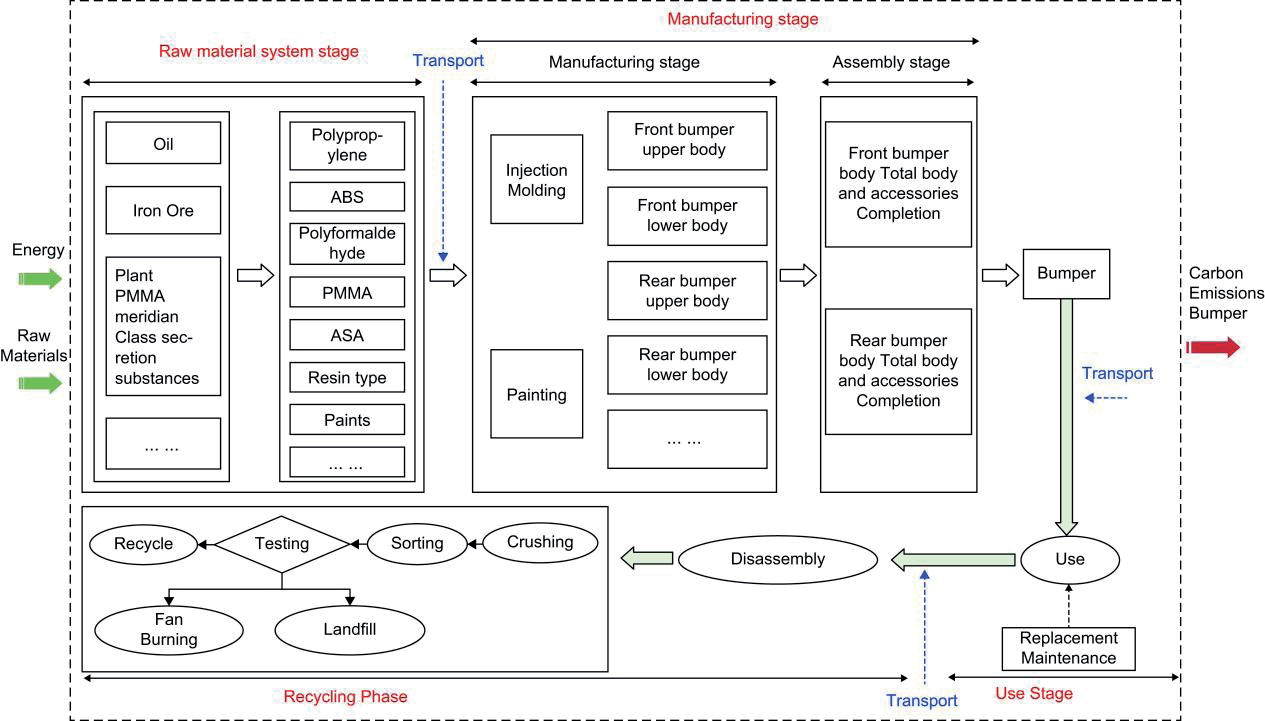
The schematic diagram depicting the boundary of the car bumper system determined based on the scope and assumptions of the study is presented in Fig. 2.
Inventory Analysis
The data collected for this study were obtained from three primary sources: field research on Chinese automobile bumper manufacturing enterprises based on the manufacturing process; background data from the educational version of the GaBi database; open literature or queried national industry statistics. The data collected from these three sources were combined to create a data inventory for the life cycle carbon footprint evaluation of bumpers.
Raw Material Preparation Phase
The production information, including the weight and material composition of each bumper part, is presented in Table A.2. Loss of raw materials occurs during the manufacturing process of each part (a rate of 3% in the study enterprise). After the raw materials are prepared, they are transported to the automobile manufacturer by road using a Liuzhou Zhanlong vehicle, which has a full load weight and fuel consumption of 15,000 kg and 18 L/100 km, respectively. The distance between the raw material preparation plant and the product manufacturing plant is 64 km.
During transportation, the vehicle emits four pollutant gases that contribute to the carbon footprint. The emission standards for each gas are outlined in Table 2.
To account for the carbon emissions of raw materials, the corresponding material carbon emission factors and their quantities must be obtained. In this study, the following carbon emission factor values were obtained from the GaBi database: factor values of various materials produced in the China region, various energy sources, and tailpipe emissions.
Table 2.
Environmental emissions per kilometer from transport vehicles.
| Environmental emissions | Emissions (mg/km) |
|---|---|
| CO | 100 |
| NMHC | 68 |
| NOX | 60 |
| PM | 4.5 |
Table 3.
The manufacturing process of the front bumper upper grille penetration trim body.
Production and Manufacturing Phase
The manufacturing process of the unsprayed parts, represented by the upper grille of the front bumper through the body of the trim, is presented in Table 3, and the manufacturing process of the sprayed parts, represented by the upper body of the front bumper, is presented in Table 4.
The energy consumption data were obtained from a field survey of the factory. The consumption of electrical energy and natural gas of the automobile bumper components in the manufacturing stage is presented in Table A.3.
The auxiliary materials added in the production and manufacturing stages were primarily used for painting the automobile bumper body. Two main body parts required spraying: the front and rear bumpers. The details of the added auxiliary materials and their corresponding carbon emission factors are presented in Table 5.
The carbon emission factors for natural gas were obtained from the GaBi database. Electricity is a secondary energy source, and the CO2 emissions from electricity are mainly due to the consumption of fossil fuels during its production. The bumper manufacturer, located in Chongqing, China, uses the central China regional power grid; thus, only the carbon emission factors for this grid were included.
Table 4.
The manufacturing process of the upper body of the front bumper.
Table 5.
Consumption and carbon emission factors of body accessories on front and rear bumpers.
In accordance with the Approved Methodology for Grid Integration of Renewable Energy Generation (ACM0002), the electricity and capacity marginal emission factors were multiplied by the weighting factors ω1 and ω2, respectively, to obtain the electricity carbon emission factor, where ω1 and ω2 = 1. The specific formula is presented in Equation (40):
where the weight of the electricity and capacity marginal emission factors, OM and BM, are adjusted to 0.25 and 0.75, respectively, for all power projects (such as thermal, hydro, and waste-to-energy power), except for photovoltaic and wind power projects where OM and BM are fixed at 0.75 and 0.25 based on the Chinese regulations, respectively.
The carbon emission factor of the central China regional power grid was determined to be 0.4287 tCO2/MWh based on Equation (40) and statistical data obtained from the China Electricity Yearbook, China Energy Statistical Yearbook, Statistical System of Energy Consumption in Public Institutions, and Compilation of Statistics on Electric Power Industry.
The manufacturing stage includes the assembly process in addition to mechanical processing. The upper and lower bodies of the front and rear bumpers require electric equipment for bolting, whereas the remaining components can be assembled manually, such as buckling and connecting. The electricity consumed by this process is presented in Table 6.
Usage and Maintenance Phase
An M1 gasoline car with this bumper has a mass of 1,400 kg, the average mileage of 600,000 km, fuel consumption of 6.64 L/100 km, and various amounts of exhaust emissions per km (Table 7). The mass of the bumper is 19 kg, and the average number of bumper replacements for this model is one, equivalent to using two sets of bumper units during the car life cycle. Thus, the average mileage of a single set of bumpers is 300,000 km. The fine-tuning process of the bumper shape is mostly manual, and the amount of paint consumed to fill it is minimal; thus, the carbon emissions from the maintenance process were not considered in this study.
Table 6.
Power consumption during the assembly stage.
| Category | Electricity consumption (kW·h) |
|---|---|
| Front bumper on the body | 0.36 |
| Rear bumper on the body | 0.38 |
| Front bumper lower body | 0.23 |
| Rear bumper lower body | 0.25 |
Table 7.
Environmental emissions per kilometer from vehicles.
| Environmental emissions | Emissions (mg/km) |
|---|---|
| PN | 61,011 pcs |
| CO | 700 |
| PM | 4.5 |
| NMHC | 68 |
| NOX | 60 |
Table 8.
Energy consumption of equipment in the scrap recovery stage.
End-of-Life Recycling Phase
The material recycling process is an environmentally beneficial practice that contributes to the sustainable development of social and environmental resources. This process involves crushing, cleaning, laminating, and screening to separate recyclable from non-recyclable materials. Crushers, cleaning equipment, laminators, paint removal equipment, and sorting equipment are used. These machines require electrical energy to operate; their electricity consumption is presented in Table 8. For automobile bumper parts that cannot be reused, some reusable materials are extracted via the recycling process of crushing, rolling, and paint removal. The average recovery rate of plastic parts, such as polypropylene, polymethyl ester, vinyl acrylic acid, and other non-metallic materials is 50%.
The recycling of this product belongs to open-loop recycling, and according to the relevant recycling allocation method of the “Environmental Footprint of European Union Products” and taking into account the actual situation of this product, the allocation principle has been determined as follows: the car bumper bears 70% of the carbon emissions in the recycling stage, and products using recycled and reclaimed materials bear 30%.
Carbon Footprint Accounting and Sensitivity Analysis
Carbon Footprint Accounting
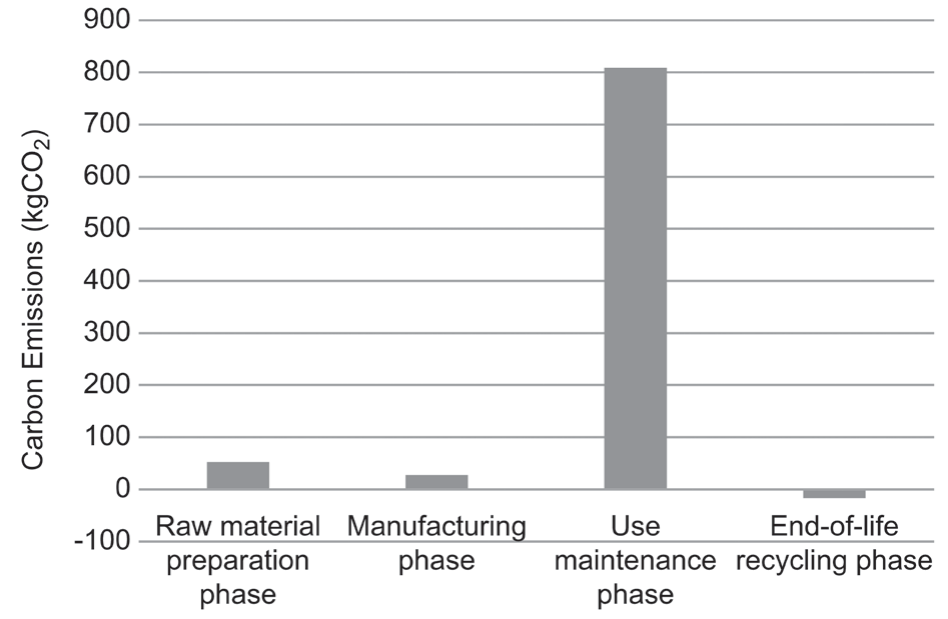
Based on the inventory and background data provided by the GaBi database, we calculated the carbon emissions of car bumpers throughout their life cycle. The results of the bumper's carbon emissions at each stage of its life cycle are shown in Fig. 3.
The total carbon emission of the whole life cycle of the bumper was 872.13 kg CO2, of which 52.37 kg CO2 was emitted in the raw material preparation stage, 27.67 kg CO2 in the manufacturing stage, 808.8 kg CO2 in the use and maintenance stage, and −16.69 kg CO2 in the end-of-life recycling stage. The emission was a negative value because after the bumper was scrapped, the consumption of new resources was reduced by recycling renewable materials, which was a positive benefit to the environment.
Sensitivity Analysis
Sensitivity analysis measures the degree of change in outcome indicators due to changes in certain factors by identifying one or more factors with a greater impact on the results. In this study, a two-factor sensitivity analysis was conducted.
Two-factor sensitivity analysis selects two factors as independent variables and analyzes their impact on the output results. In this study, the total mass of the product and the proportion of certain materials were used as the factors of change. Increasing or decreasing the proportion of certain materials in the original product will alter the proportion of the remaining material accordingly to achieve equilibrium.
The model function is shown in Equation (41) as follows:
where the value range of x is x ∈ (c1,c2) y = (−b,b) p ≥ 2; x is the total product mass; c1,c2 are the upper and lower limits of the total product mass, respectively; y is the material proportion; b is the material proportion change in ratio range value; as is the share of the s-th material in the original mass s = (1,2,3,···,t); and CEFms is the carbon emission factor of the s-th material s = (1,2,3,···,t).
Sensitivity analysis was performed on the total mass of the car bumper and the proportion of each material based on the established model. The quantity of various raw materials in this bumper can be increased or decreased by 10% under the existing conditions without affecting the product structure and usage performance and can ensure normal usage. The materials that comprise automotive bumpers were classified into five categories—polypropylene (PP), polyoxymethylene (POM), polymethylmethacrylate (PMMA), engineering plastics (ASA), and modified resins (ABS)—and were analyzed by adding or subtracting 10% to the existing mass of each type of material.
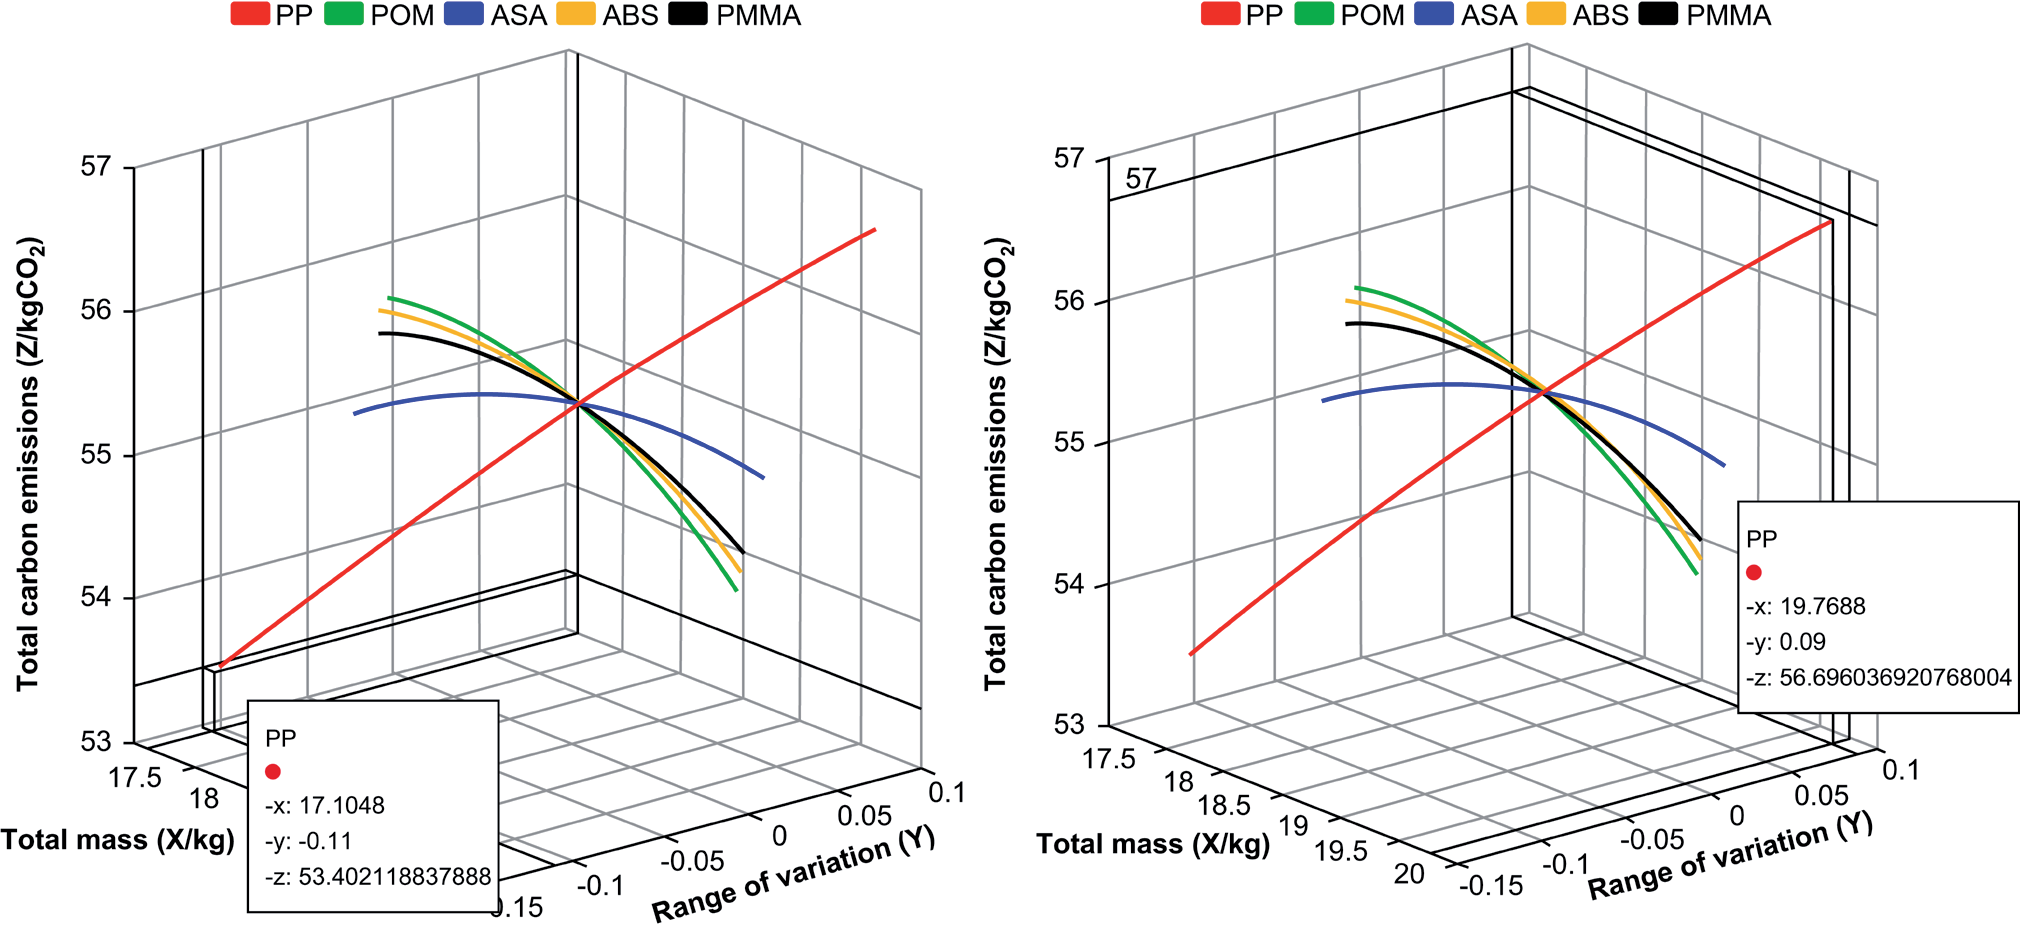
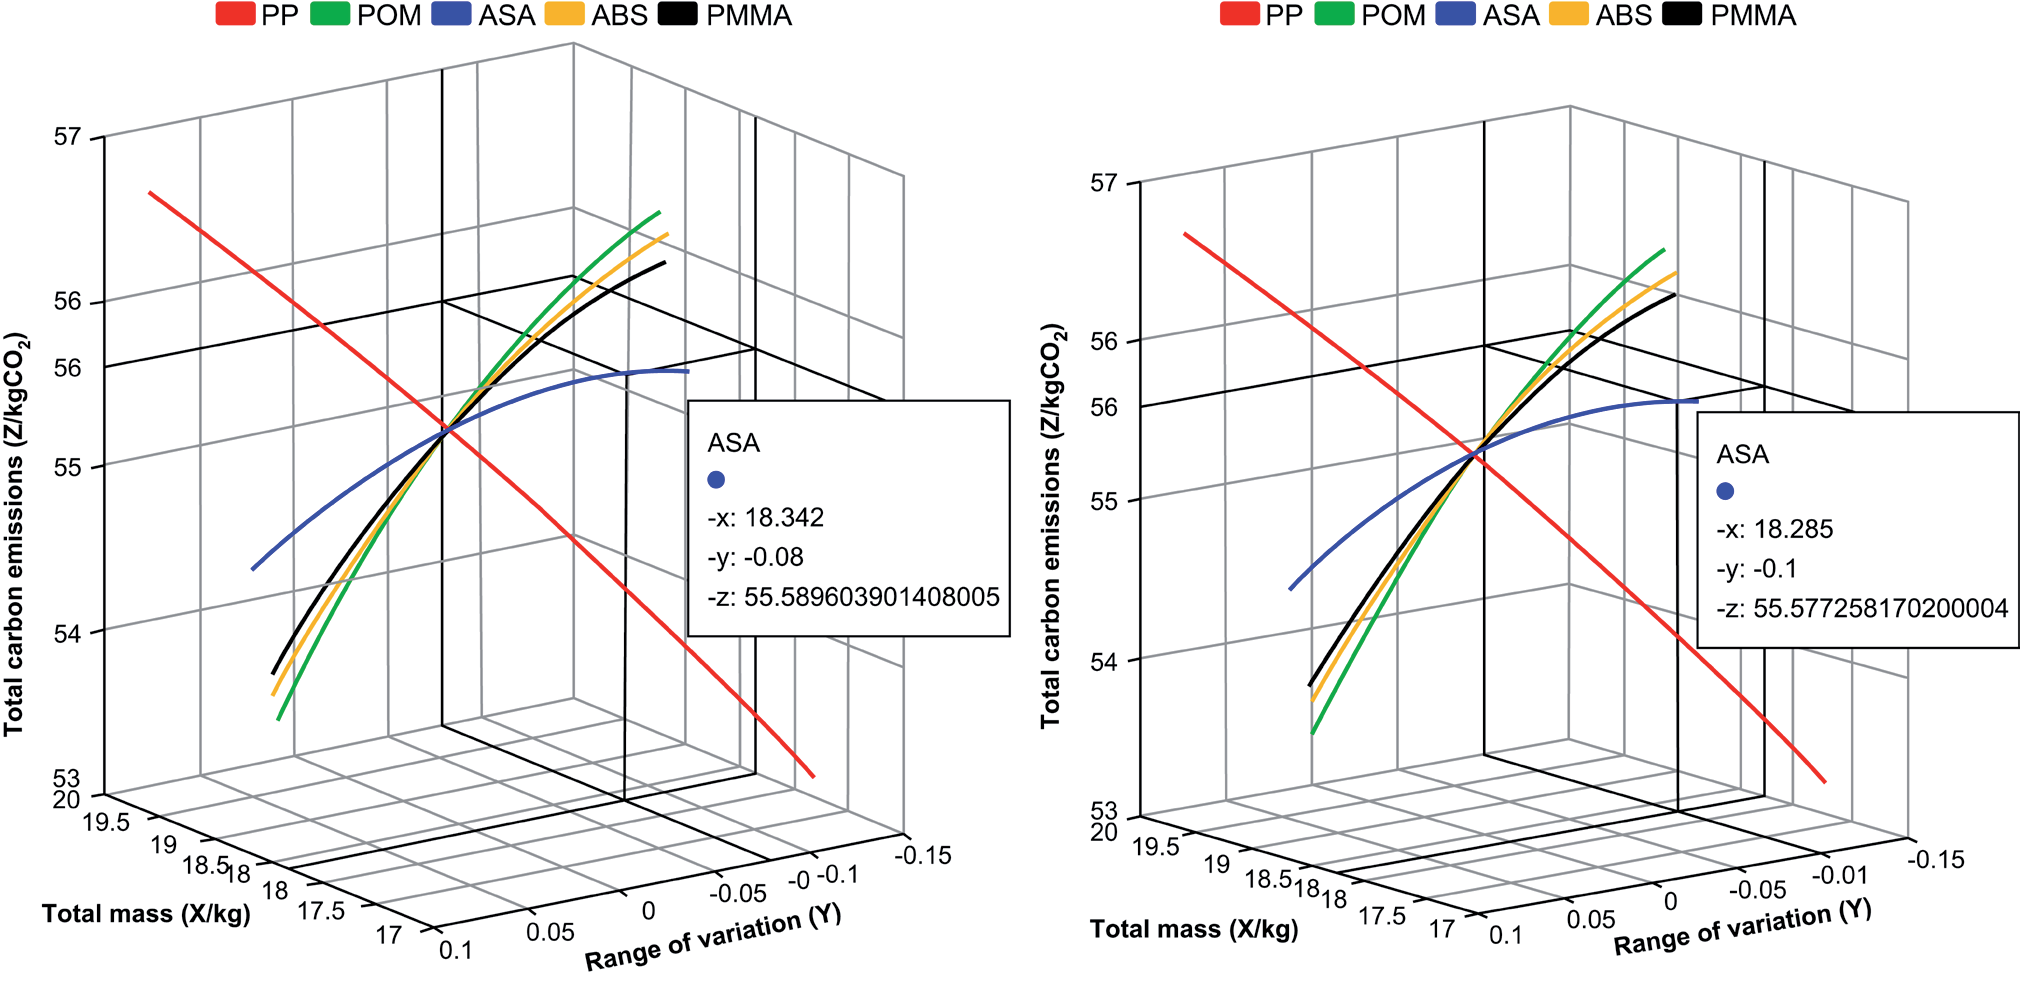
Combining the functional model equation (41) and the relevant data of each material, the varying mass of each of the five materials was calculated. As shown in Fig. 4, the X-axis indicates the range of the total mass change of the bumper, the Y-axis represents the mass share of material, and the Z-axis represents the total carbon emissions of all raw materials. The red line shows the range of changes in carbon emissions for all raw materials with a 10% increase or decrease in the current mass of the PP material. Similarly, the green line corresponds to POM, the blue line to ASA, the yellow line to ABS, and the black line to PMMA.
Polypropylene was the material with the greatest impact on the total carbon emissions of raw materials. Polyoxymethylene, ABS, and PMMA tended to show decreases in the total carbon emissions as their mass increased. The overall trend of ASA was also to decrease its total carbon emissions as the mass share increased; however, the total carbon emissions of raw materials for bumpers were the highest when the mass of ASA was reduced by 8% of its current mass, after which it decreased again (Fig. 5).
The model was feasible for the selection of green raw materials. While ensuring product performance, it enables the determination of the total quality of the material and the selection of proportion of each material for products consisting of multiple materials, thereby optimizing the carbon emissions from the raw materials of the product.
Conclusions
Combined with actual production, this study constructed a carbon footprint accounting model for automotive parts based on life cycle evaluation, quantitatively evaluating the carbon footprint of automotive parts during their life cycle based on the processing and manufacturing sequence of the parts, as well as the material and energy consumption throughout. Considering the S201XXX model bumper produced by the Chinese company PW Enterprise, we determined the life cycle system boundary of the bumper, designed the inventory data collection form, conducted inventory data collection, combined the carbon footprint evaluation model of the automobile bumper with the inventory data, and completed the accounting of the carbon footprint of the bumper life cycle. The results showed that the carbon emission of the life cycle of the S201XXX model bumper was 872.13 kg CO2, and the order of life cycle carbon emission was 808.8 kg CO2 in the use and maintenance phases, 52.37 kg CO2 in the raw material preparation phase, 27.67 kg CO2 in the manufacturing phase, and −16.69 kg CO2 in the end-of-life recycling phase. We conducted two-factor sensitivity analysis with the total mass of the product and the proportion of material as the factors of change and found that the mass proportion of ASA was the same as the proportion of the material. Furthermore, the highest total carbon emissions from the raw materials of the bumper were achieved when the mass percentage of ASA was reduced by 8% from the current level.
The auto parts accounting model helps enterprises mitigate carbon emissions at various stages, identify the main carbon emission links, and formulate targeted carbon reduction measures. The proposed two-factor sensitivity analysis can provide a scientific basis for the selection of product material types and determination of quality ratio.

