

Introduction
In recent years, sustainable development and conservation of natural resources have become global issues. Cement is one of the oldest building materials [1]. From 2005 to 2050, global cement production is projected to increase by a factor of 2.5, and most of this growth will be in developing countries. Cement production consumes large quantities of limestone, clay, sand and iron slag. Typically, 1.7 tons of mineral raw materials are required to produce 1 ton of cement clinker [2]. Anhydrous Portland cement is a mixture of clinker and gypsum. Clinker is a heterogeneous material consisting of at least four phases. The two major phases are tricalcium silicate Ca3SiO5 (C3S) and dicalcium silicate Ca2SiO4 (C2S). Most calcium silicate phases are not pure: they exist in solid solution, with the C3S and C2S basal phases known as alite and belite, respectively [3]. Both types of calcium silicate are capable of producing hydrates, which play a role in the mechanical properties of hydrated cement. C3S reacts faster with water than C2S and is mainly involved in short-term strength. Alite is another main hydraulic phase of cement and is important for subsequent strength development [4]. The use of raw materials (rich in Ca3P2O8) as alternative fuels in cement plants usually raises the question of the effect of phosphorus on C3S. The main effect of phosphorus addition is to reduce the alite/belite ratio and severely affect the strength and properties of hydrated cement [3, 5]. Various forms of phosphorus (P) have different definite effects on the reactivity of the synthesized raw meal and the texture of the corresponding clinker. Under oxidizing conditions, P is highly soluble in the C2S phase in the form of P5+ ions, decreasing the alite content. Under reducing conditions, the major portion of P is reduced to P3+. PO43- ions decrease the viscosity of the liquid phase. The addition of P into the cement raw meal and its effect on the clinker formation and cement properties have been broadly discussed over the past few years. For every 1 wt% of P2O5 added above the limit, the concentration of alite decreases by 9.9 wt%, while the concentration of belite increases by 10.9 wt%. Above 2.25 wt. % P2O5, the clinker is no more acceptable for cement production [6]. Few studies have dealt with the effect of small amounts of added phosphorus (by weight).
On the other hand, the potential threat of sludge has also caught the Chinese government’s attention. Phosphorus is a substance with a high content in municipal sewage sludge (MSS). Removal and recovery of phosphorus from MSS is very costly and complicated [7, 8]. In recent years, the phosphorus contents have continued to rise in MSS. Sustainable disposal of MSS has an important goal which is to recycle resources without a supply of harmful substances to humans or the environment [9, 10]. Nowadays, landfill is still an important way of being used for sludge disposal in China. Incineration presents a good choice because the volume of the end product (ash) is only about 30% of the initial solids content of MSS [11]. Unfortunately, the drawbacks of incineration include the expensive incinerator and the generation of residual inorganic ash. Therefore, there is a better way through the co-combustion of sludge in cement-producing kilns [12]. This not only replaces the cement raw meal, but it also saves phosphate rock which helps in the burning of clinker for cement production. Therefore, the technology is a cost-effective solution for sludge treatment and contributes to sustainable phosphorus recycling. Sludge as an alternative fuel and raw material in cement production has been widely reported [11, 13, 14]. The feasibility of the replacement of raw material for cement production with heavy metal-containing sludge was investigated. As the replacement of raw mix by sludge was within 15%, the formation of the C3S phase in cement would be enhanced by the introduction of heavy metals. Dried sewage sludge as an additive could have an effect on cement property in the process of clinker burning [15, 16]. It is found that sewage sludge has no negative effects on the consumption of free lime and the formation of clinker minerals [15, 17]. However, few studies focused on the impurities (such as phosphorus, sulfur, etc.) of sludge to the effect of burning clinker. The high content of phosphorus in sewage sludge has a certain potential impact on the subsequent coordination of cement kilns [18]. The different forms of phosphorus could also lead to different influences on cement-burning behavior.
The early-stage work is carried out in the laboratory and the later stage is in a cement rotary kiln. In this work, the reaction process of lime-dried sludge after addition to cement raw meal was investigated. It will provide a theoretical basis for its subsequent application as a sintering agent in cement kilns.
Material and Methods
Sludge Samples
The sludge used in this work was obtained from a municipal wastewater treatment plant located in the southern suburbs of Beijing City (North China). The plant is capable of producing 600,000 m3/d of wastewater. The MSS was collected after being concentrated by a belt filter press, lime was then used to raise the density of sludge particles, and improve the property of sludge dewatering in the plant. LDS was investigated under a 10% mass mixing ratio blending sludge with CaO (AR) in the laboratory, after being dried at 105ºC for 48 h. The LDS was further pulverized in a planetary ball mill (agate mill, QM-3SP2) until the particles were passed through a #200 mesh (with 75 m pore diameter) metallic sieve, and its chemical composition was then characterized.
Cement Raw Materials
The raw meal was collected from a cement plant in Beijing that could produce 9,000 tons of cement clinker per day. All of these raw materials were over-dried at 105ºC for 24 h, and the chemical composition was characterized. The raw materials were further pulverized in a ball mill until the particles could pass through a #200 mesh (with 75 μm pore diameter) metallic sieve, and then blended according to the cement clinker ratio, which was calculated with a consideration of the lime saturation coefficient:
Table 1.
Chemical compositions of cement raw materials and sludges (%).
| Samples | LOIa | SiO2b | Al2O3b | Fe2O3b | CaOb | MgOb | P2O5b |
|---|---|---|---|---|---|---|---|
| Raw meal | 28.78 | 14.03 | 2..68 | 2.48 | 47.60 | 2.72 | 0.00 |
| Dried sludge (DS) | 65.26 | 6.09 | 3.22 | 5.74 | 6.09 | 0.98 | 6.02 |
| LDS | 38.05 | 3.24 | 1.82 | 3.56 | 44.74 | 1.27 | 3.24 |
Table 2.
The P2O5 content in the mixed raw meal with LDS (%).
| Mixed raw meal | 0% | 6% | 9% | 12% | 15% | 18% |
|---|---|---|---|---|---|---|
| P2O5b | 0.00 | 0.24 | 0.34 | 0.44 | 0.53 | 0.63 |
Table 3.
Granulometric parameters of cement raw materials.
| Material | Granulometric parameters (μm) | ||
|---|---|---|---|
| D10 | D50 | D90 | |
| Cement raw materials | 2.08 | 15.8 | 50.3 |
The composition of all the raw meals and sludges are shown in Tables 1 and 2, and the particle size distribution of the cement raw material is presented in Table 3.
Experimental Procedure
The eco-cement raw meals were doped by mixing various amounts of phosphorus as a co-solvent in the form of LDS. The resulting types of cement raw materials contained LDS at 0, 6.0, 12.0, 15.0 and 18.0%, respectively (by weight of raw meal). Raw mixtures were then pressed with a pressure of 35 MPa into blocks of 50 mm × 50 mm × 10 mm and dried in an oven at 105ºC for 2 h. All grounded raw mixtures were burned in a programmable electrically heated furnace to form eco-cement clinkers. The temperature of the high-temperature furnace was raised by 10ºC/min from 50ºC and maintained at 1250~1400ºC for 60 min. After burning, products were cooled rapidly at room temperature. All eco-cement clinkers were pulverized and thoroughly grounded in a ball mill until most of them could pass through a #200 mesh (with 75 μm pore diameter) metallic sieve (retention on the mesh sieve was less than 5% in weight.
Analysis
The SMT extraction method was used to harmonize phosphorus fractionation which includes three independent extraction procedures applied to separate subsamples (~0.2 g). Phosphorus in sewage sludge was then extracted through extraction and centrifugation. The supernatant fluid of phosphorus in the form of active phosphate (SRP) was determined by antimony molybdenum spectrophotometry.
Chemical compositions of sludge and raw meal were detected by using a wavelength dispersion X-ray fluorescence spectrometer (XRF PAN analytical Axios of Netherlands). A particle distribution test was carried out using a laser diffraction particle size analyzer (Mastersizer 3000, England), and its measured range of particle sizes was from 0.01 to 3500 μm.
The content of free lime in clinker was estimated using the glycerin-alcohol method (GB/T 176-2008). Mineral phases of clinker were identified by using a Bruker Corporation D8 Advance diffractometer (Cu Kα radiation). Measurements were carried out at temperatures ranging from 10 to 80° (2θ) with a step size of 0.02° (2θ). The counting time was 4 s at each step, and the accelerating voltage was 40 kV with a current of 100 mA. Observation of mineral morphological features, in particular the alite phase, was carried out on a FEI Company Quanta 200 FEG-SEM with a Link EDX system in a backscatter mode. The accelerating voltage and probe current for the images were 12 kV and 3 nA, respectively. A STA 449 C Jupiter Synchronous thermal analyzer was used to conduct DTA analyses of non-evaporated water content. Hydrated samples were subjected to acetone and isopropyl ether treatment, dried for 24 h in a vacuum and grounded to a fineness less than 80 μm. The grounded samples were placed in an oven at 105ºC and dried to constant weight. Samples were then examined by a thermal analyzer from 30 to 1500ºC at a heating rate of 10ºC/min under flowing nitrogen (100 cm3/min).
Results and Discussion
Change of Phosphorus Forms in the Process of Lime-Stabilized Sludge
To achieve comparable measurements of phosphate forms in the process of lime drying, the Standards, Measurements and Testing Programme (SMT, formerly BCR), the European Commission has launched a project, the first step of which was to evaluate collaboratively existing extraction procedures in sludges [19, 20]. The SMT protocol focuses on five phosphorus fractions: non-apatite inorganic phosphorus (NAIP: the form associated with oxides and hydroxides of Al, Fe, and Mn), apatite phosphorus (AP: the form associated with Ca), inorganic phosphorus (IP), organic phosphorus (OP), and total phosphorus (TP) [20], which exist certain interrelation: TP = OP + IP, IP = NAIP + AP.
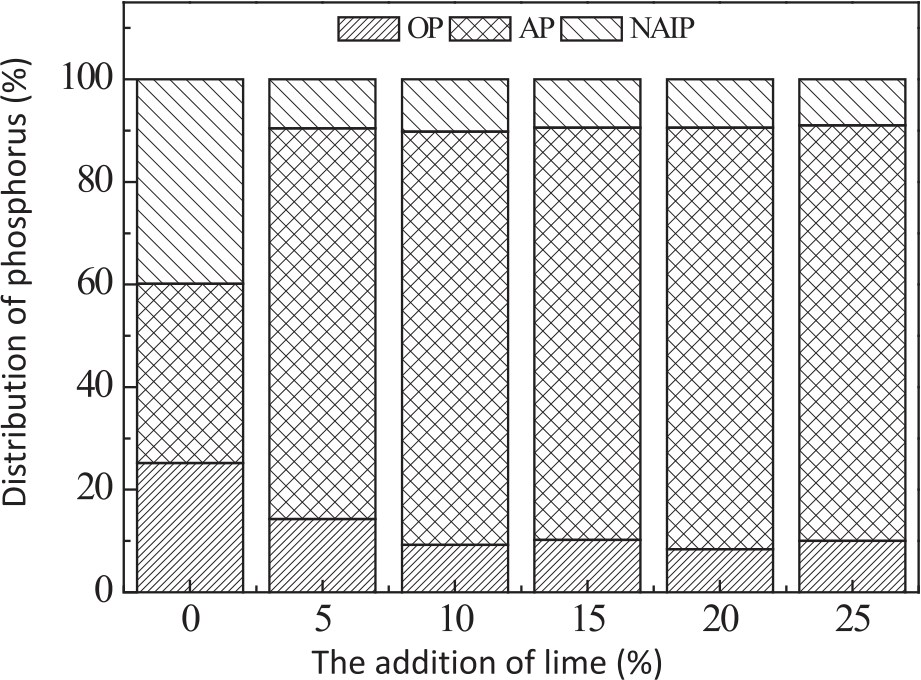
As shown in Fig. 1, IP is the main fraction (74.8% of the TP) in raw sludge. Although raw sludge is considered to be rich in organic compounds, the amount of organic phosphorus was even lower (less than 30% of the TP). This indicated that the portions of organic phosphorus and inorganic fractions were not directly related to the organic matter content of the sludge sample. Furthermore, the ratio of inorganic phosphorus between AP and NAIP inorganic forms was also evaluated. More NAIP was found in sewage sludge (close to 40% of the TP) while AP, NAIP and OP, especially NAIP, are labile phosphorus forms, which could provide an increased risk of phosphorus release to the environment [19]. With the addition of lime, the proportion of OP and NAIP decreased (Fig. 1). This indicated that the labile phosphorus form was changed into a stable phosphorus form. The calcium content in the sludge could be responsible for the decrease by binding phosphorus to calcium phosphate. Nevertheless, 10% of lime was added and the concentration of calcium hydroxide reached saturation in the sludge. pH value and calcium ion concentration did not change, and the phosphorus formed in sewage sludge remained unchanged. The results here demonstrated that lime could stabilize phosphorus in the process of drying sludge. This will significantly reduce the potential environmental risk of phosphorus release during subsequent use of the MSS.
Chemical Composition and Particle Size Distribution of LDS and Cement Raw Materials
Table 1 shows that the main compositions of MSS and some raw materials in cement production were CaO, Al2O3, Fe2O3 and SiO2, while the composition of LDS was closer to the traditional raw material. Therefore, LDS can be used as a raw material substitute in cement production. The lime had a dilution effect on phosphorus in LDS (Table 2). With the increase/addition of LDS, phosphorus content was higher, and it had a high value of utilization. The size distribution of cement raw materials is presented in Table 3. The diameter of particles the size of D10, D50 and D90 were shown to be 2.08, 15.8 and 50.3 μm, respectively. The particle size of the cement raw materials was mainly found in the range of 0.59 to 98.1μm, which attained the production requirements for cement clinker sintering (retained on 80 mesh sieves at less than 10%). Thus, the size distributions of raw materials met the industrial quality criteria for cement production.
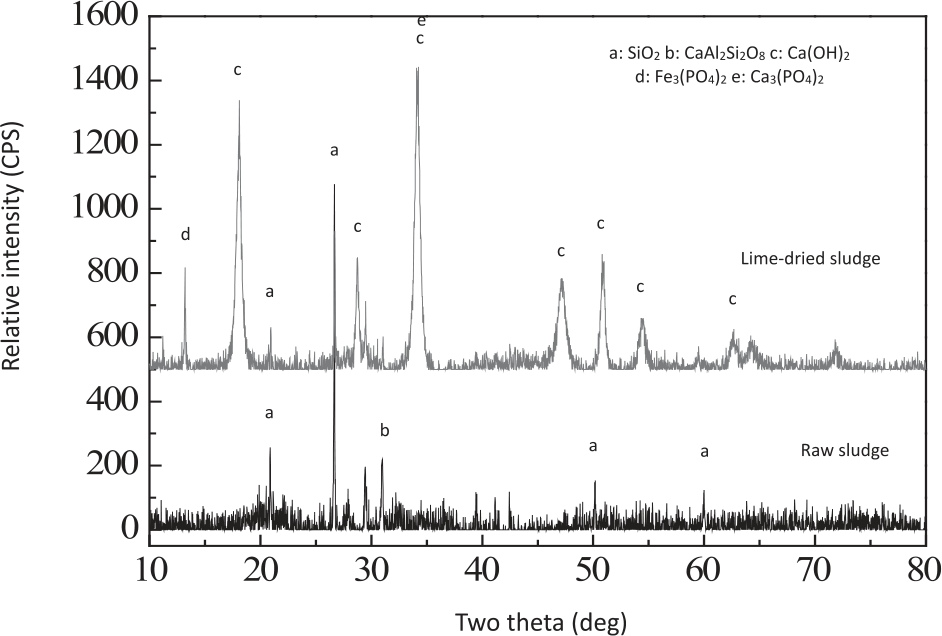
Characterization of crystal phase in sludge samples is shown in Fig.2.
As shown in Fig. 2, the XRD analysis results showed that the raw dewatered sludge contained mainly SiO2, a small amount of CaCO3 and CaAl2Si2O8. This is identical to Rodríguez’s results [13]. However, with the addition of lime (10 wt.%), the diffraction intensity of SiO2 was significantly reduced. Meanwhile, many new diffraction peaks appeared in XRD, which implied that new compounds were formed after lime drying. The strong diffraction peak of LDS was identified as calcium hydroxide, which is associated with the chemical reaction between calcium oxide and water. The calcium and iron in the sludge could bind phosphorus as phosphate in the moist alkaline environment, which was proved by a stronger Ca3(PO4)2 diffraction peak and weaker Fe3(PO4)2 diffraction peak. The results demonstrated that the phosphorus forms of sludge could be turned into a stable form of phosphate by way of lime-improving sludge.
The Volatilization of Phosphorus in the Calcination Process
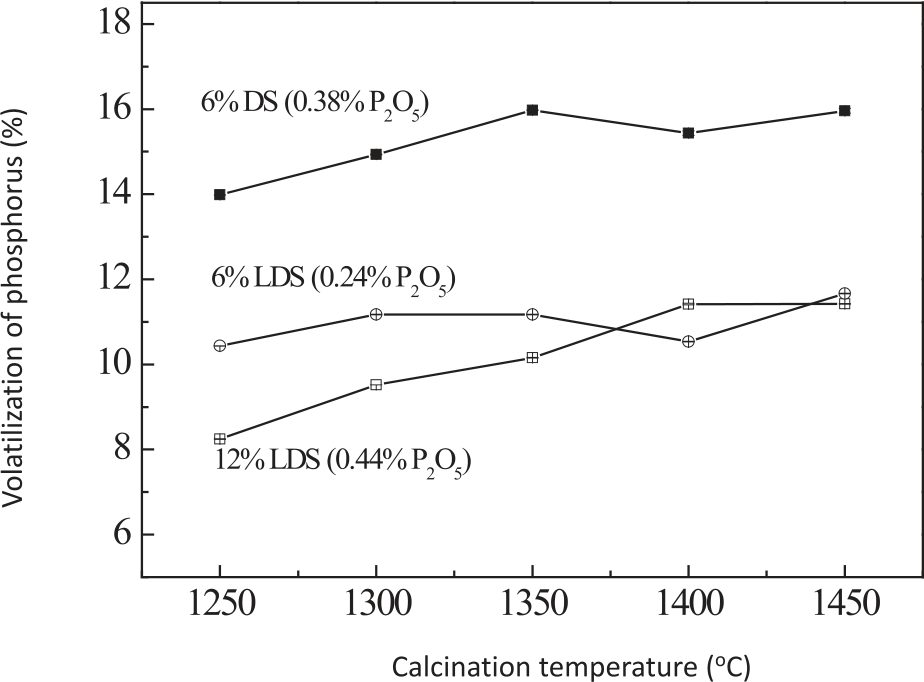
The main crystal phase alite of cement clinker depends on the number and types of ions in the solid solution [21]. Phosphorus is volatile at high temperatures, which inevitably has an effect on the amount of solid solution of phosphorus in alite. Varying volatility of different forms, phosphorus may be the cause of different phosphates on the performance of alite in the cement clinker. The phosphorus releasability of phosphorus-containing cement clinker containing 6% DS, 6% LDS, and 12% LDS, respectively, during the roasting process was investigated.
As shown in Fig. 3, the total amount of phosphorus released increased with the increase in temperature in the process of sintering cement clinker. The phosphorus rate of the clinker mixed with raw sludge was significantly higher than that of the clinker, doped with LDS. Fig. 1 shows that the raw sludge contains large amounts of unstable OP and NAIP, which account for 65% of TP. Therefore, more phosphorus was released at high temperatures. The addition of lime could solve the problem. Overall, the phosphorus-releasing rate of cement clinker doped with LDS was less than 12% in the process of calcining. Compared with the direct co-disposal of 80% aqueous sludge [22, 23], cement kiln co-disposal of lime-dried sludge is able to reduce the secondary pollution emission of phosphorus, and change the form of phosphorus to make good use of it. It also avoids the energy consumption associated with the spray-in method at the end of the kiln, as well as the possibility of clogging the flue chamber at the end of the kiln after a large amount of aqueous sludge is fed into the kiln.
The Effect of Total Phosphorus on the Formation of Clinker
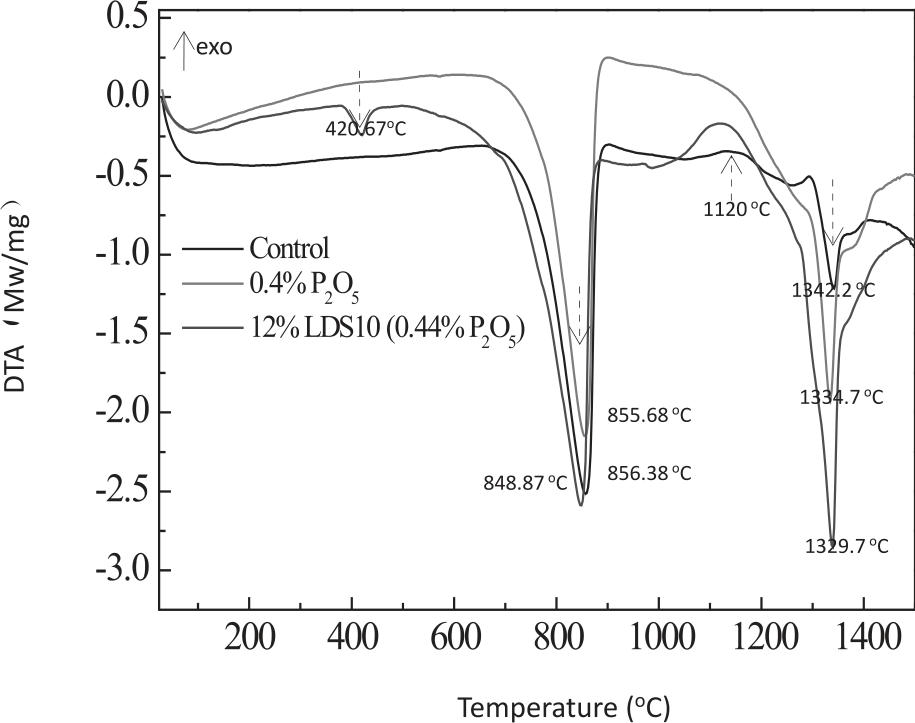
There are three main peaks of energy in all kinds of raw meals, ranging from 200ºC to 1450ºC (Fig. 4). The endothermic peak at around 850ºC was subjected to the decomposition of CaCO3. The thermal decomposition of CaCO3 is an important reaction during cement raw meal decomposition, on which the decomposition rate of raw meal and the output of clinker depends. The two exothermic peaks at around 1120ºC were associated with the production of C3A, C2AS (2CaO·Al2O3·SiO2) and C4AF. Peaks for clinkering reactions were also identified. These peaks were followed by an endothermic reaction: liquid formation at 1330ºC. The liquid phase is essential to the reaction of C3S formation by C2S and free CaO. DTA curves of the mixture containing mineralizer showed similar peaks to that of cement raw material. All clinkering peaks could be identified. A slight variation in the reaction temperatures was observed. Conversely, the raw materials doped with LDS showed a decomposition peak at 420ºC, which was caused by the decomposition of calcium hydroxide. The sintering temperature (1334.7ºC) of the liquid phase of raw cement with 0.4% P2O5 was significantly lower than that of the control (1342.2ºC). The results suggested that the addition of an appropriate amount of P2O5 in raw material was beneficial to reducing the formation temperature of the liquid phase and promoting the formation of C3S, which could reduce the primary energy consumption. Thus, phosphate rock should be a kind of important clinker sintering additive in cement production.
Phosphorus is an essential and limited resource. Looking for a suitable phosphorus substitute was very necessary for the sustainable development of the environment and economics. The effective utilization of phosphorus in lime-dried sludge could save the phosphate rock. Further, the sintering effect of clinker with LDS was superior to the clinker with the addition of phosphorus. LDS could provide an abundant phosphorus source, and the trace elements also play a positive energy in clinker sintering. This form of “double blending” may have a more pronounced effect on cement firing than the direct addition of phosphorus [24]. Under this “double blending” condition, controlling the amount of drying sludge in the right proportion can provide a source of phosphorus, which can save the raw material of cement and promote clinker firing.
Free Lime (f-CaO) in Clinker
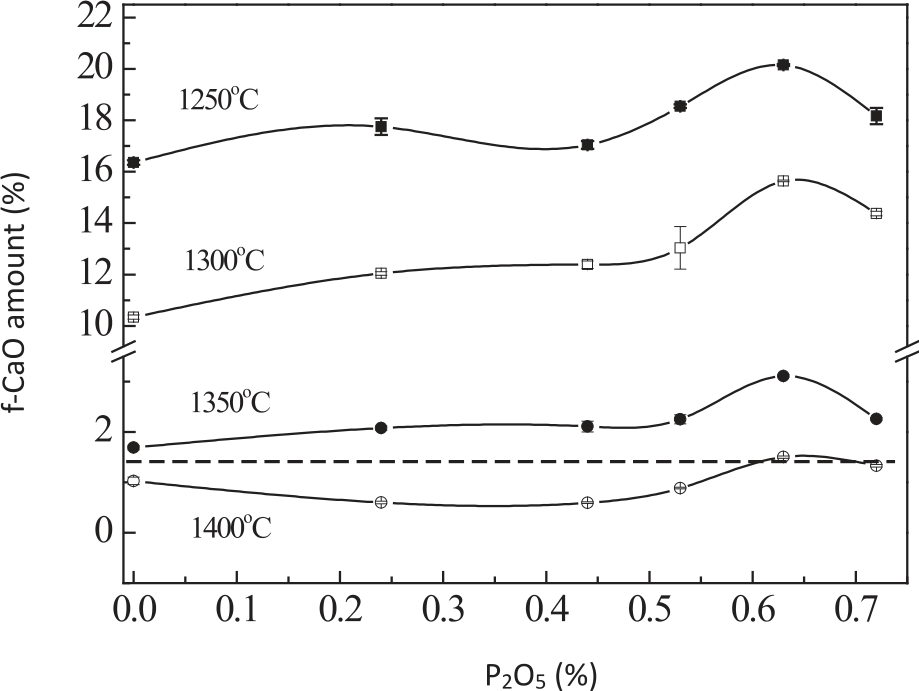
The results of chemical analysis of unreacted lime, so-called free lime (f-CaO) at different temperatures are shown in Fig. 5. Free CaO is undesirable in clinker as it can give rise to expansion during hydration as CaO converts to Ca(OH)2 [13]. The f-CaO content increased with the addition of LDS and decreased with increasing burning temperatures in both series of samples. The increase of f-CaO content in clinker was caused by the addition of P2O5 into C2S. At 1250ºC, 1300 oC, and 1350ºC, the content of f-CaO increased as the amount of P2O5 rose. This trend was obvious in the range of P2O5 amount from 0.44 to 0.63%. When the content reached 0.63%, the f-CaO content began to decrease. From 1300ºC to 1350ºC, free lime content was significantly lower, but the content of free lime was still relatively high. Kolovos [25] found that the effect of phosphorus on the ease of burning of cement was related to its morphology, with CaHPO4 being significantly more effective than Ca3(PO4)2, which is also consistent with our findings. Lime stabilization of sludge improves the utilization of phosphorus in sludge. The phosphorus of LDS mainly existed in the form of stable AP (Fig. 2) with a high melting point in the alkaline environment. It was difficult to generate low melting point material, which was not conducive to the formation of the liquid phase. The impact of phosphorus on the burnability of cement raw mills was regarded to be associated with the different forms of phosphorus. The clinker containing phosphorus at 1400ºC always presented a lower free CaO content than the clinkers at all three firing temperatures studied. Therefore, the coordination of LDS using a cement kiln should increase the reaction temperature for clinker sintering. At 1400ºC, the burnability of raw meals was significantly improved. The effect of P2O5 on the content of f-CaO in clinker is considered to be the decrease in the formation temperature of the liquid phase (Fig.4). This indicated that P2O5 increased the amount of the liquid phase. However, the addition of P2O5 into cement raw meal at this temperature decreased the formation of C3S, while increasing f-CaO in the clinker. Burning clinker at 1400ºC limited the addition of P2O5 to less than 0.63%. Higher contents of P2O5 were challenging because of the high content of free lime. The increasing content of P2O5 causes increasing retardation of alite formation and later, causes total blockage block. It is necessary to consider LDS as an alternative to P2O5. Therefore, the amount of phosphorus to be added should be strictly controlled.
Clinker Mineral
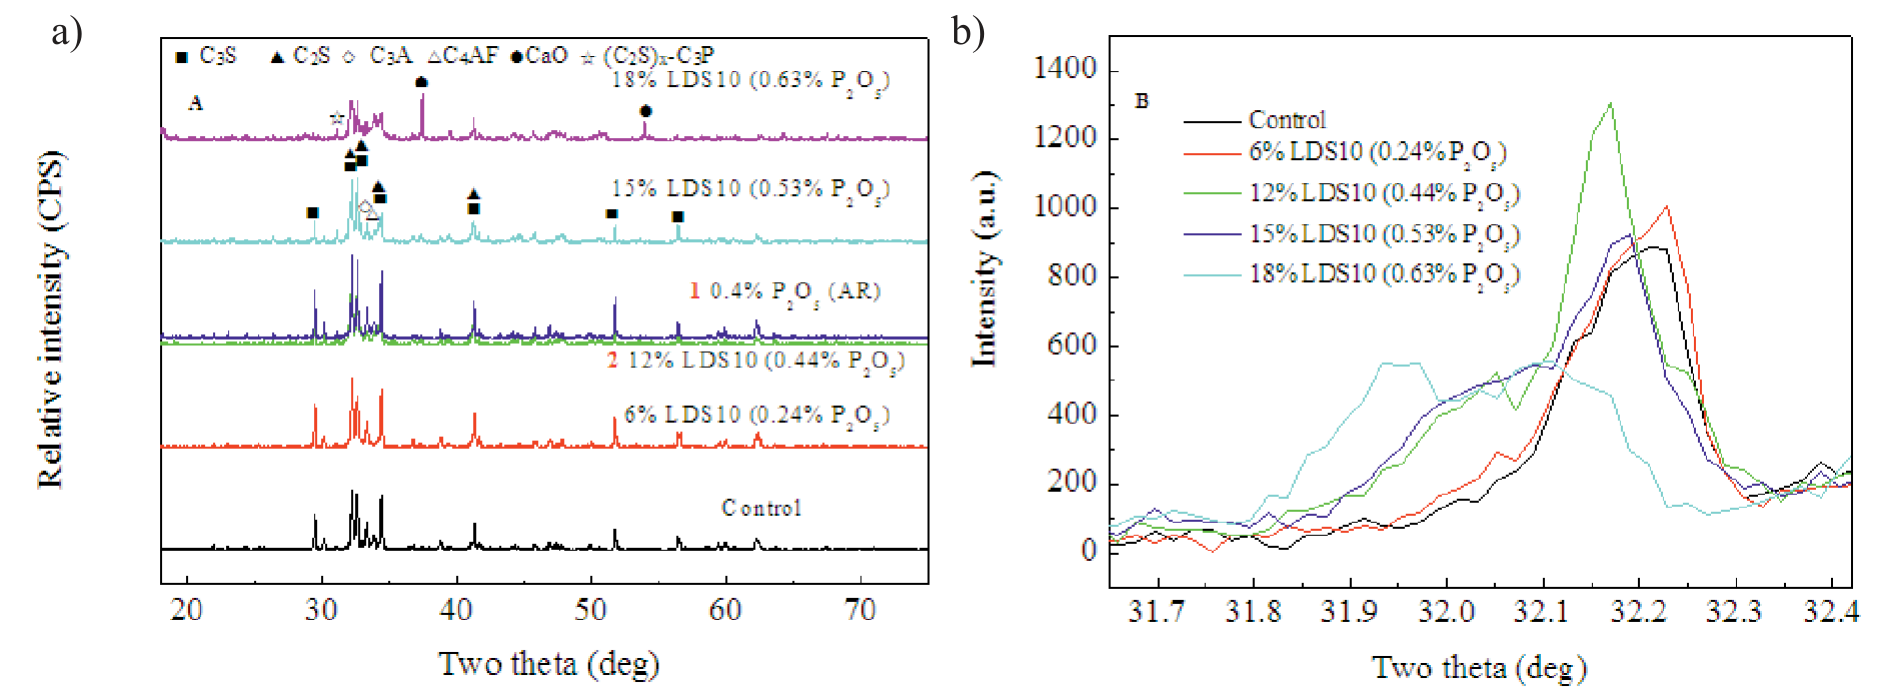
The XRD patterns of clinkers doped with LDS containing phosphorus as alternative materials and sintering agent, respectively, revealed that the incorporation of high contents of phosphorus element led to a modification in the stability of clinkers phases (Fig. 6a). However, these trace elements (except for P, trace Zn, Cu, etc.) could not affect the same phases of clinker.
To compare the crystal phase between the clinker (Red 1 of Fig. 6a) with the addition of phosphorous pentoxide in the form of analytical reagent Ca3(PO4)3 and the clinker (Red 2 of Fig. 6a) with the addition of phosphorous in the form of LDS, main crystal phases (C3S, C2S, C3A, C4AF) of two clinkers were detected. The results showed that the main crystal phases of the two clinkers were the same, while no new crystal phase was formed. This indicated that under the multiple ion compound doped system, trace impurity ions in the sludge did not affect the formation of crystalline phases. Further, the high content phosphorus of in sludge played an important role in the process of clinker sintering. For underdeveloped countries, phosphorus recovery from sludge is expensive, and cement kiln co-disposal would be a safe and environmentally friendly option for most countries where investment is not sufficient to support technologies such as phosphorus recovery [26]. Fig. 6a) showed that a small amount of P2O5 incorporation could lead to the increase of intensity of each phase diffraction peak, especially C3S diffraction peaks with 2ϑ of 29.5°, 34.4°and 41.3°. This indicated that a certain amount of P2O5 was favorable for the formation of the crystal phase of C3S and the improvement of C3S content. Besides, a new diffraction peak at about 31.06ºC, appeared in the clinkers mixed with LDS. With the addition of only 0.24% P2O5, phosphorus was detected in the α-C2S-C3P phase, which suggested that this phase was enriched in phosphorus from the beginning. However, when the phosphorus content was higher by the introduction of LDS, C3S diffraction peaks weakened at 2θ = 29.5°, 34.4° and C2S diffraction peak with 2θ = 32.5° increase, which initiated the partial decomposition of C3S. As phosphorus content increased, C3S was decomposed into free lime and α-C2S(P), forming a series of C3S-3CaO·P2O5 solid solutions. Here, the threshold limit was defined as the maximum amount of trace elements that could be incorporated into a standard clinker whilst reaching the limit of solution of its major phases. The main C3S characteristic peak of the qualified clinker occurs around 32ºC. The relative content of C3S in clinker with the increasing of phosphorus was shown in Fig. 6b). The major effect of phosphorus addition is to decrease the alite/belite ratio, with a strong deterioration of the mechanical properties of the hydrated cement, since alite is the main hydraulic phase in the clinker [27]. The results showed that the content of C3S in the clinker samples with less than 15% LDS (0.53% P) was significantly higher than the reference clinker. The complex mineralization of calcium hydrogen phosphate in LDS is the most effective, and the complex effect of impurity ions can mitigate the effect of high phosphorus content during clinker formation. When the amount of LDS was 18% and the P content was 0.63%, the C3S content in clinker was significantly reduced, which had a greater effect on the strength of cement clinker. The use of phosphate-coating sludge as a substitute in cement production was investigated [28] and significant changes in the clinker formation process were observed when sludge addition was up to 7%. The results showed that P2O5 distinctly blocked the formation of alite and stabilized belite. The trend was detected already in clinkers containing 0.63 % P2O5.
Alite Polymorph
C3S is the most important phase in Portland cement. It exhibited seven polymorphisms: three triclinic TI, TII and TIII, three monoclinic MI, MII, MIII and a rhombohedral R. At room temperature, pure C3S provides only polycrystals of TI. The other six modifications were stable only at higher temperatures (more than 1450ºC) or as solid solutions with stabilizing foreign oxides. However, some trace components, could dissolve in C3S, decrease the formation temperature of C3S, and reduce the viscosity and formation temperature of the liquid phase, which was conducive for the generation of a high-temperature phase. When many impurities with high concentrations existed in the raw meal, MI and MIII were the most frequently observed polymorphs in commercial clinker.
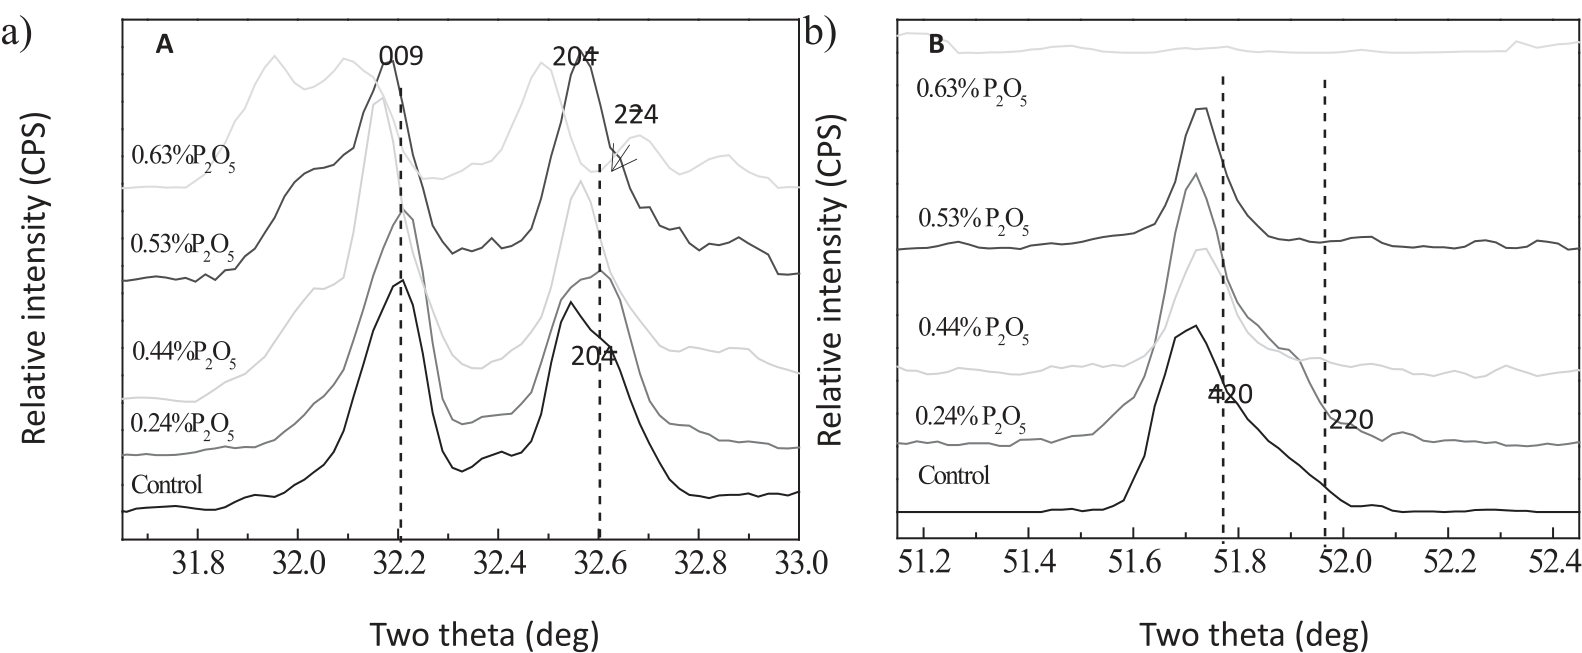
After the introduction of phosphorus, diffraction peaks with 2θ = 32-33° and 51-52° of the clinker after calcination at 1400ºC were shown in Fig. 7. Peaks appearing from 32° to 33° and from 51° to 52° are good indicators of the symmetries for the C3S polymorphs. As mentioned by Urabe K the crystalline form of reference clinker was R-form [29]. When the introduction amount of phosphorus was less than 0.44% (Fig. 7b), a splitting peak appeared at 2θ = 51-52°, which indicated that the crystal phase in cement clinker appeared crystalline MI-form. However, with the increase of phosphorus content, MI-form phase gradually disappeared again. When the phosphorus content increased to 0.53%, the crystal phase in cement clinker became crystalline R-form again.
The effect of phosphorus on C3S crystal form was related to the types of phosphorus compounds. After lime drying, the phosphorus of LDS mainly existed in the AP form. The melting point of calcium phosphate was 1670ºC, which was not easy to generate the solid solution. When the solid solubility of P2O5 in clinker was smaller, AP in solid solution did not change to the C3S crystal phase. After the solid solubility of P2O5 increased, the clinker crystal phase changes were more obvious. At the same time, it could be seen that the peak at 2θ≈51.7° drifted to the right, which was mainly because of the replacement of P5+ by Si4+. This is a non-equivalent replacement, the ion radius of Si4+ in tetrahedral coordination is 0.26 Å and that of P5+ is 0.17Å. The incorporation of phosphorus facilitates a high level of substitution of Si4+ for P5+ in belite phases, which causes a contraction in the crystal cell.
Microstructure and Chemical Analysis of Co-Cement Clinkers by SEM/EDS
SEM examinations were performed to verify the XRD pattern results for the plain clinker and three eco-cement clinkers. Fig. 8 showed the microstructure of clinkers with different content of P by introducing LDS. A discrepancy in the microstructure of the clinkers was found with different amounts of sewage sludge added to the raw meal.
Fig. 8.
SEM micrographs of the eco-cement clinkers with the addition of different percentages of P: a) 0%, b) 0.44%, c) 0.53% and d) 0.63%
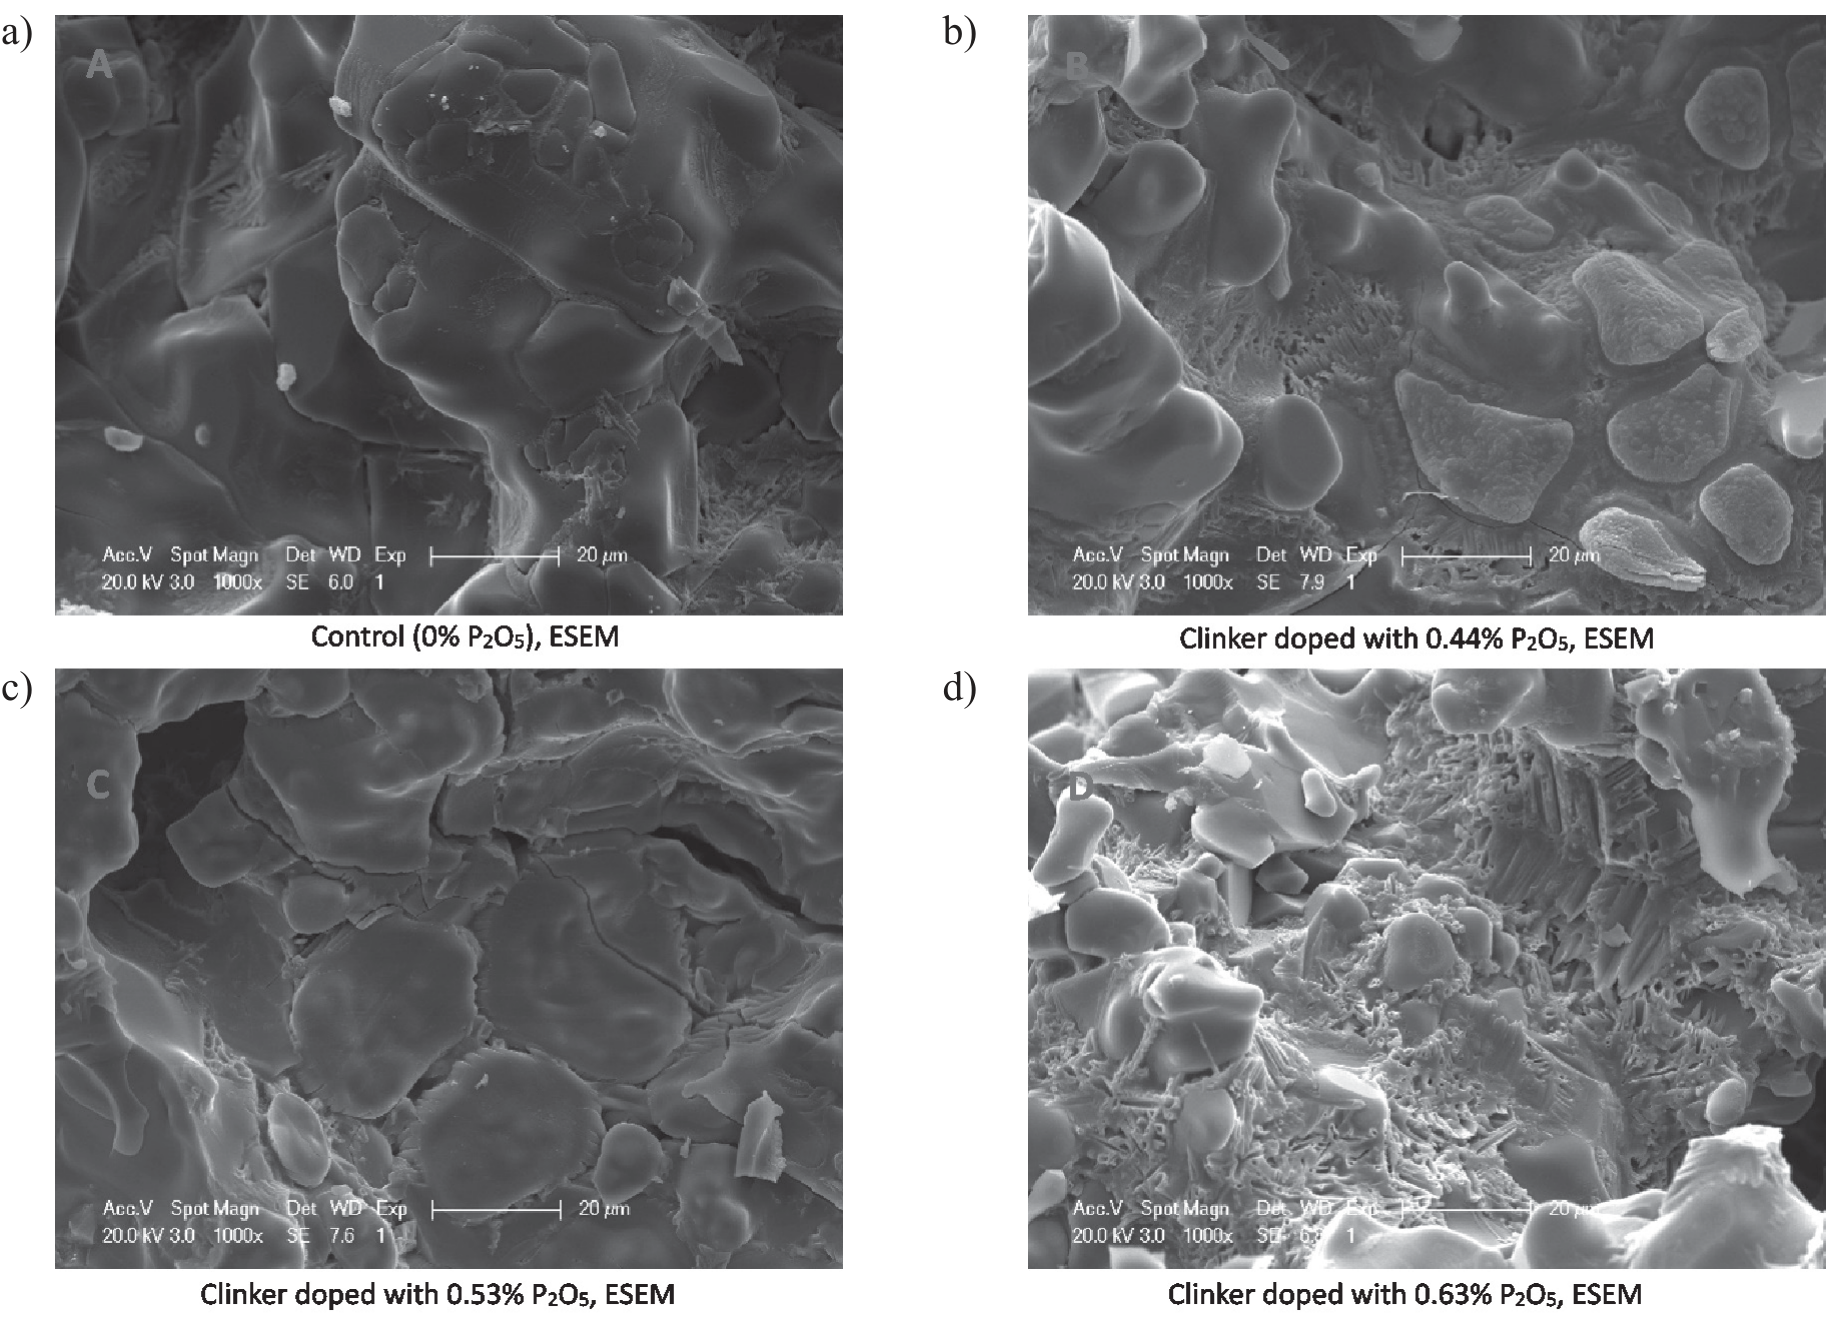
A phase with a very smooth appearance (no porosity, no polishing lines and no cracking) covered more and more of the C3S grain clusters in the reference clinker (Fig. 8a). It appeared that their outlines and boundaries were very clear. Compared with the reference, the mineral structure of cement clinker doped with P had no obvious change (Fig. 8(b, c)). However, the silicate mineral crystals of P-doped clinker became slightly smaller and the mixed melt increased significantly. The Blend melted inlaid in the phases and made the outline of the crystal phase fuzzy. This is mainly a contribution of phosphorus to clinker liquid formation. Liquid content had a great effect on the sintering. The more liquid contained, the faster the sintering rate obtained. Low content of phosphorus could promote the clinker mineral development, and improve the high-temperature liquid viscosity. This was advantageous to the proliferation and migration of the particles in the liquid phase sintering process. Thus, it promoted the formation of C3S and reduced the activation energy of the clinker formation process. However, when phosphorus was introduced at 0.63%, it stabilized belite, reduced the viscosity of the melt phase, delayed the crystallization of alite, affected its crystal size, and significantly increased the liquid content. At this point, a phase with porosity, polishing lines, and cracking appeared and the C3S structure disappeared. Larger liquid content was easy to produce higher content of C2S-C3P solid solution, which was bad for clinkers sintering. Therefore, when cement kilns are utilized for co-processing sludge with high phosphorus content, threshold limits for phosphorus need to be strictly controlled.
Table 4 showed that Fe, Al and Mg were detected in all crystal phases and P. This indicated that most of the calcium silicate phases were not pure. Alite, belite and intermediate phase (C4AF) were detected in Fig. 9. Phosphorus was found among them but mainly in the C4AF phase and belite phases. Lime could stabilize phosphorus and change its form in the drying process. P contents in belite phases were observed to be more than double those in alite phases. It was reported that if P2O5 in the clinker was ≥0.5%, the solubility of P2O5 in belite could be twice as high as in alite. Other effects that were noted in the belite phases were reductions in Si level and an increase in Al level, relative to the alite phase of the clinker. This indicated that the presence of P in the raw materials has favored substitutions of Si4+ for P5+ in the silicate phases. According to the different valencies of the ions, the substitutions tend to react in the following ways [13]:
Fig. 9.
EDS spectrum diagram of clinker adding 12 wt.% LDS containing 0.44% P. EDS analyses made in several parts of the sample (points A, B and C) show calcium, silicon, oxygen, phosphorus, iron, magnesium and aluminum.
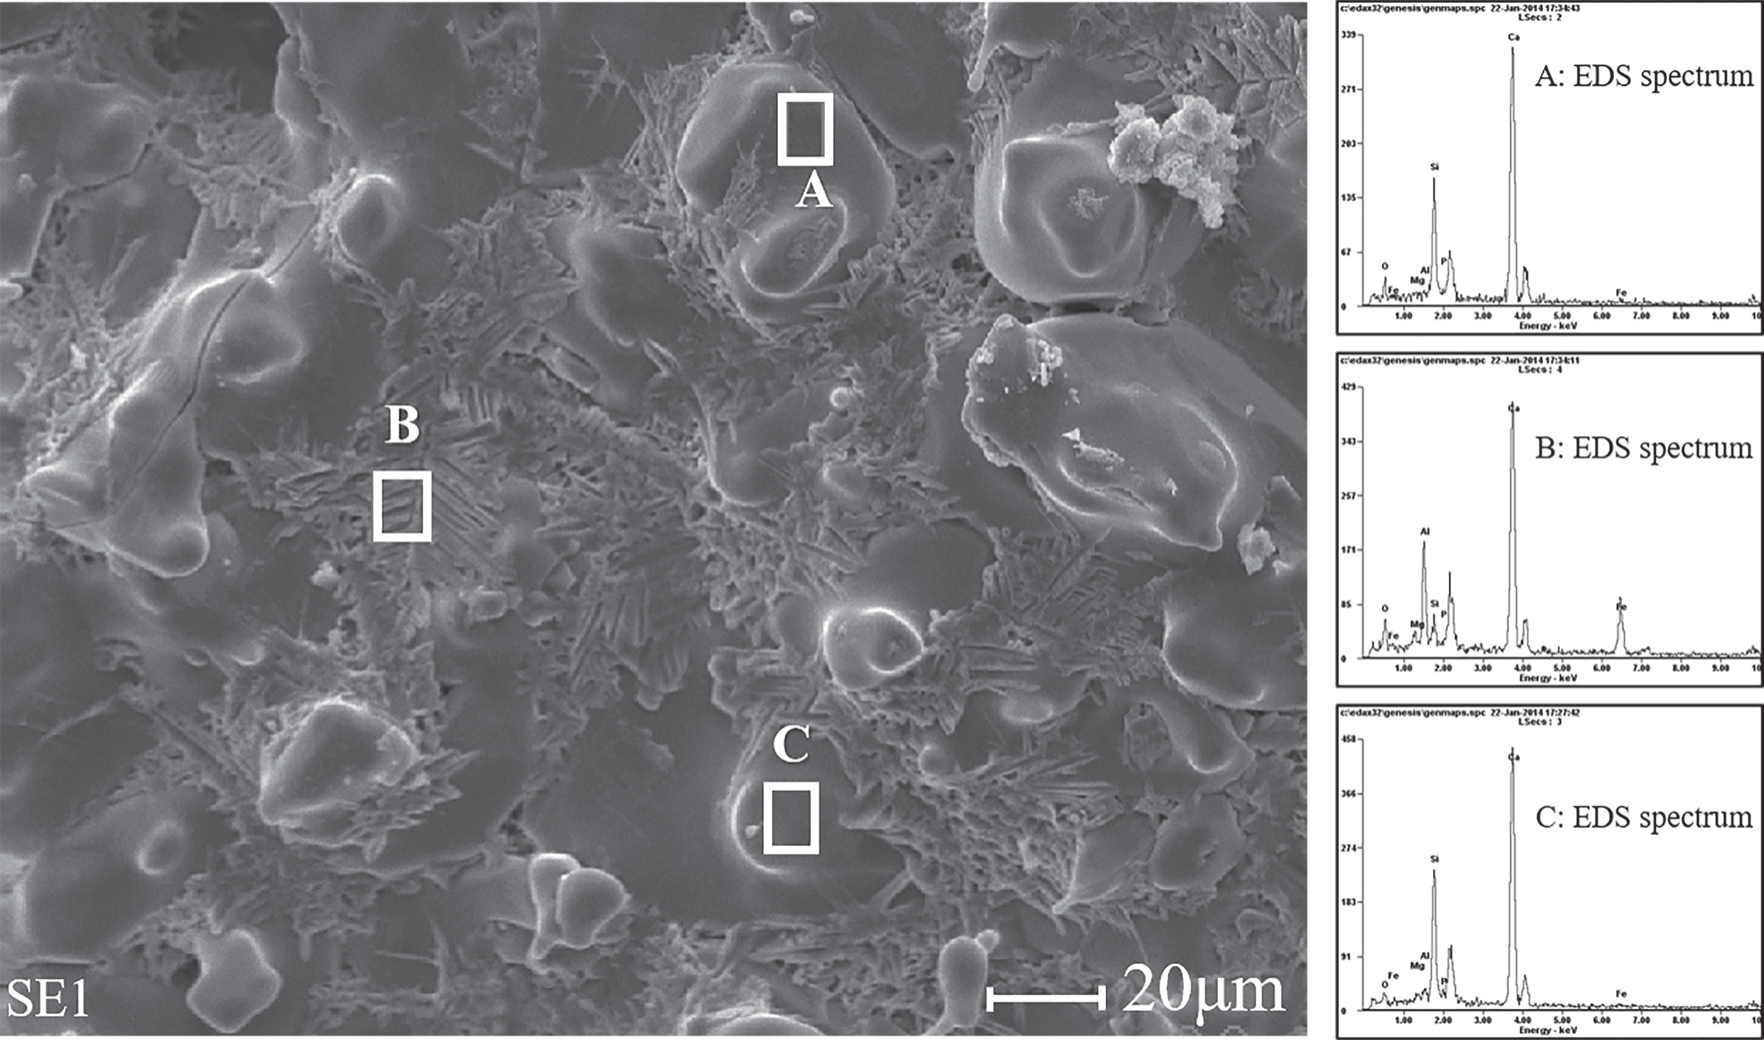
Table 4.
EDS chemical analysis of points A, B and C on the surface of clinker doped with LDS (at%).
| Element | O | Ca | Si | Al | Fe | Mg | P |
|---|---|---|---|---|---|---|---|
| Alite (A) | 36.86 | 41.91 | 15.47 | 1.38 | 1.15 | 1.54 | 1.69 |
| C4AF (B) | 34.96 | 28.85 | 4.33 | 15.30 | 10.53 | 3.93 | 2.10 |
| Belite (C) | 47.95 | 30.17 | 13.45 | 3.08 | 0.89 | 3.32 | 1.94 |
where: R+ is monovalent metal ions, such as Na+ or K+. M3+ is trivalent metal ions, such as Al3+ or Fe3+.
This also explained that phosphorus was detected in the α-C2S-C3P phase from the beginning when LDS was added (Fig. 6).
Conclusions
In conclusion, our results demonstrate that it is feasible that lime-mediated sewage sludge can partly replace phosphorus fluxes as cement sintering and LDS can function as a source of phosphorus. In the process of lime-drying sewage sludge, the sludge is stabilized and reduced, and most of the high phosphorus content is turned into a stabilized form. In the coordination of lime-dried sludge using a cement kiln, over 85% of phosphorus was solidified in the clinker to reduce the environmental pollution of phosphorus. The results show that lime-dried sludge can be directly added to the cement kiln raw meal preparation system when the addition of lime-dried sludge is less than 15% and the introduced phosphorus content is less than 0.53%. This method reduces the environmental load, improves combustibility and accelerates clinker formation. Small amounts of phosphorus promote the production of the M1-form of C3S at lower temperatures. In the beginning stage, the introduction of phosphorus led to the decomposition of C3S to α-C2S and calcium oxide. Phosphorus enters calcium silicates (C2S, C3S), preferentially C2S, and its content is higher in the case of C2S than in C3S in analyzed samples. Moreover, the formation of alite is not blocked neither the maximum selected addition of P2O5. Conclusively, lime-mediated sewage sludge as phosphorus fluxes is a potential way of utilizing cement clinker production. Co-disposal of sludge in cement kilns will effectively reduce carbon emissions and promote the green transformation of the cement industry. The cement kiln co-disposal method of lime-dried sludge we studied can reduce the secondary pollution emission of phosphorus and change the form of phosphorus to make full use of it compared with direct sludge disposal. In addition, our research has been proven to have good popularization value and practicality. The process has been applied in cement plants in Beijing, Zunyi and Guangzhou.

